 This item is sold
 This item is sold
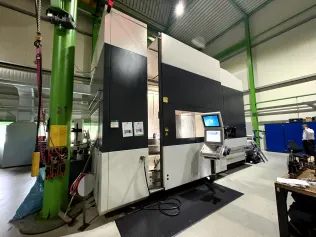 This item is sold
 This item is sold
 This item is sold
1. Used 5-Axis Machining Centres
A 5-axis machining centre has the three linear axes X, Y and Z plus two rotary axes, so the tool can reach the workpiece from almost any direction. Several faces are machined in one set-up, which reduces the number of set-ups and keeps the positional accuracy between those faces. Typical parts:
Moulds and cores with free-form surfaces
Aerospace components and turbine blades
Prismatic parts machined on several faces in one set-up
Complex one-off parts and small series
ReMach lists second hand 5-axis machining centres, with travels, control, tool magazine and photos on every machine page.
>>> Browse the machines below or send an enquiry for the configuration you need.
2. 3+2 Positional and Simultaneous 5-Axis Machining
Both run on a 5-axis machine, but they work differently. Knowing which one your parts need avoids paying for capability you will not use, or buying a machine that cannot do the job.
3+2 Positional Machining
The two rotary axes tilt the part or the head to the required angle and are then clamped
The three linear axes do the cutting
Enough for most prismatic parts that need machining on several faces
Lower CAM requirements and simpler programming
Simultaneous 5-Axis Machining
All five axes move at the same time along the whole tool path
Needed for free-form surfaces, turbine blades and continuous curved tool paths
Requires 5-axis CAM and a post-processor matched to that exact machine and control
In listings this is usually stated as "5-axis simultaneous machining"
A machine that supports simultaneous 5-axis machining can also run 3+2, but not every 3+2 machine can run simultaneously. When reading a listing, look for the word "simultaneous" and for the control model.
3. Rotary Axis Design: Swivel Head, Trunnion Table or Gantry
Where the two rotary axes sit determines the maximum part size and weight. This is the biggest difference between 5-axis machines.
Swivel Head with Rotary Table (B-axis in the head, C-axis in the table)
The B-axis sits in the milling head, the C-axis is an NC rotary table
Heavy parts stay flat on the table, only the head tilts
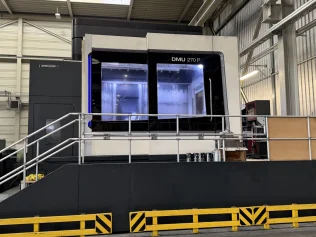
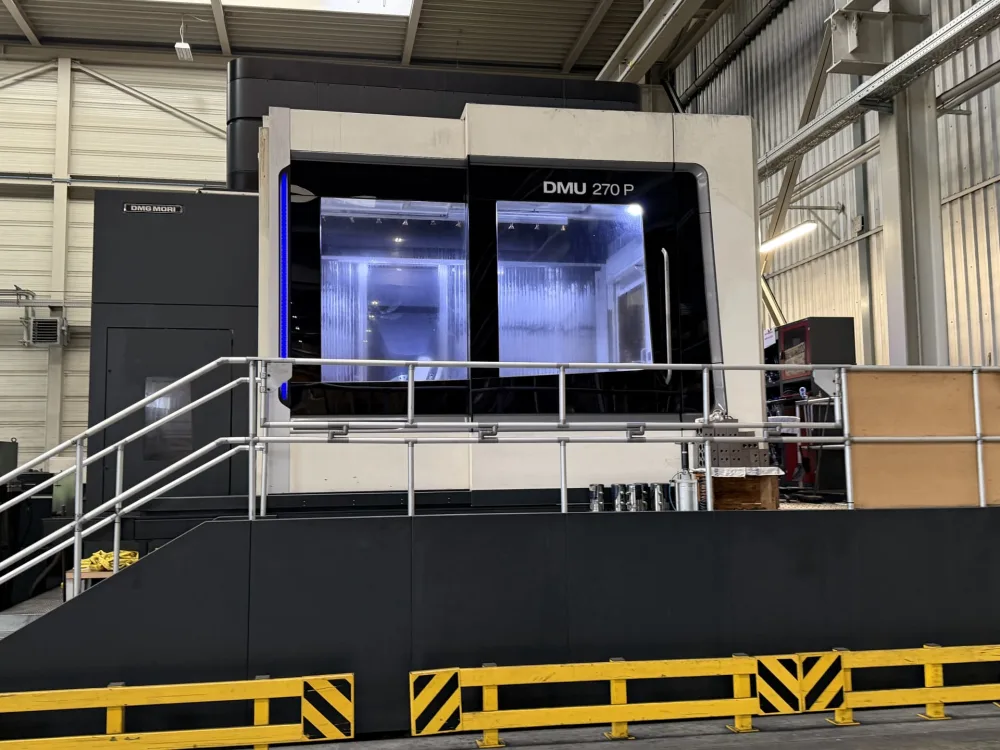
Suited to large, heavy parts; this is the design of the DMG MORI DMU P series
Trunnion Table
Both rotary axes are in the table, so the part tilts with it
Compact and accurate for small and medium parts
Part size and weight are limited by the table
Gantry (Portal) Design
The spindle moves on a gantry above a fixed table
Suited to very long or wide parts such as plates and large moulds
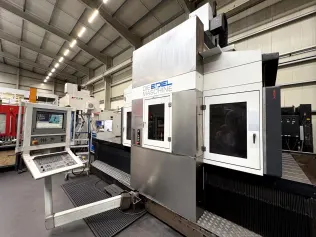
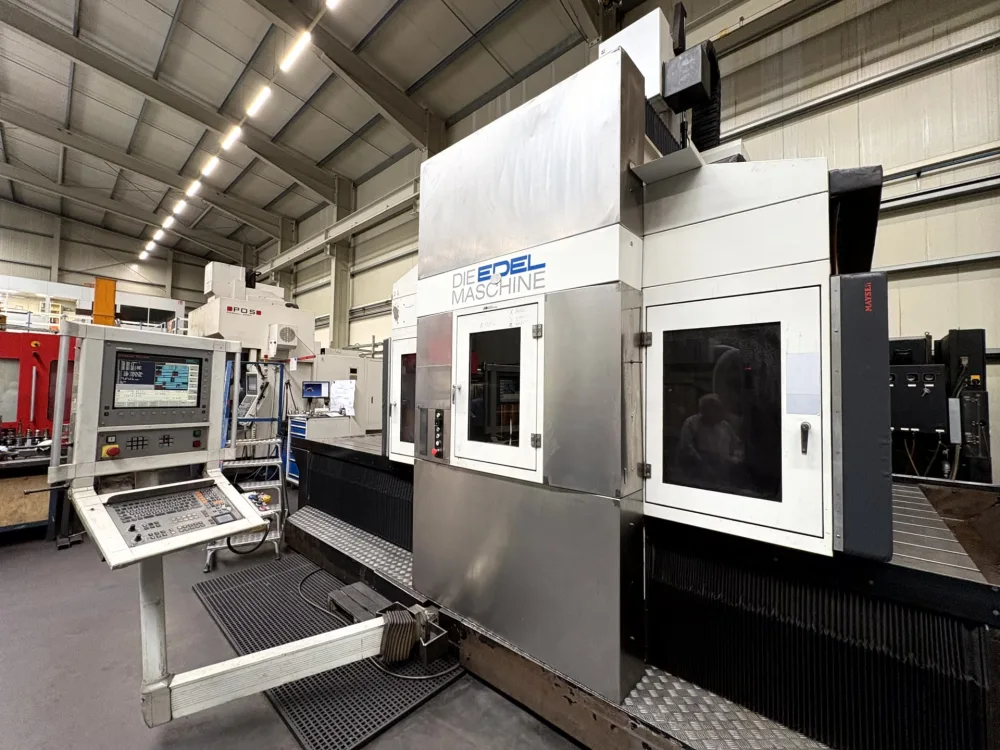
Example: EDEL CP3020, table 5,000 x 2,300 mm, A-axis ±110°, C-axis ±360°
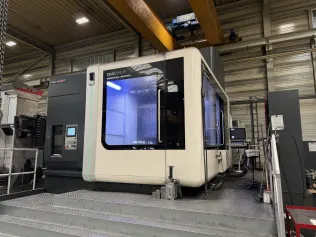
5-axis machining centres documented in the ReMach catalogue include the DMG MORI DMU P series, Reiden and EDEL. X-axis travels range from 980 mm to 3,000 mm and machine weights from approx. 16 t to 85 t.
4. What to Check on a Used 5-Axis Machining Centre
Besides travels and spindle power, which matter on any milling machine, a 5-axis machine has a few points of its own.
Working Envelope
Travels and table size: X, Y and Z travel together with the table dimensions
Rotary table: diameter and maximum table load
Swivel range: for example A-axis ±110°, B- or C-axis ±360°; it decides which tool angles you can reach
Rotary Axes and Accuracy
NC control of both rotary axes: fully NC controlled, or only manually indexed
In-machine measurement: tool and workpiece probing, for example a touch probe or laser system
Kinematic calibration: after relocation, the rotary axis kinematics must be recalibrated before precision parts are run
Control and Operation
Control and version: for example Heidenhain iTNC 530 with 3D path control
Tool magazine and taper: number of tool positions and taper, for example SK50 to DIN 69871, or HSK
CAM post-processor: it must match the machine and control, otherwise simultaneous 5-axis machining cannot be used
Spindle hours: where the listing states them
5. Installation, Transport and FAQ
5-axis machining centres weigh roughly 16 t to 85 t depending on size. Plan the following before buying:
Foundation and hall: large machines need a foundation to the manufacturer's drawing; check the machine dimensions in the listing against floor space, hall height and crane capacity
Dismantling and transport: in most cases the buyer is responsible for organizing the transport; upon request, ReMach can check whether transport can be arranged or supported
Paperwork: ReMach helps with dismantling and loading, export and customs checks, and export documents
See all machining centres in our CNC Machining Centres category, or other machine types under Milling Machines.
Do I need simultaneous 5-axis machining, or is 3+2 enough?
If your parts are mainly flat faces and holes on several sides, 3+2 is enough and programming is simpler. Simultaneous 5-axis machining is needed for free-form surfaces such as moulds and turbine blades, where the tool must tilt continuously along the path.
Which design should I choose: swivel head, trunnion table or gantry?
A swivel head with a rotary table suits large, heavy parts because the part does not tilt. A trunnion table is compact and accurate for small and medium parts. A gantry machine suits very long or wide parts.
Does a used 5-axis machine need recalibration after relocation?
Yes. After dismantling, transport and reinstallation, the rotary axis kinematics should be recalibrated and checked with a test part before precision work starts.
Can I keep my existing CAM programs?
Not automatically. 5-axis programming needs a CAM post-processor matched to the machine design and the control, so confirm the control and its version before buying.
How heavy is a used 5-axis machining centre and how is it transported?
In the ReMach catalogue, 5-axis machines weigh from approx. 16 t to 85 t. The machine is dismantled into assemblies and moved by heavy haulage. In most cases the buyer is responsible for organizing the transport; upon request, ReMach can check whether transport can be arranged or supported.
>>> Send an enquiry about a 5-axis machining centre