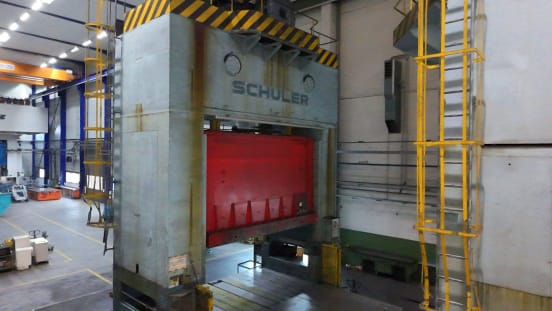
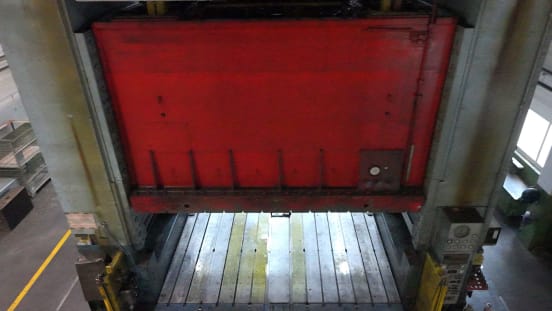
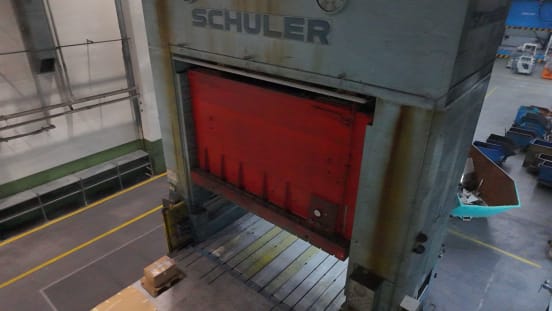
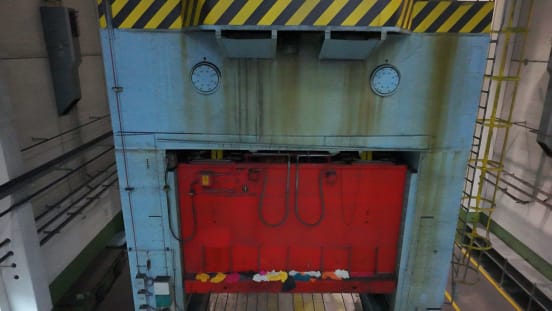
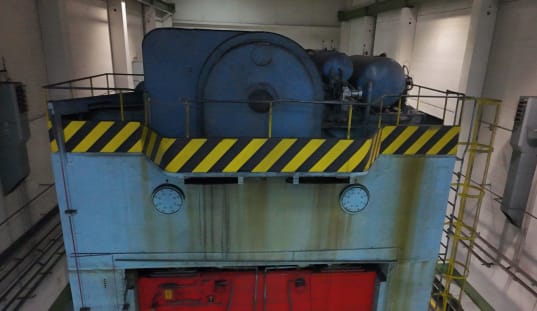
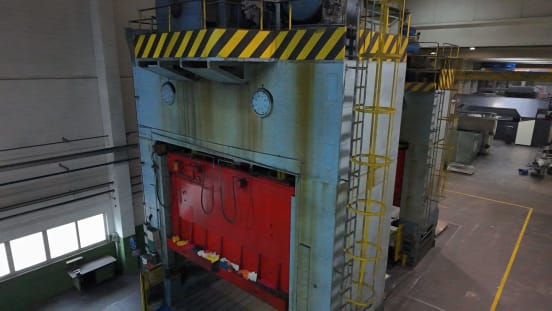
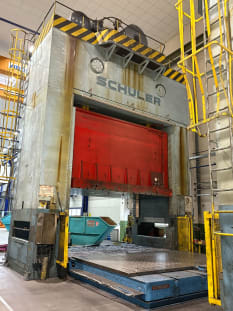
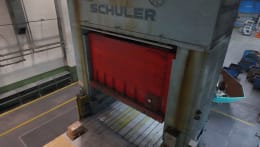
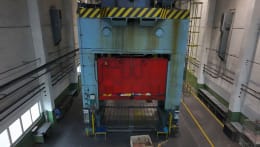
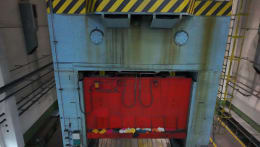
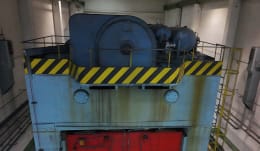
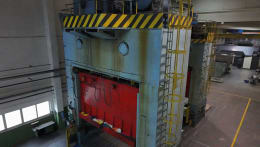
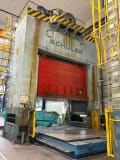
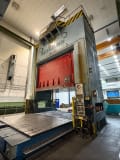
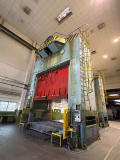
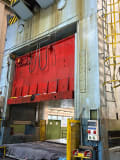
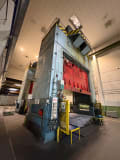
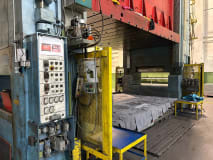
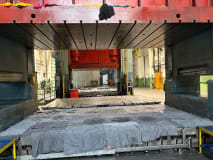
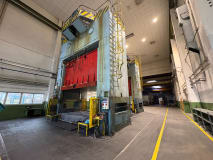
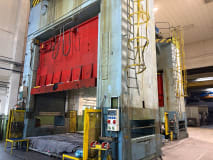
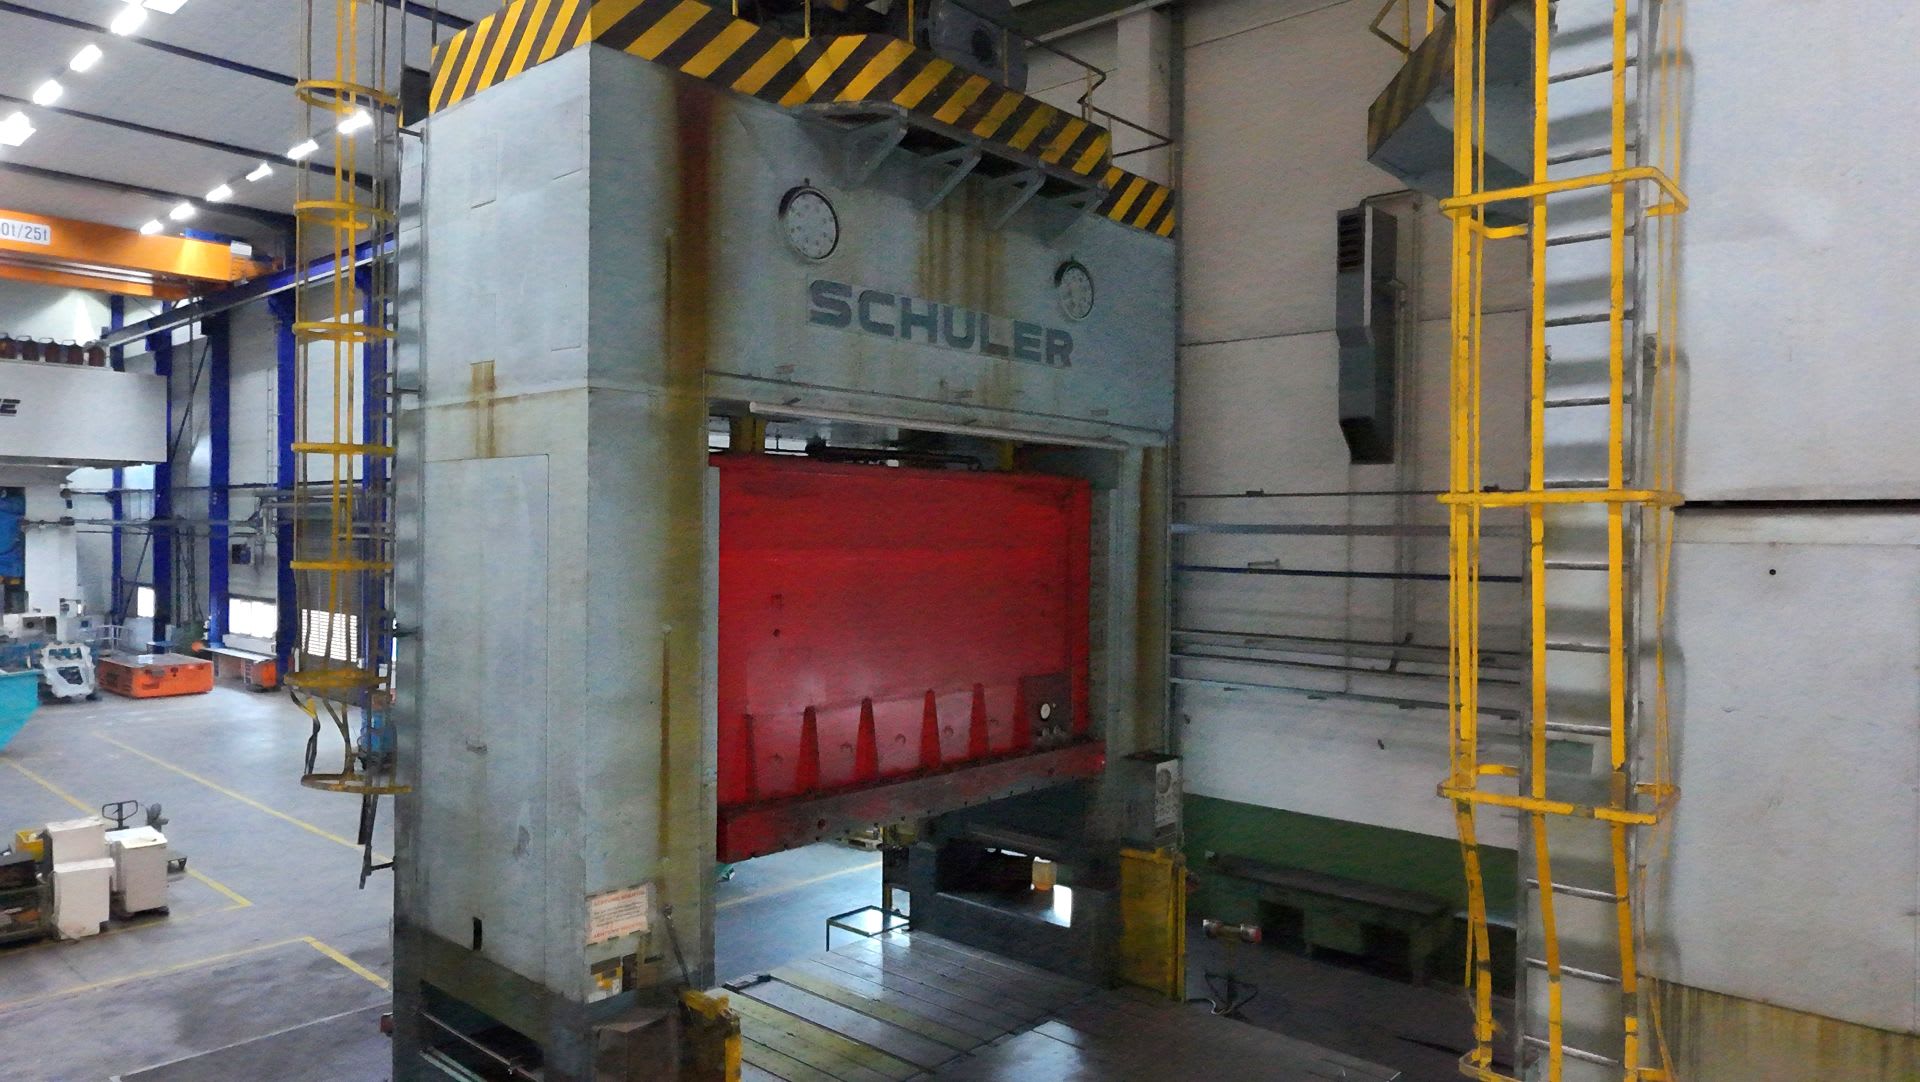
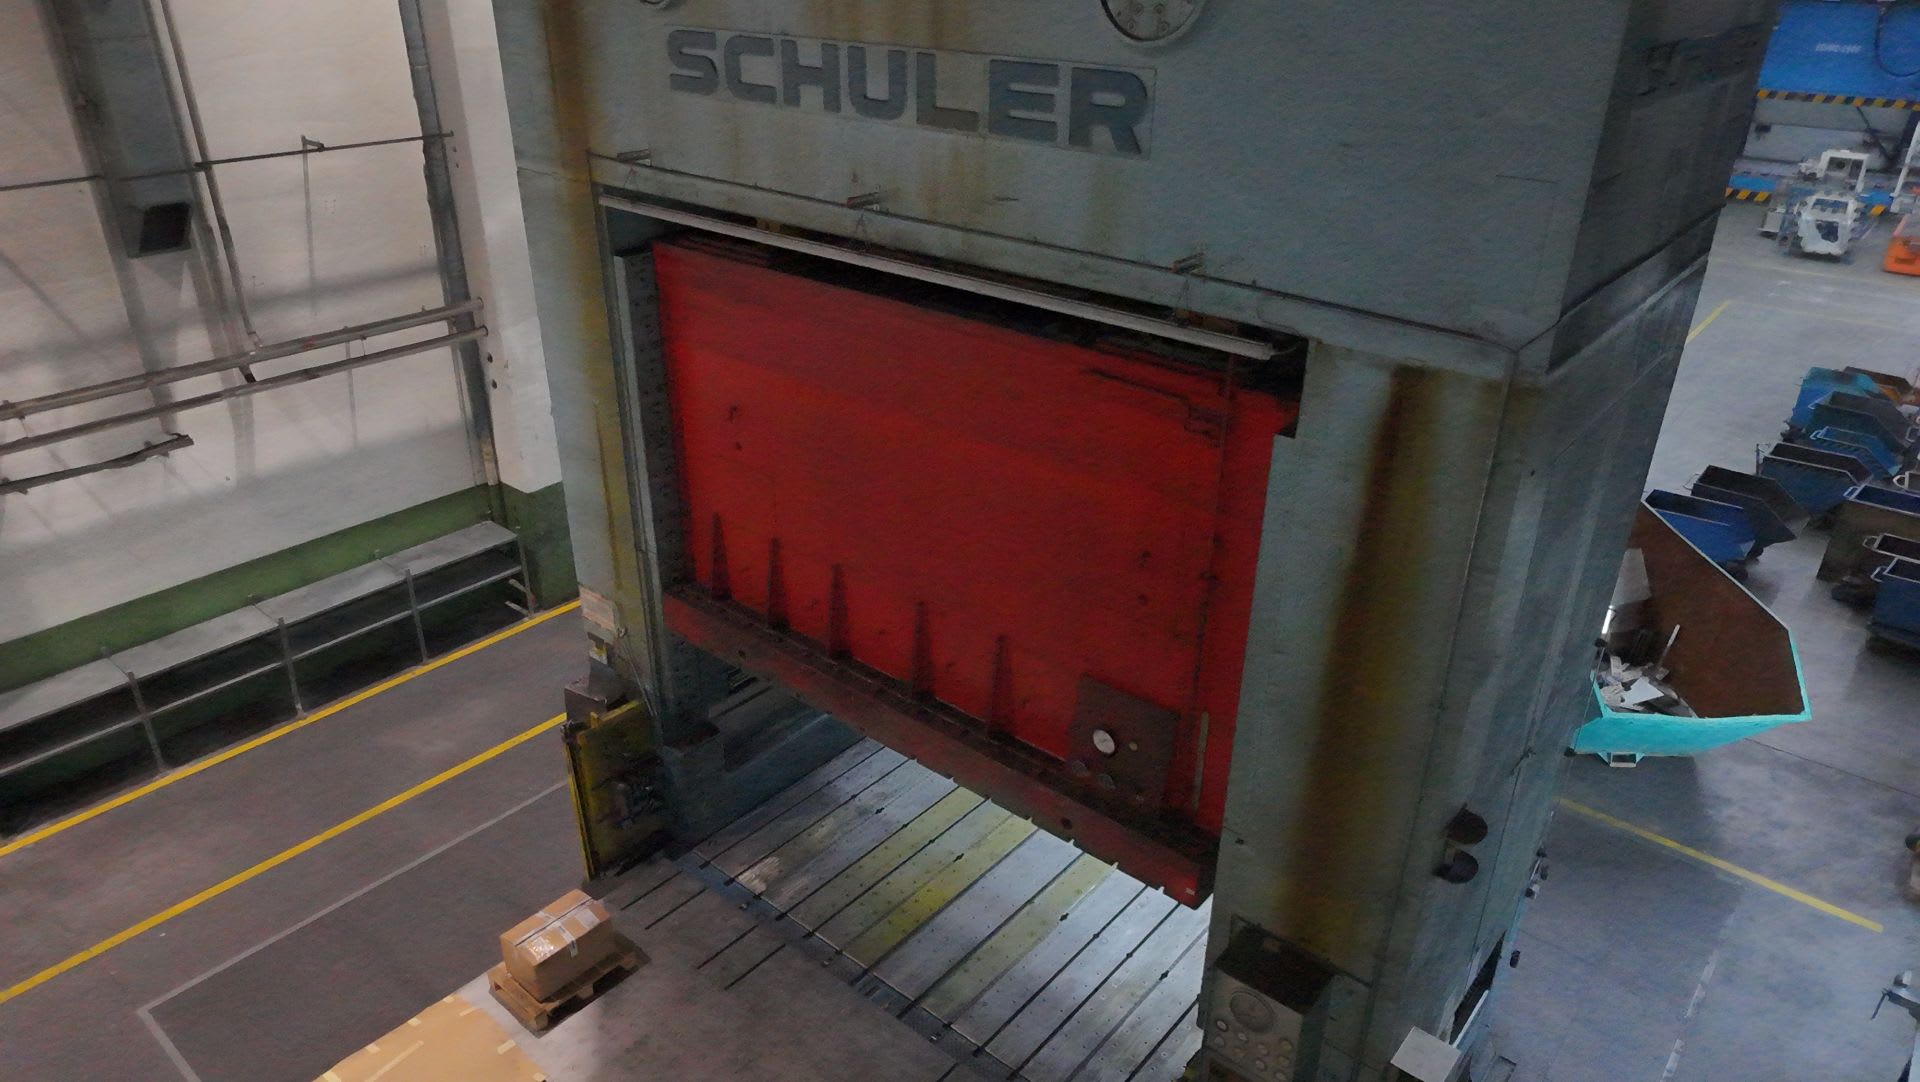
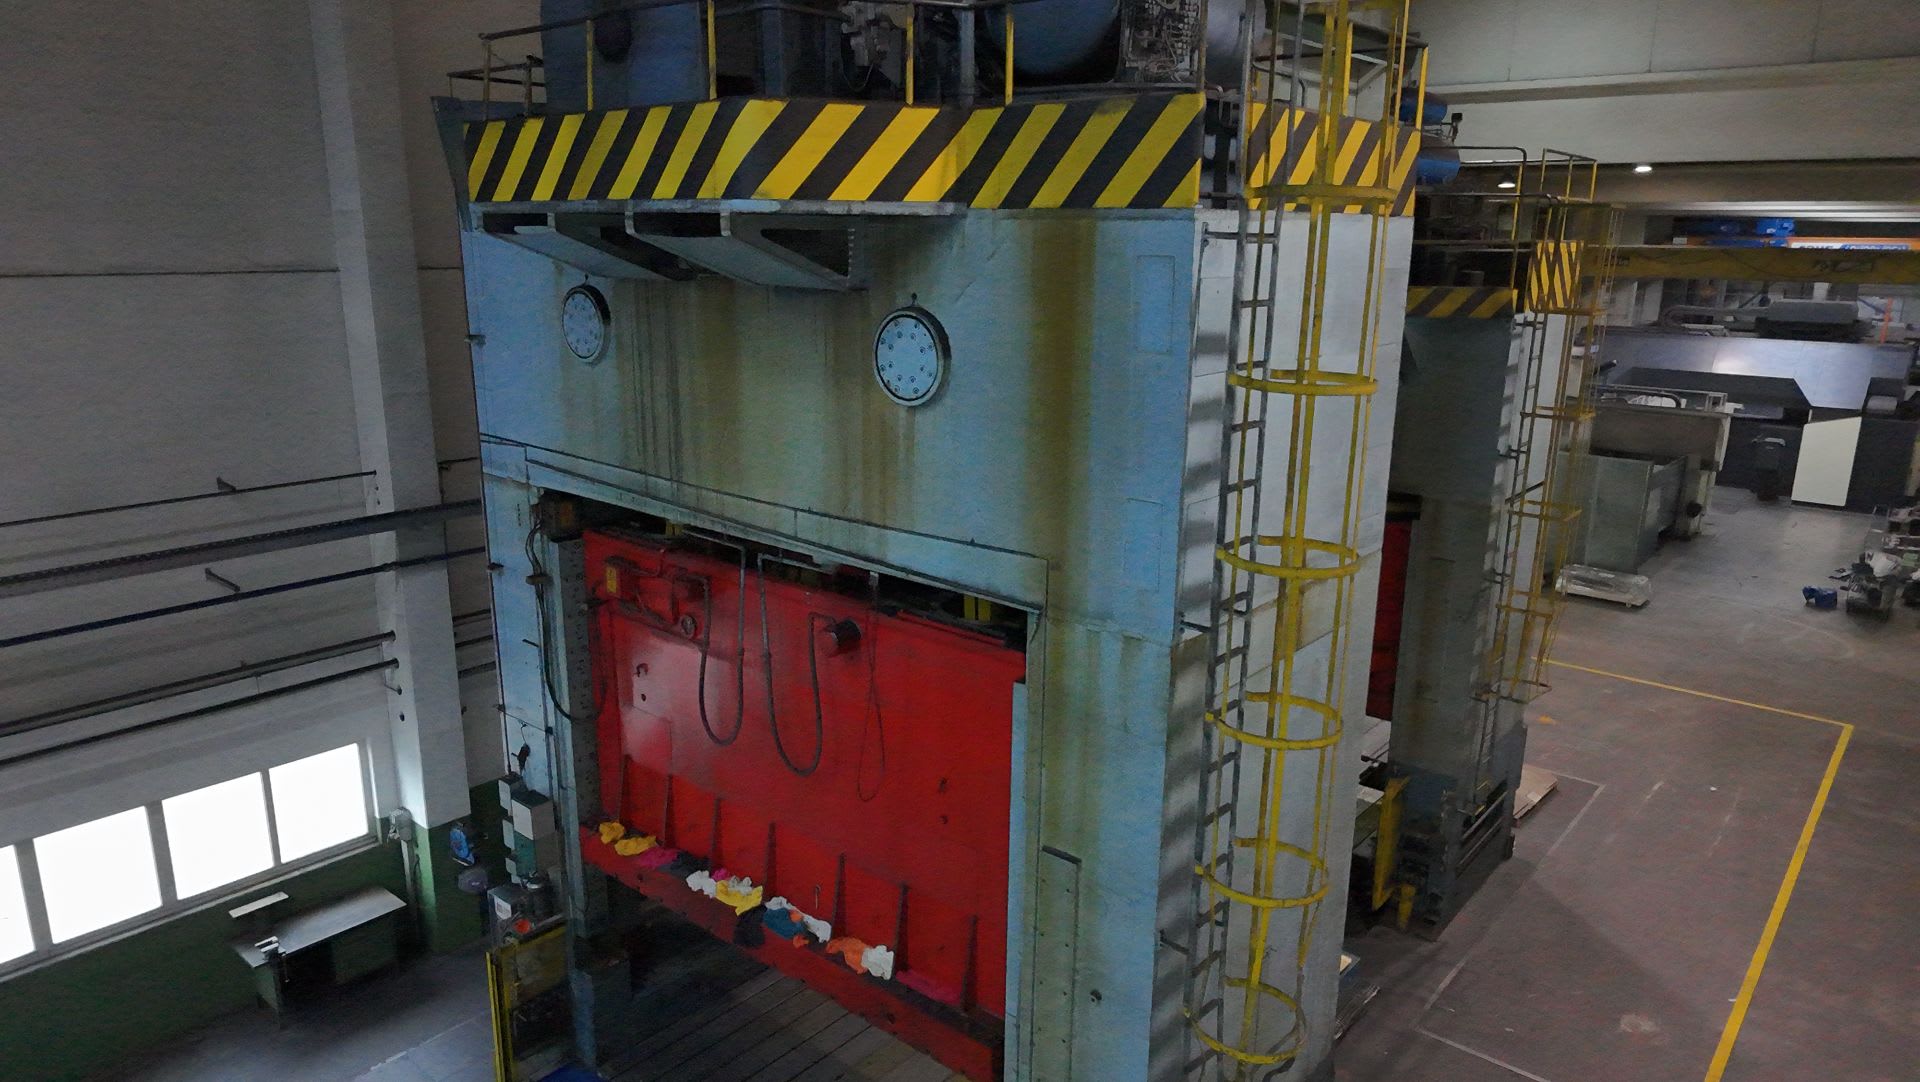
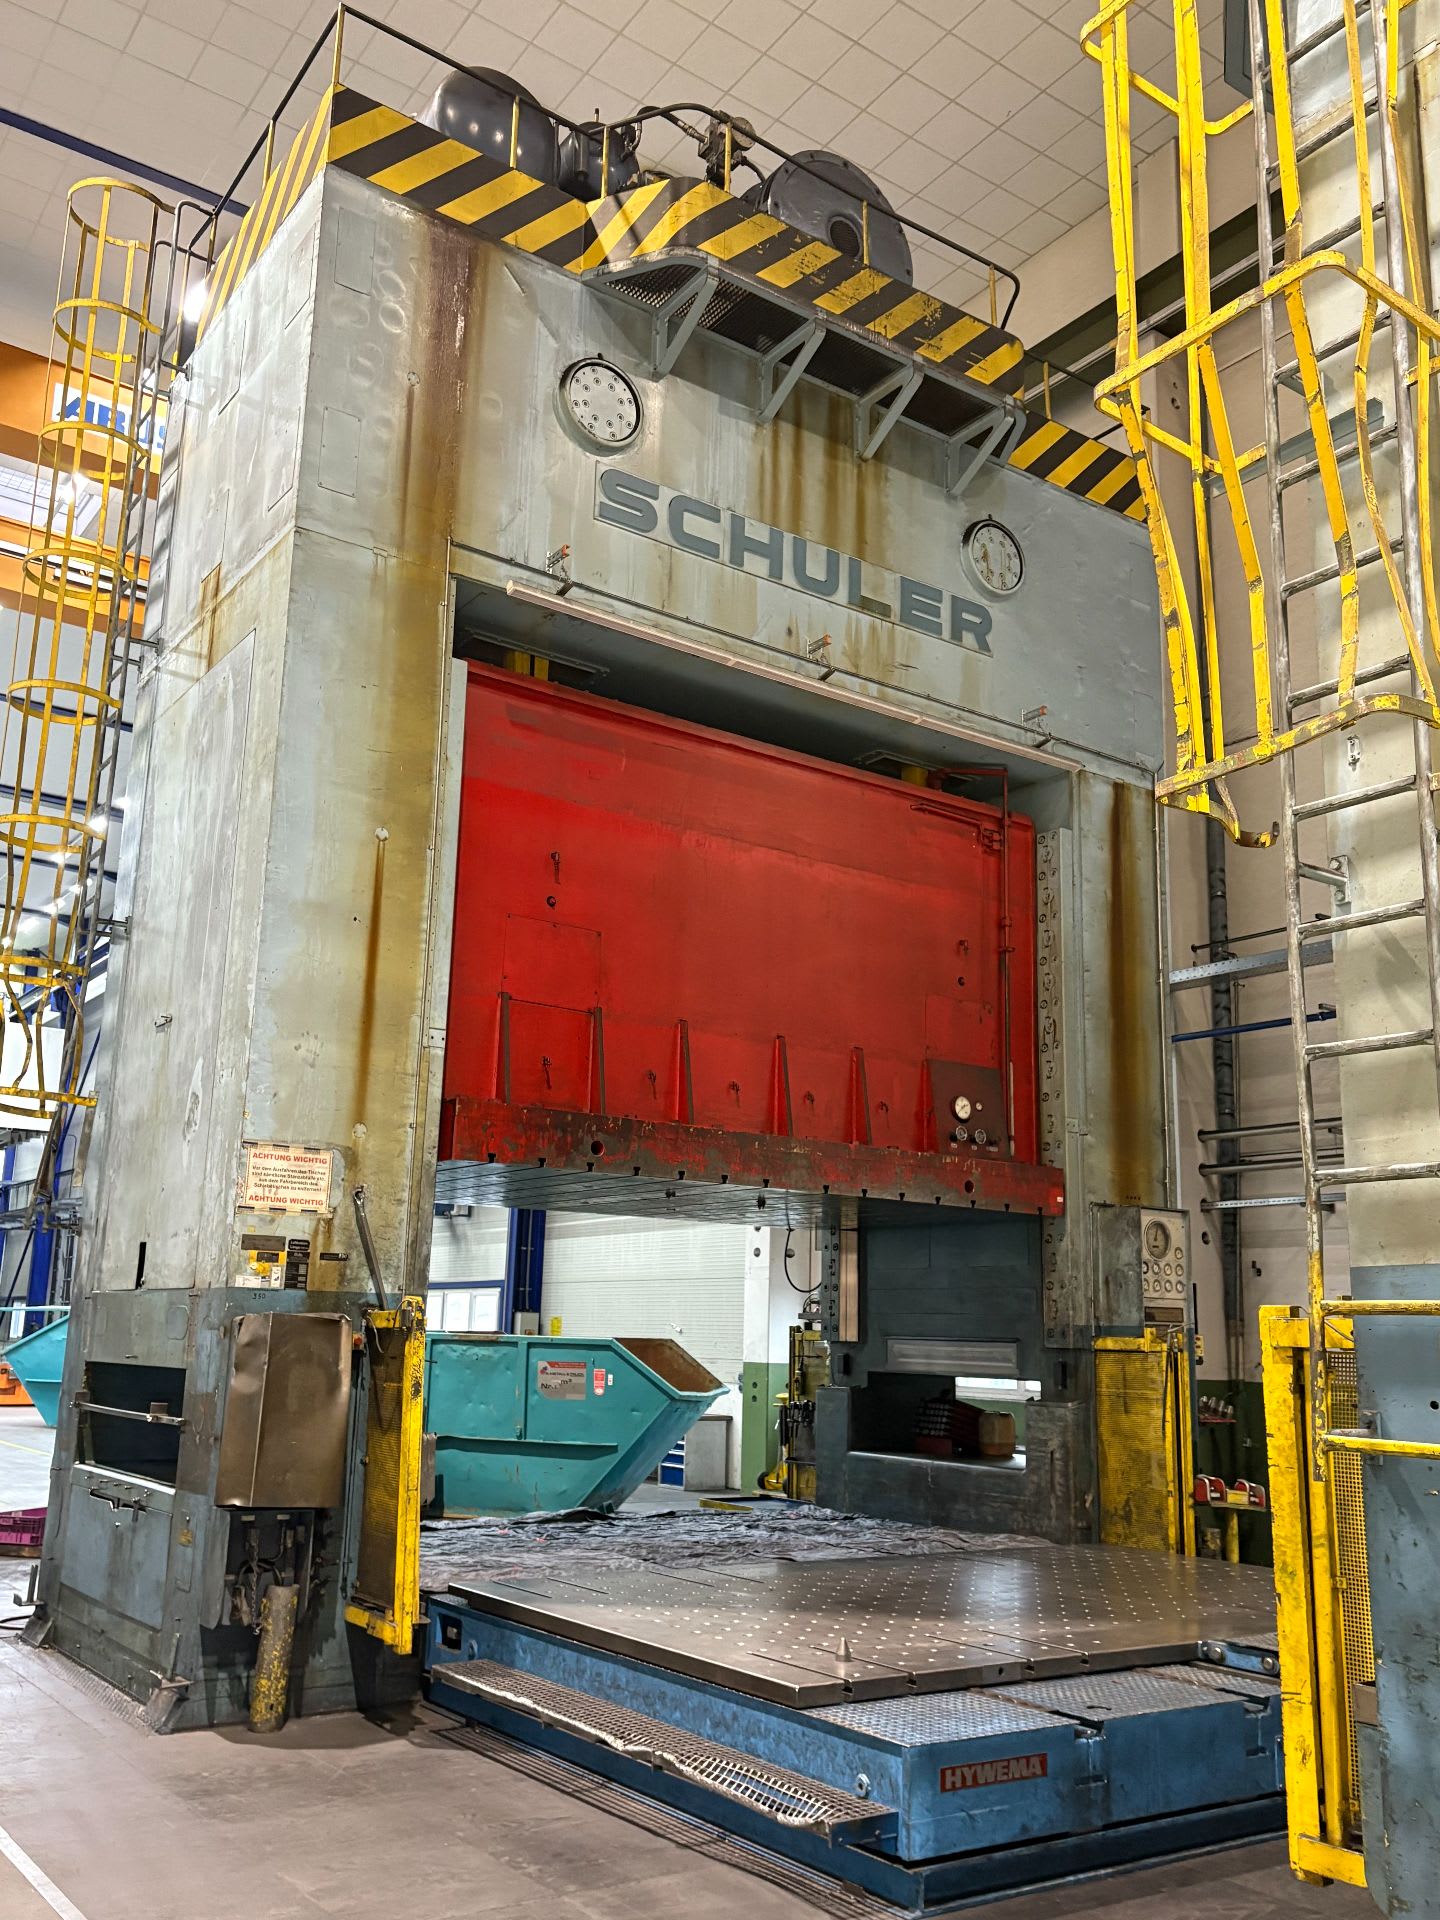
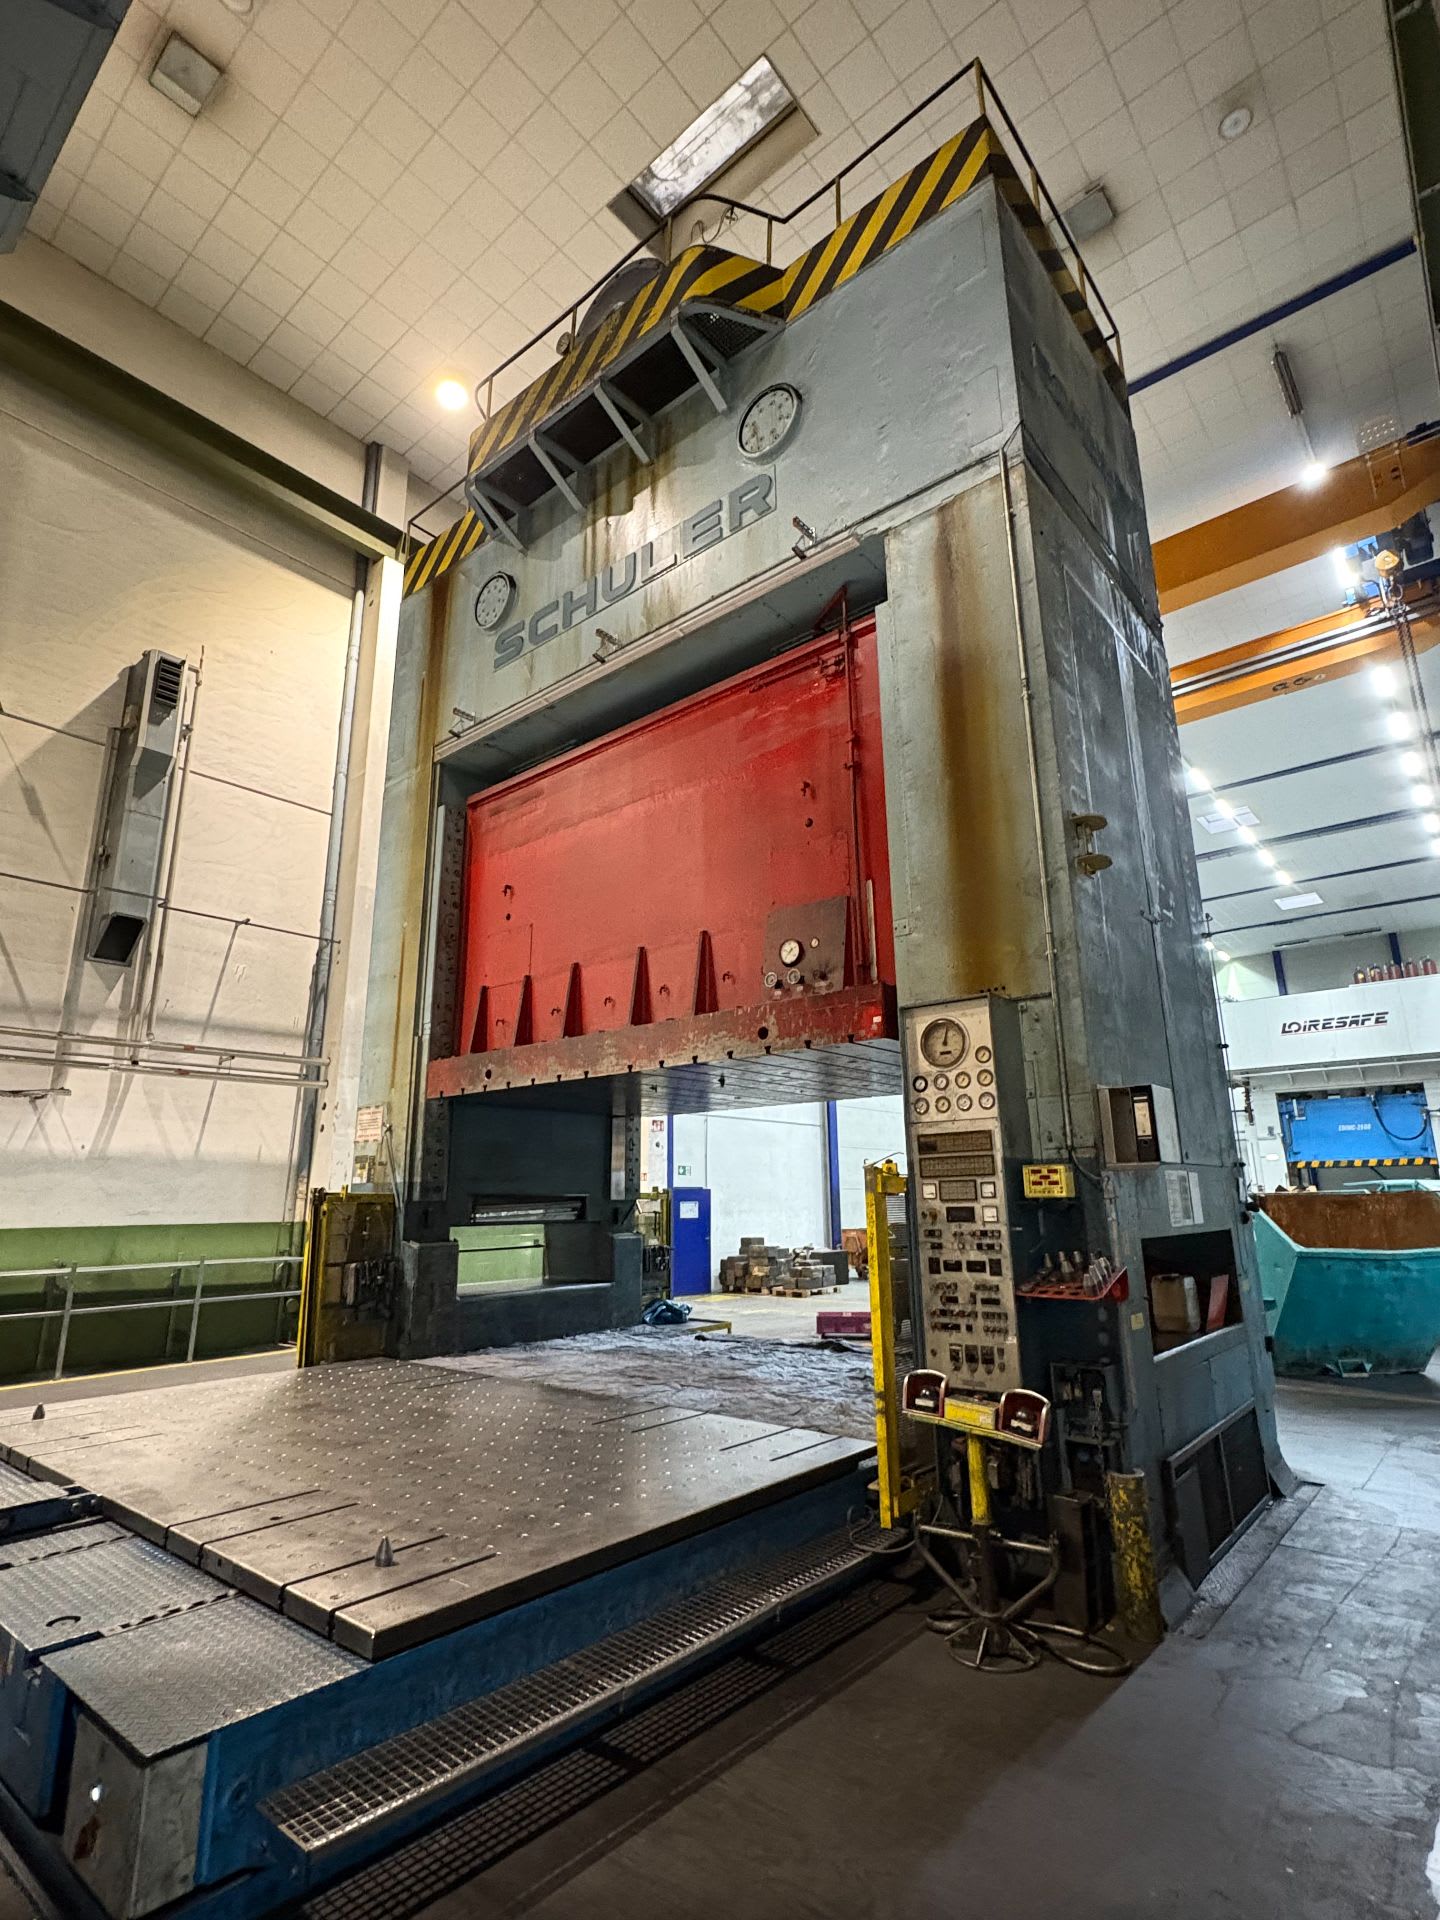
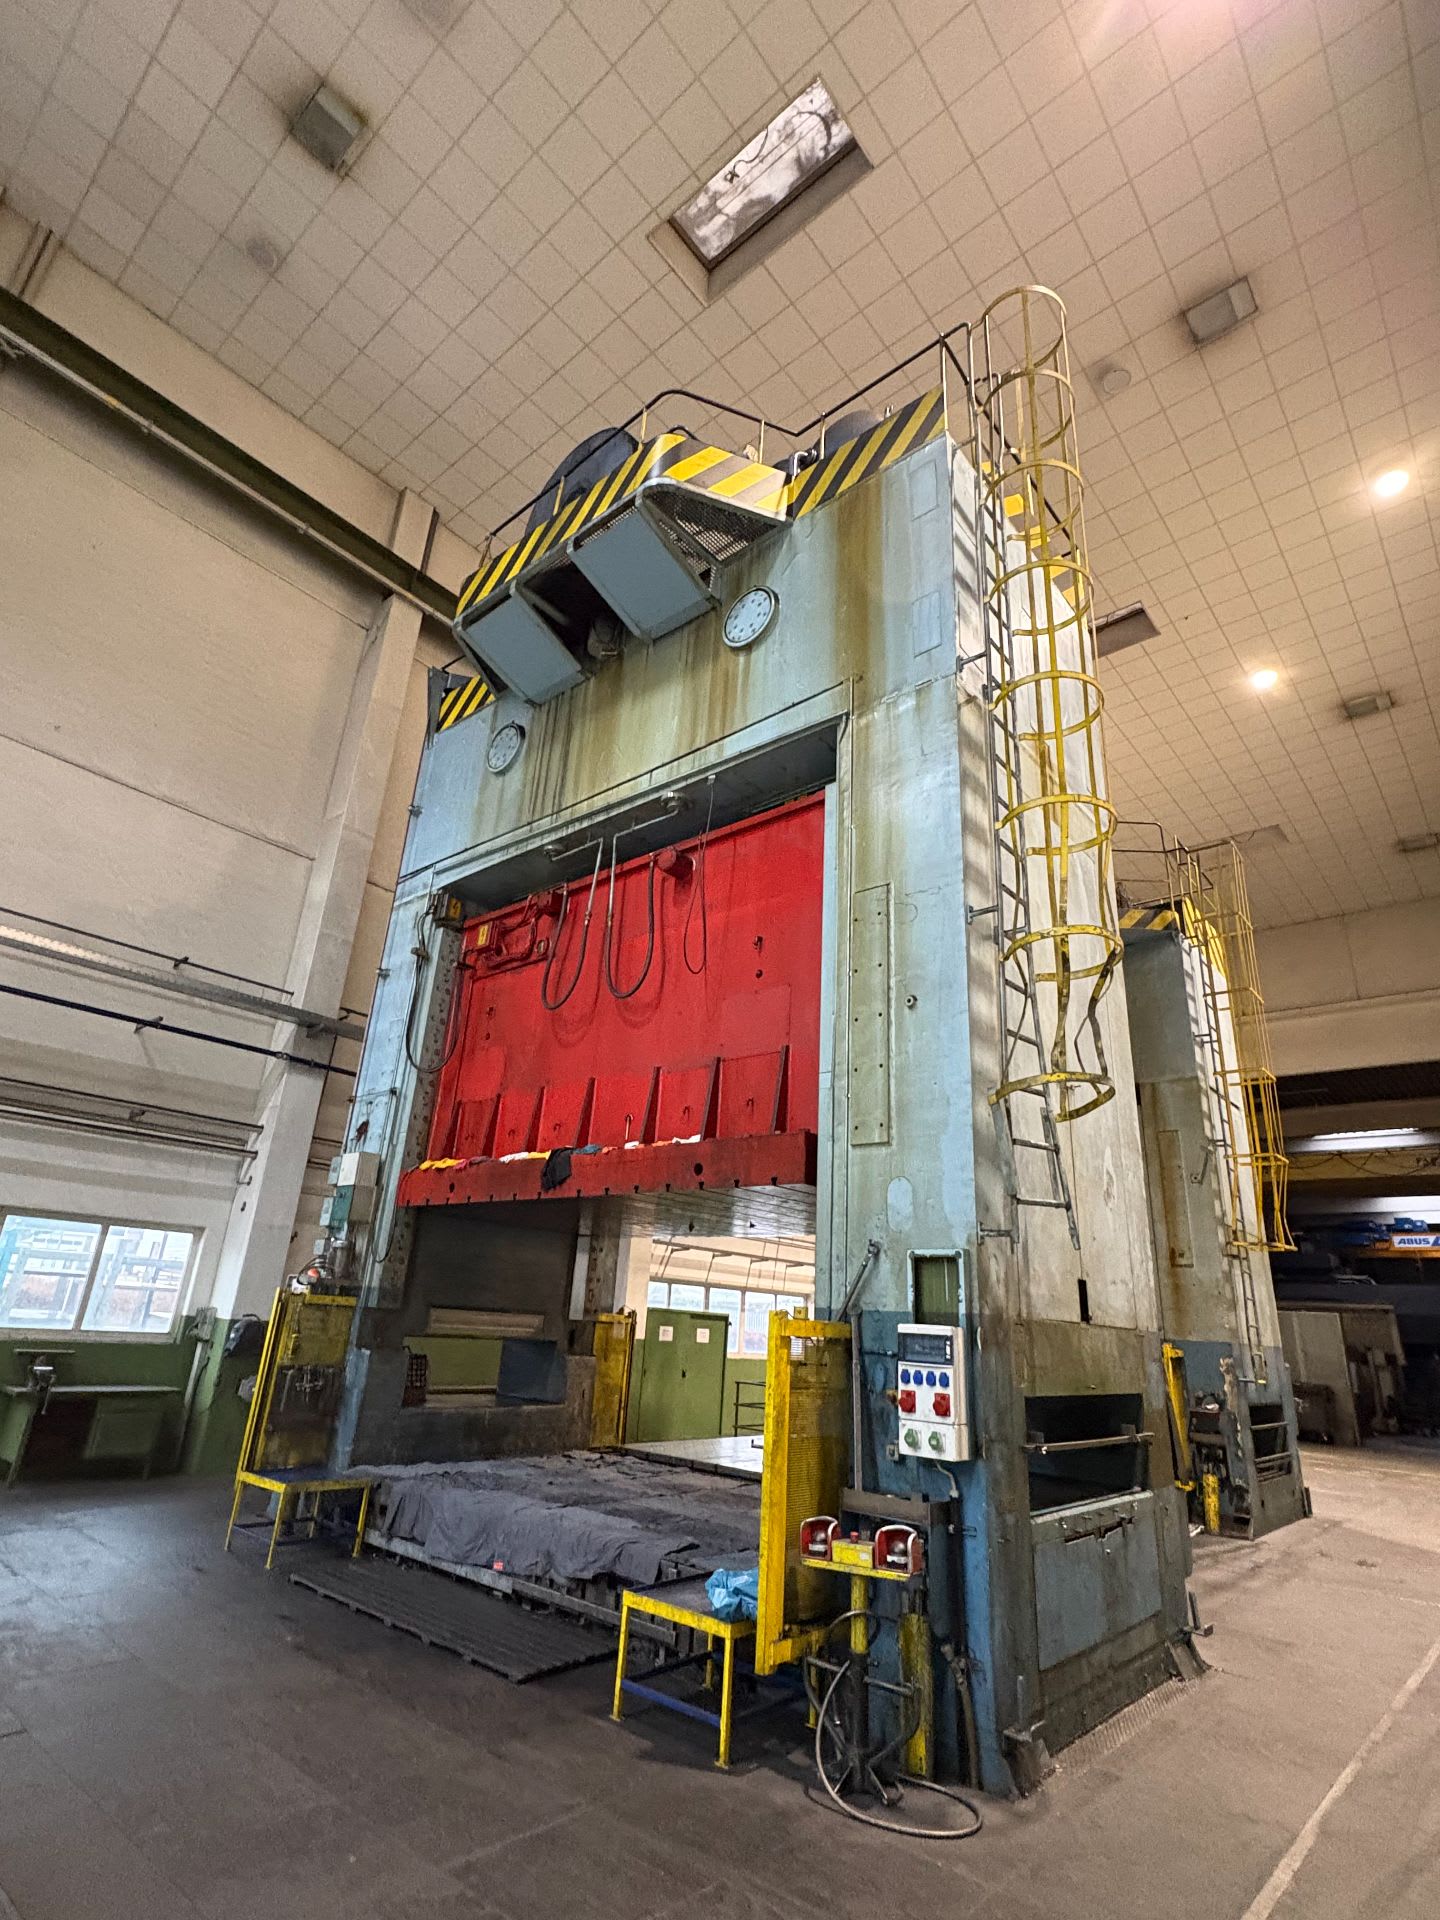
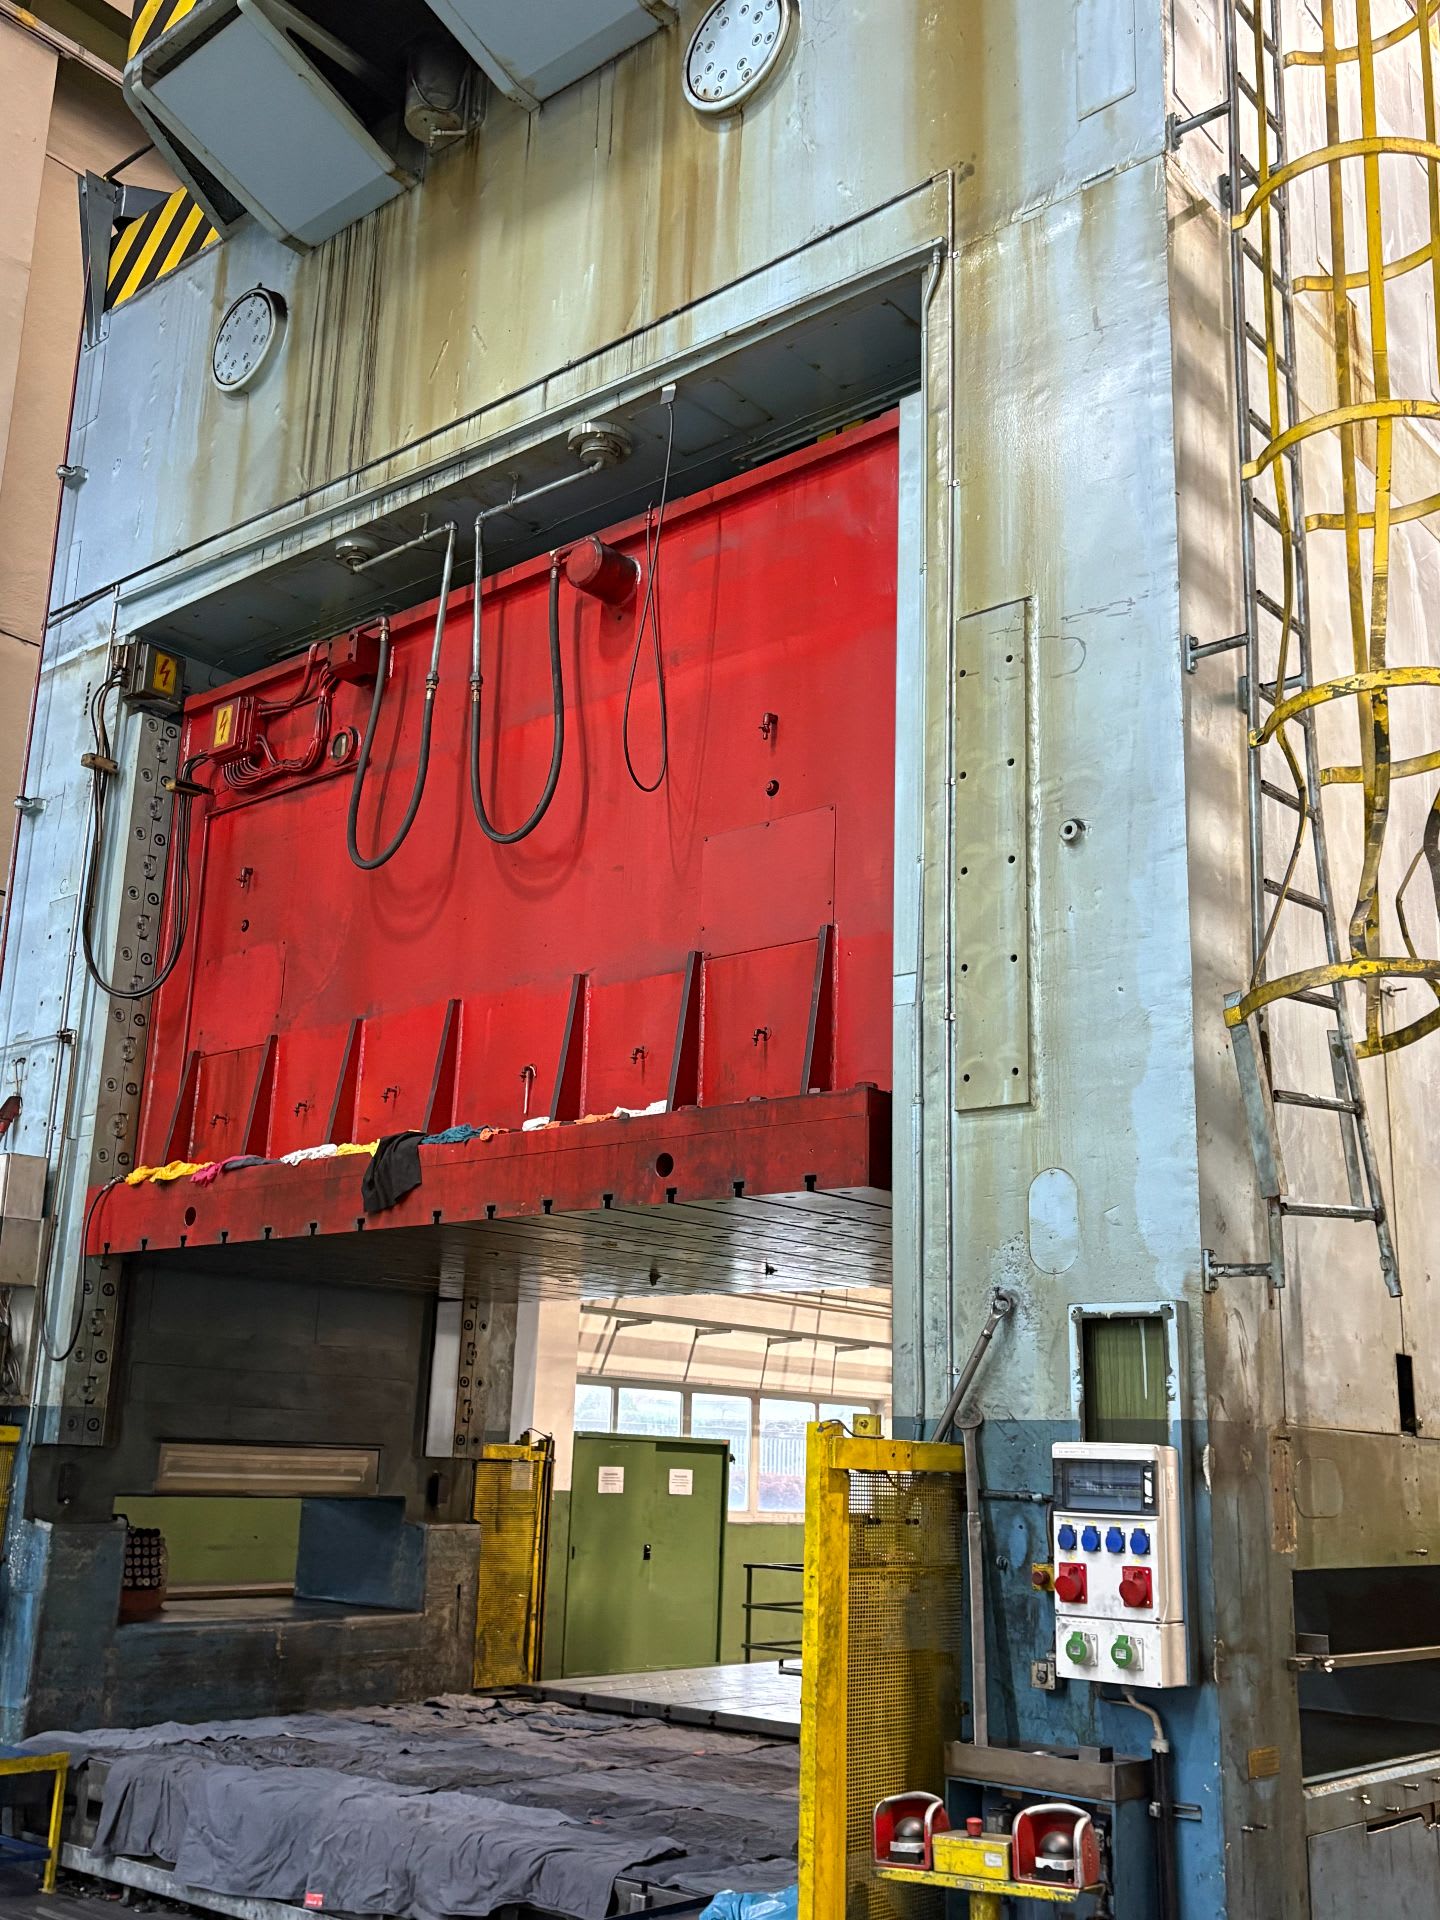
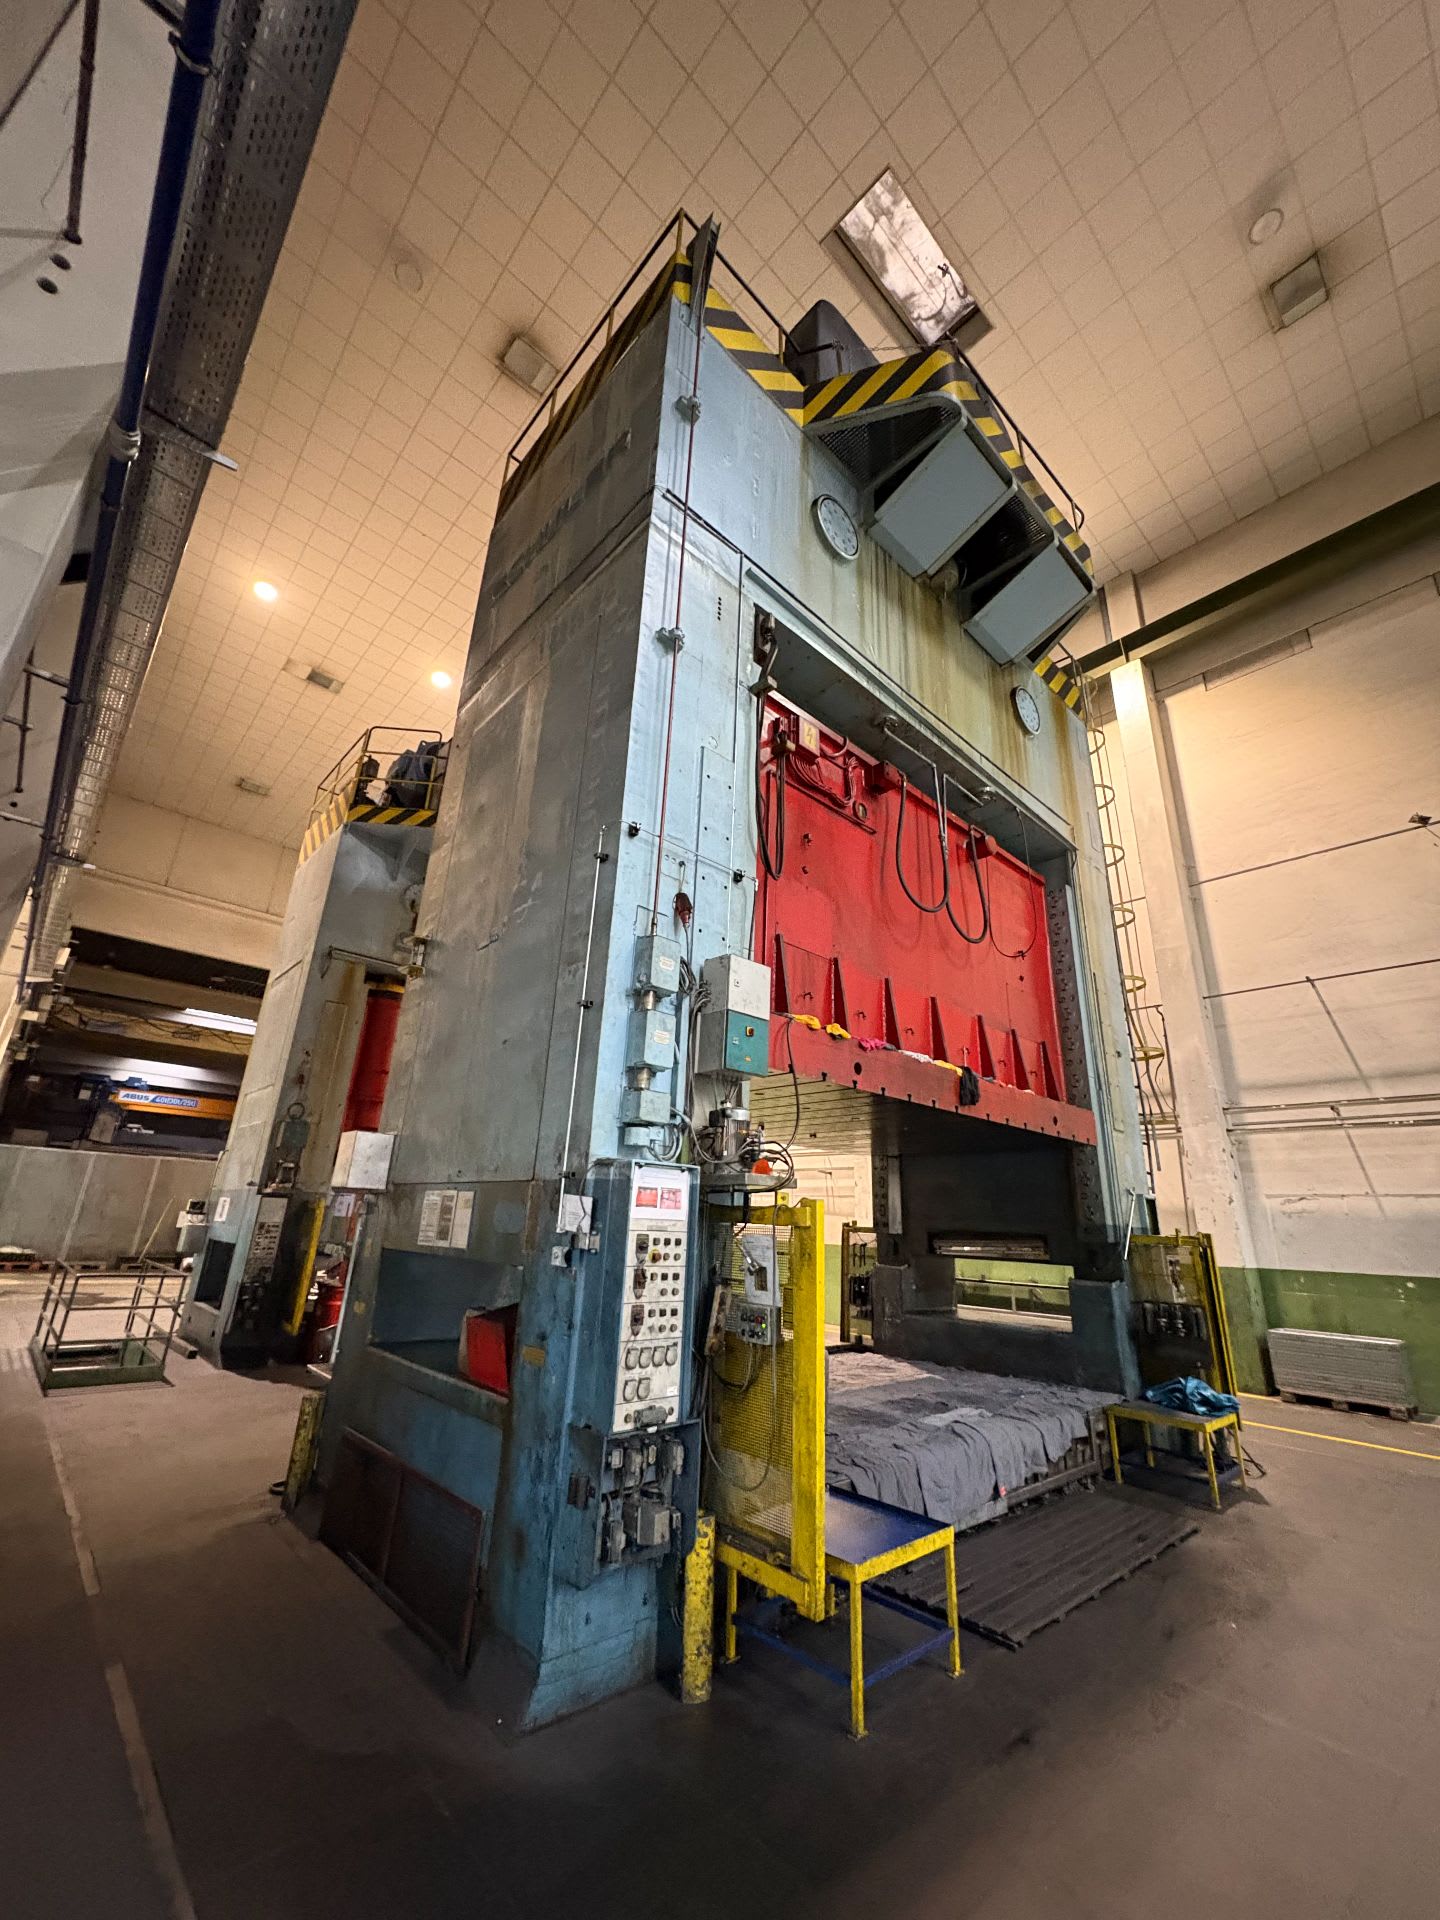
SCHULER P4 E2 SQ 1200 Mechanical Press
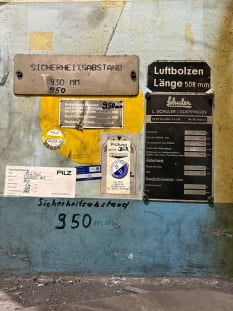
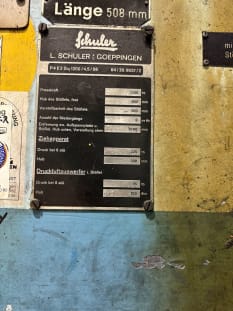
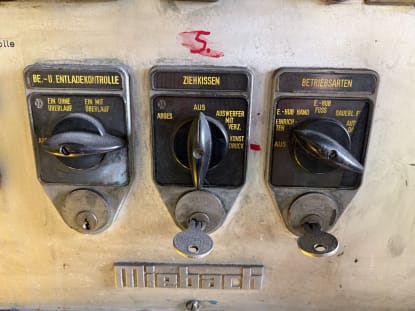
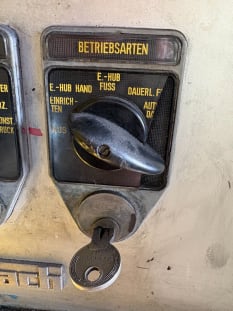

- Storage Number
- 26007-39
- Machine type
- Mechanical Presses
- Manufacturer
- SCHULER
- Type
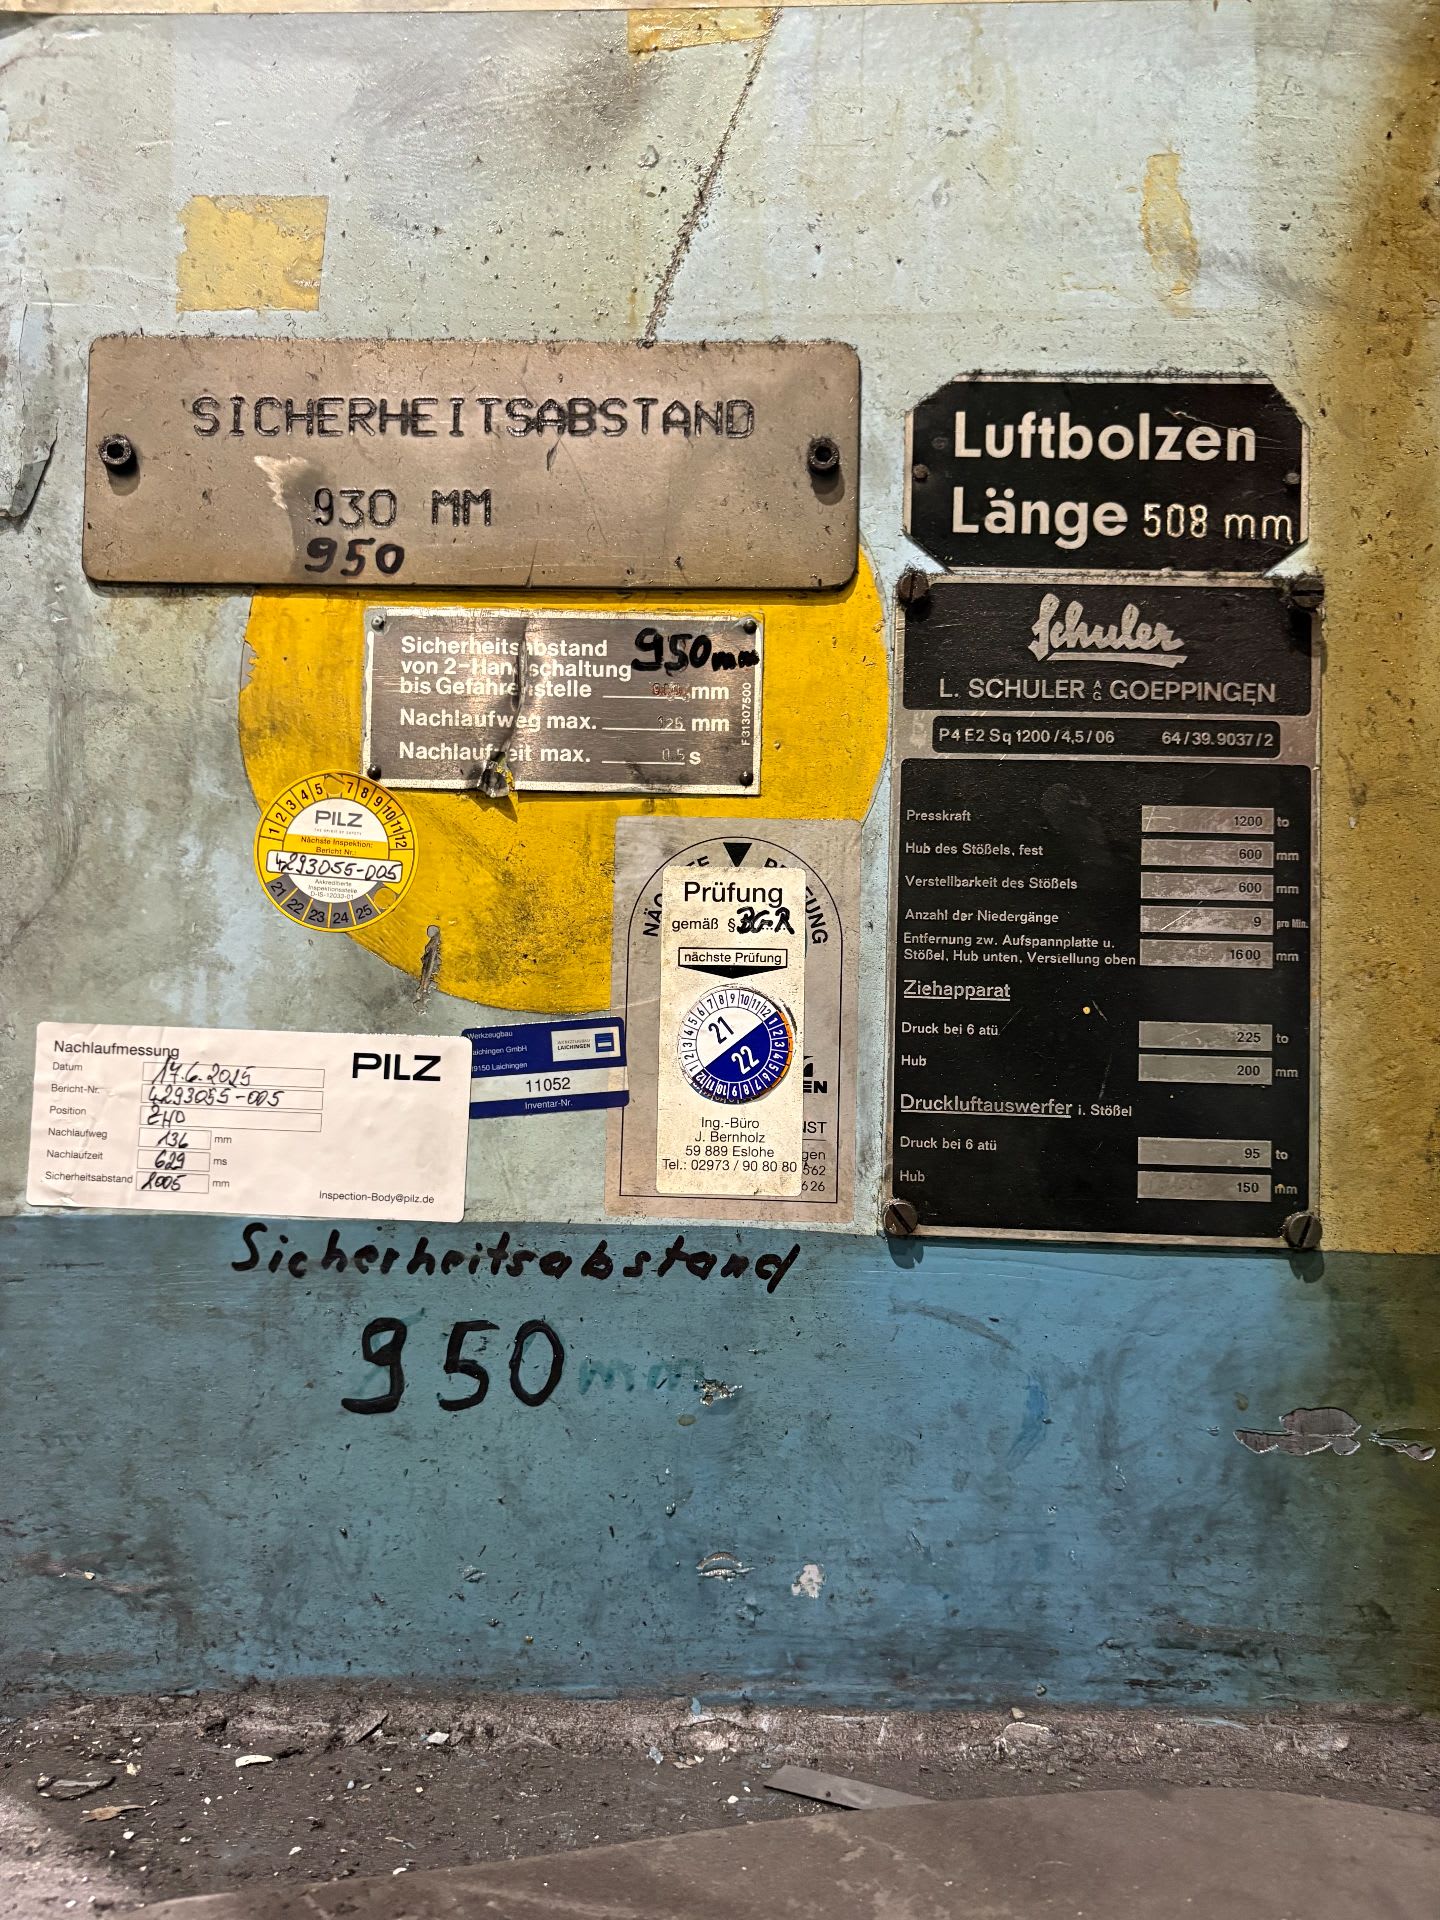
- P4 E2 SQ 1200
- Year of construction
- 1964
- Location
- Laichingen, Germany
- Availability
- immediately
- Price
- This item is sold
- Dimensions (LxWxH) approx.
- 7600 x 6000 x 10000 mm
- Installation height max.
- 1,600 mm
- Machine table clamping surface
- 4500 x 2700 mm
- Passage between the uprights
- 5,200 mm
- Pressing force max.
- 1,200 t
- Serial number
- 64 / 39.9037 / 2
- Weight approx.
- 400,000 kg
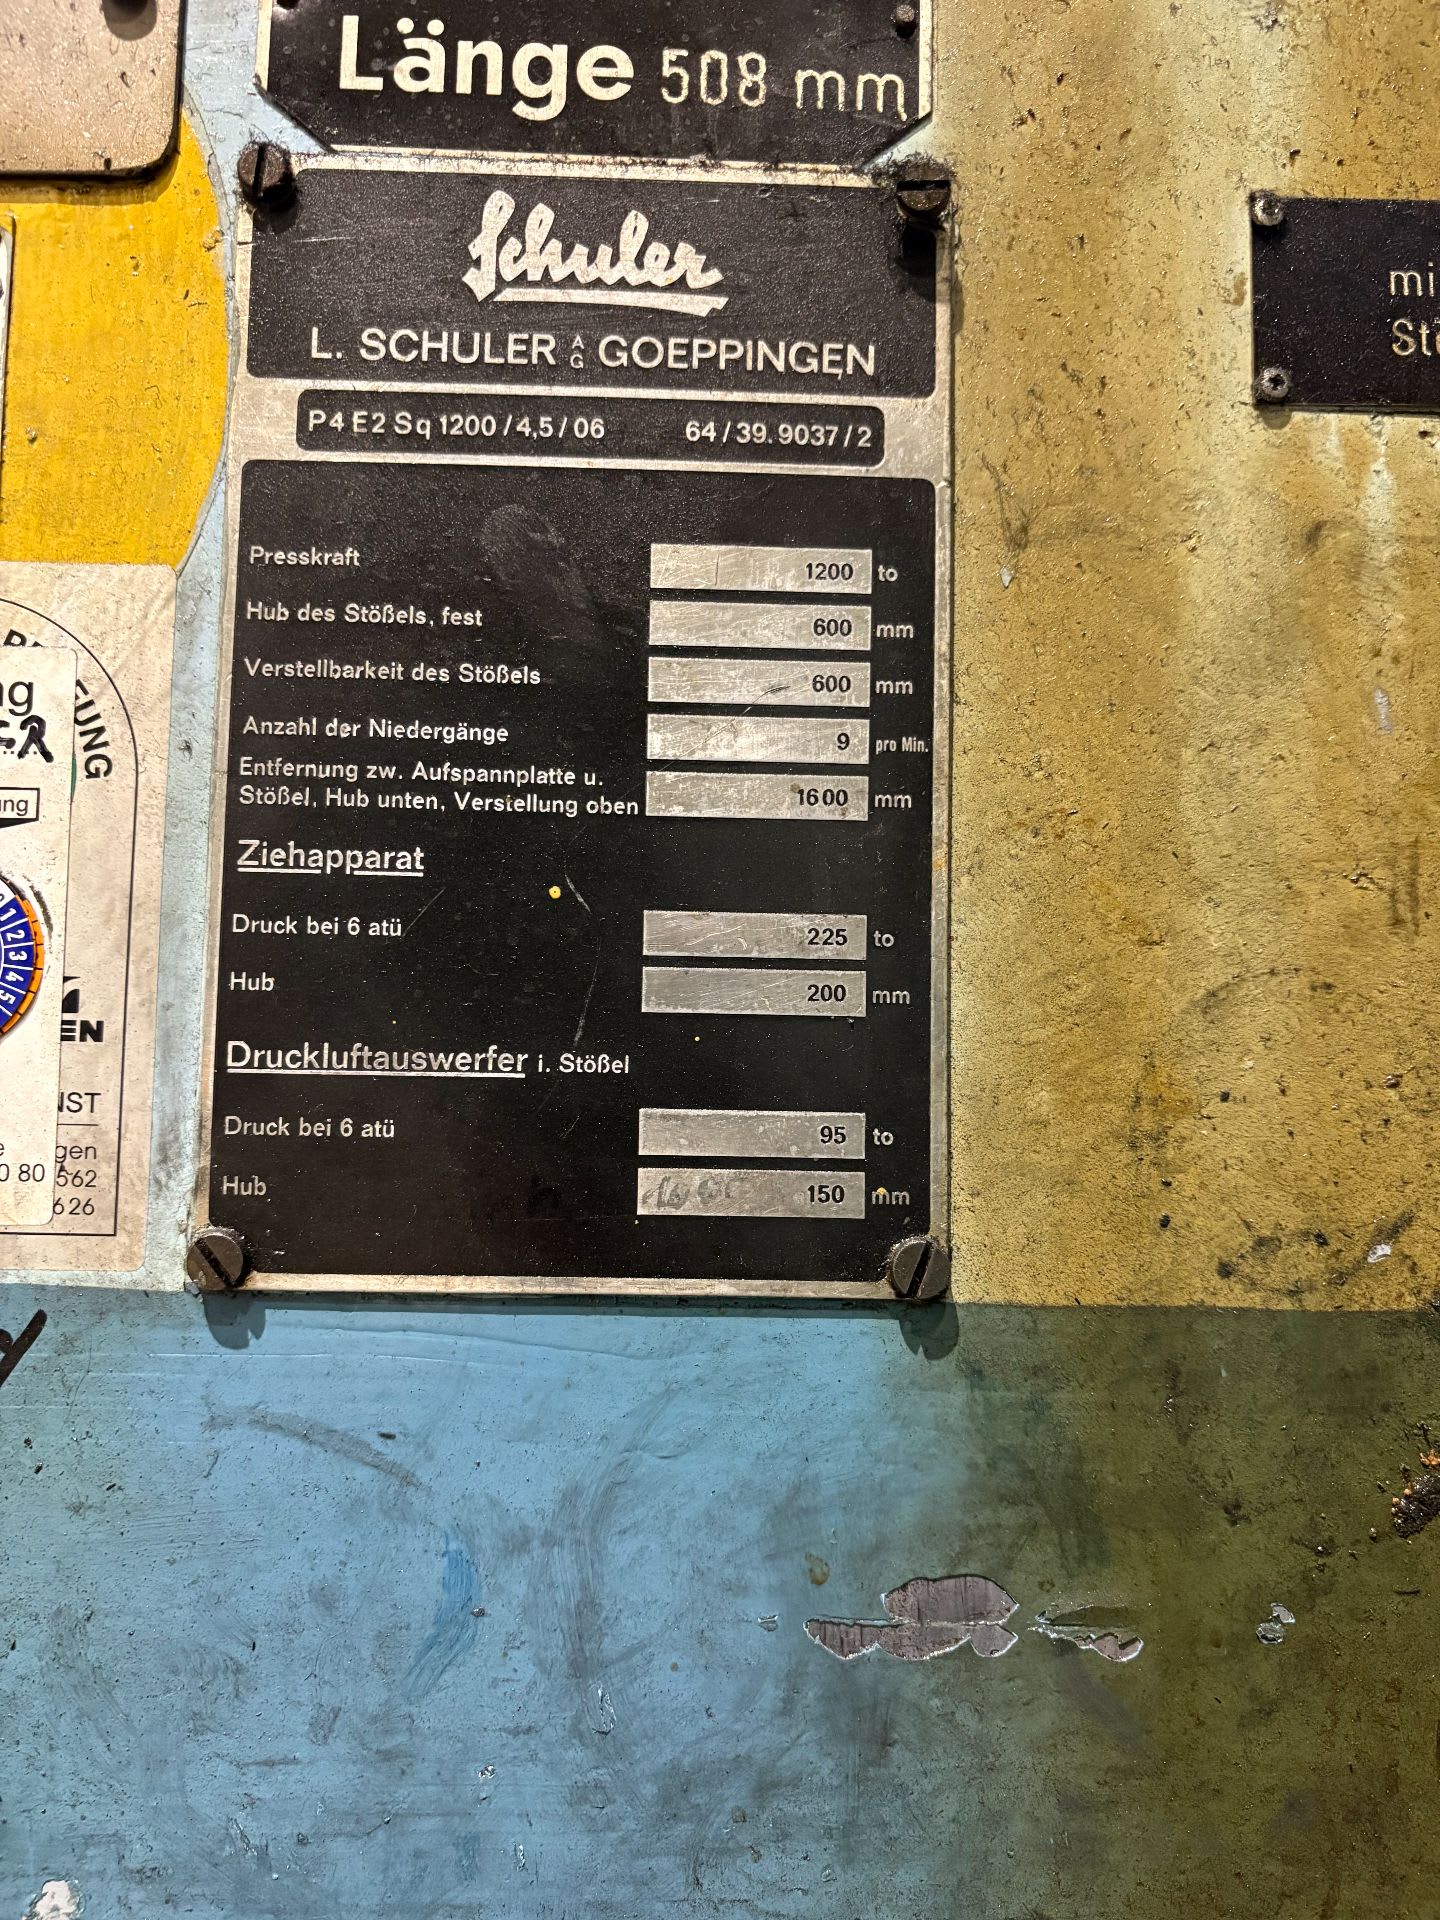
Press force: 1,200 t
Ram stroke: 600 mm
Ram adjustment: 600 mm
Stroke rate: approx. 9 strokes/min
Shut height: approx. 1,600 mm
Drawing equipment:
Drawing cushion force: approx. 225 t
Drawing cushion stroke: approx. 200 mm
Pneumatic ejector in ram:
Force: approx. 95 t
Stroke: approx. 150 mm
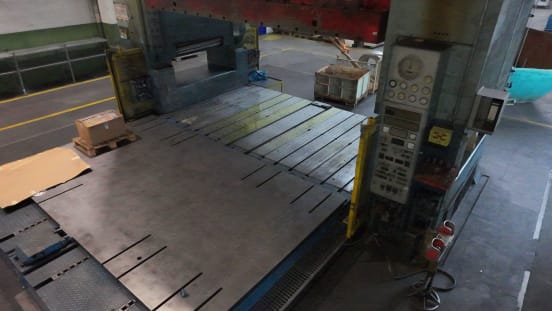
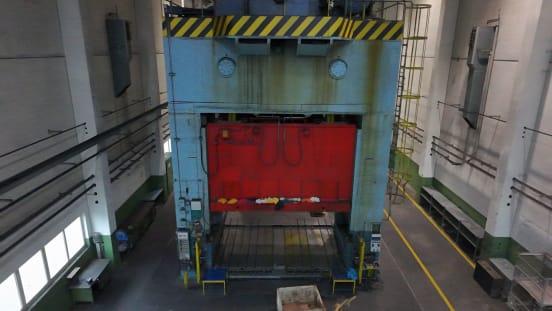
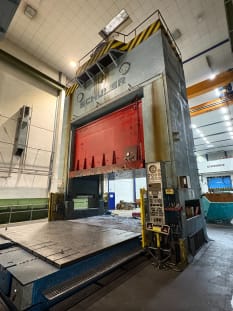
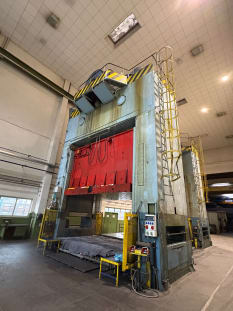
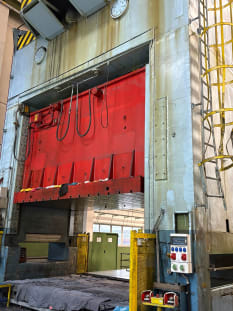
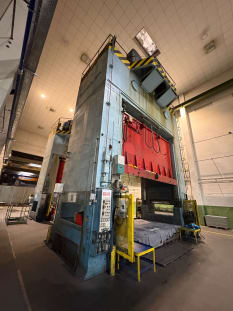
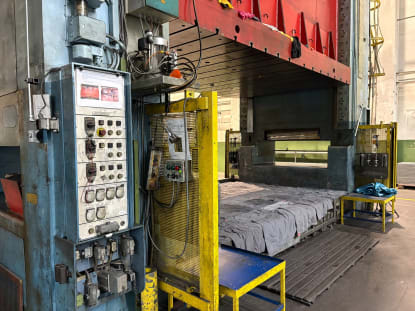
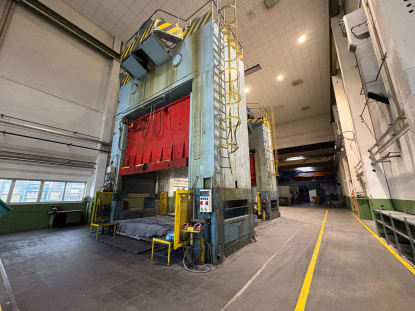
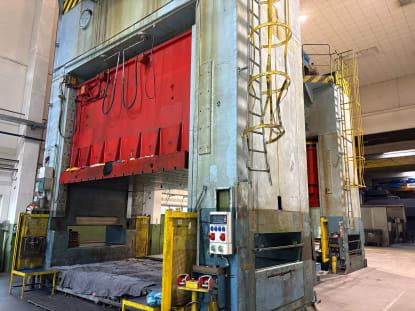
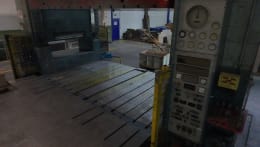
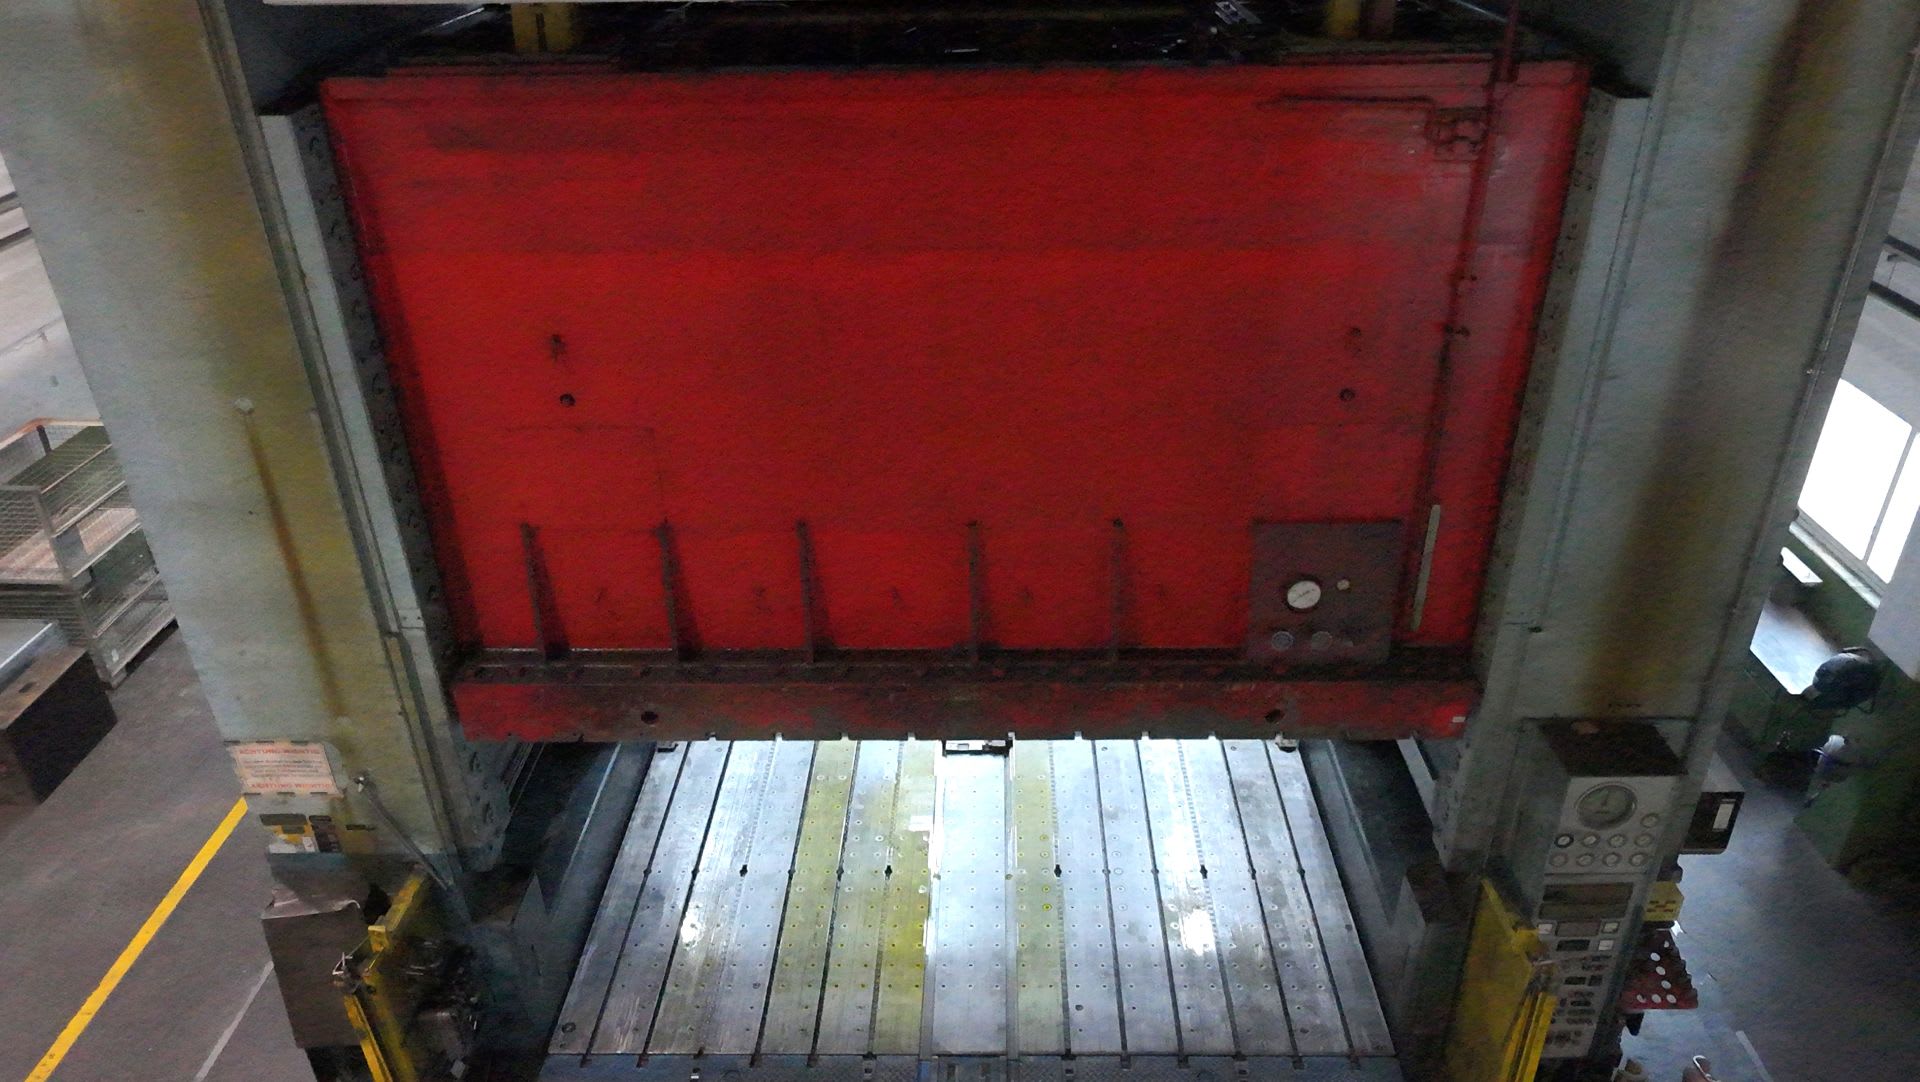
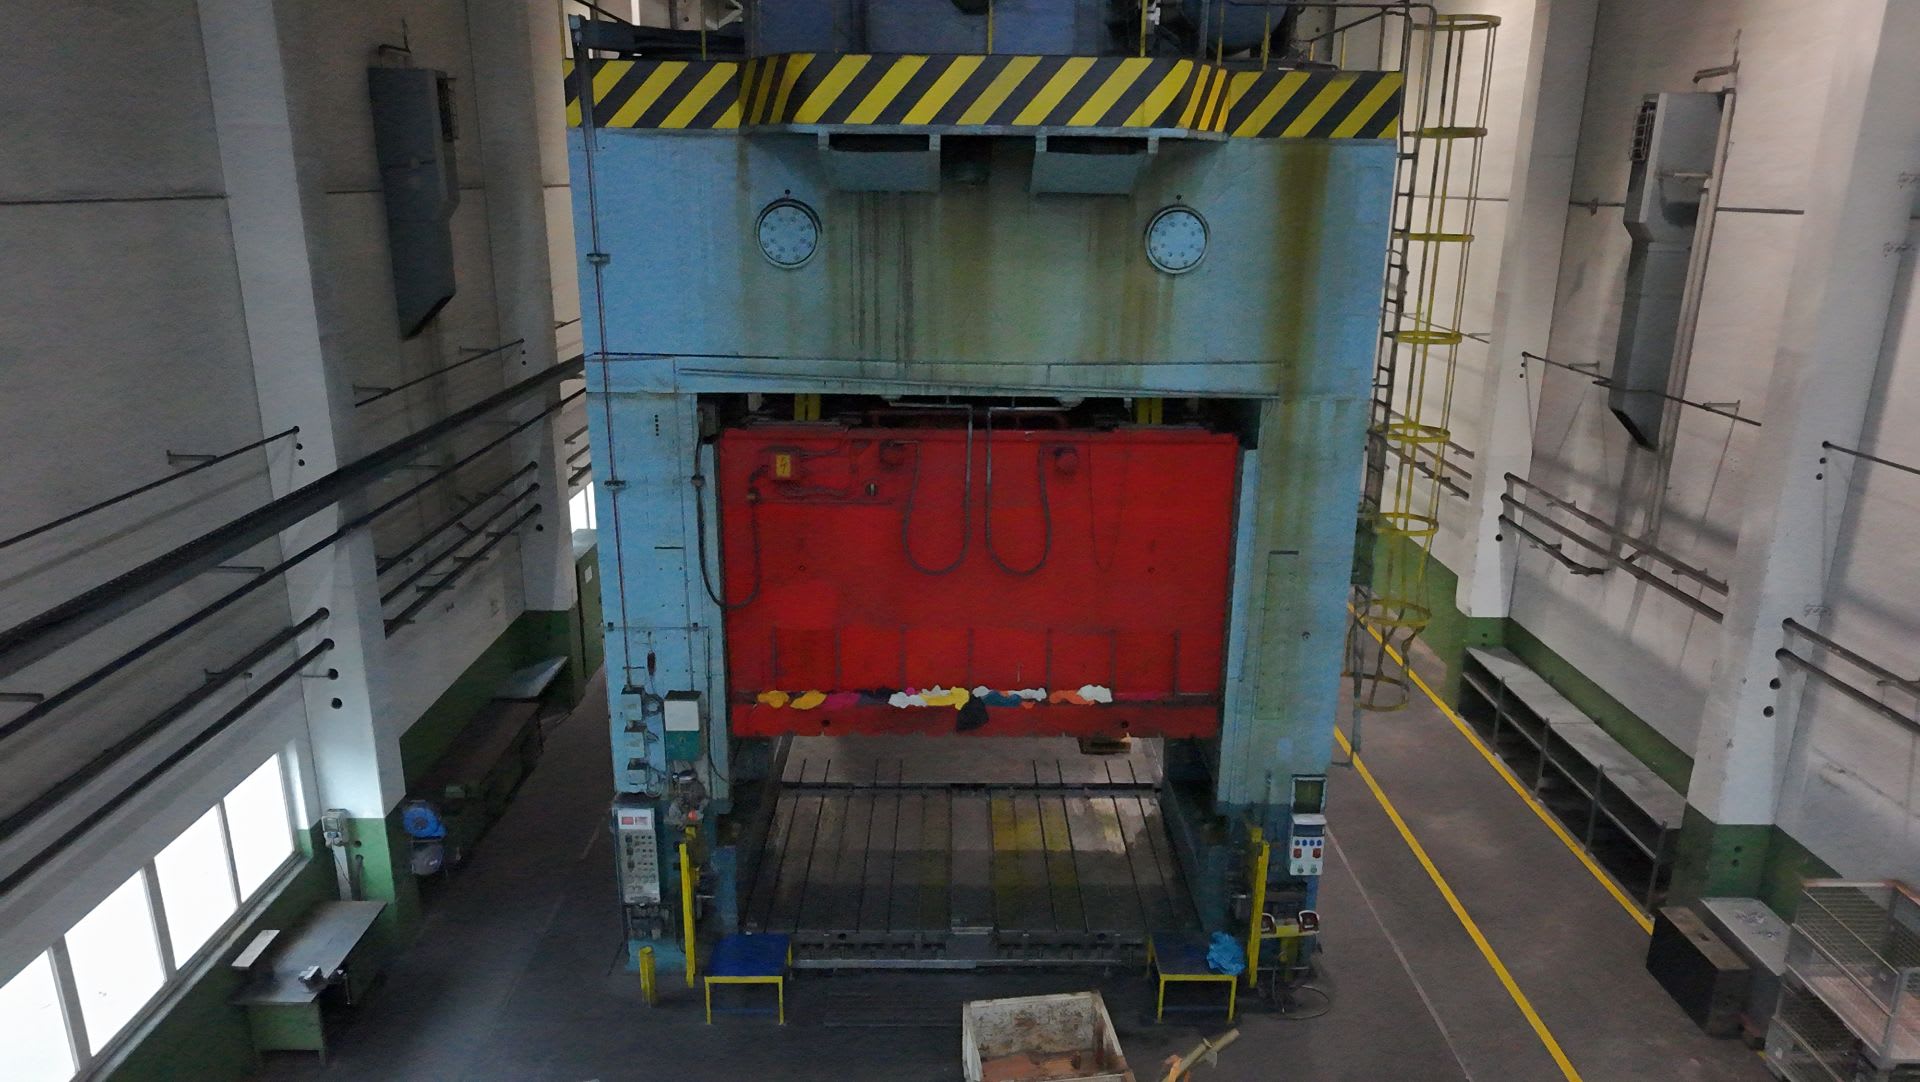
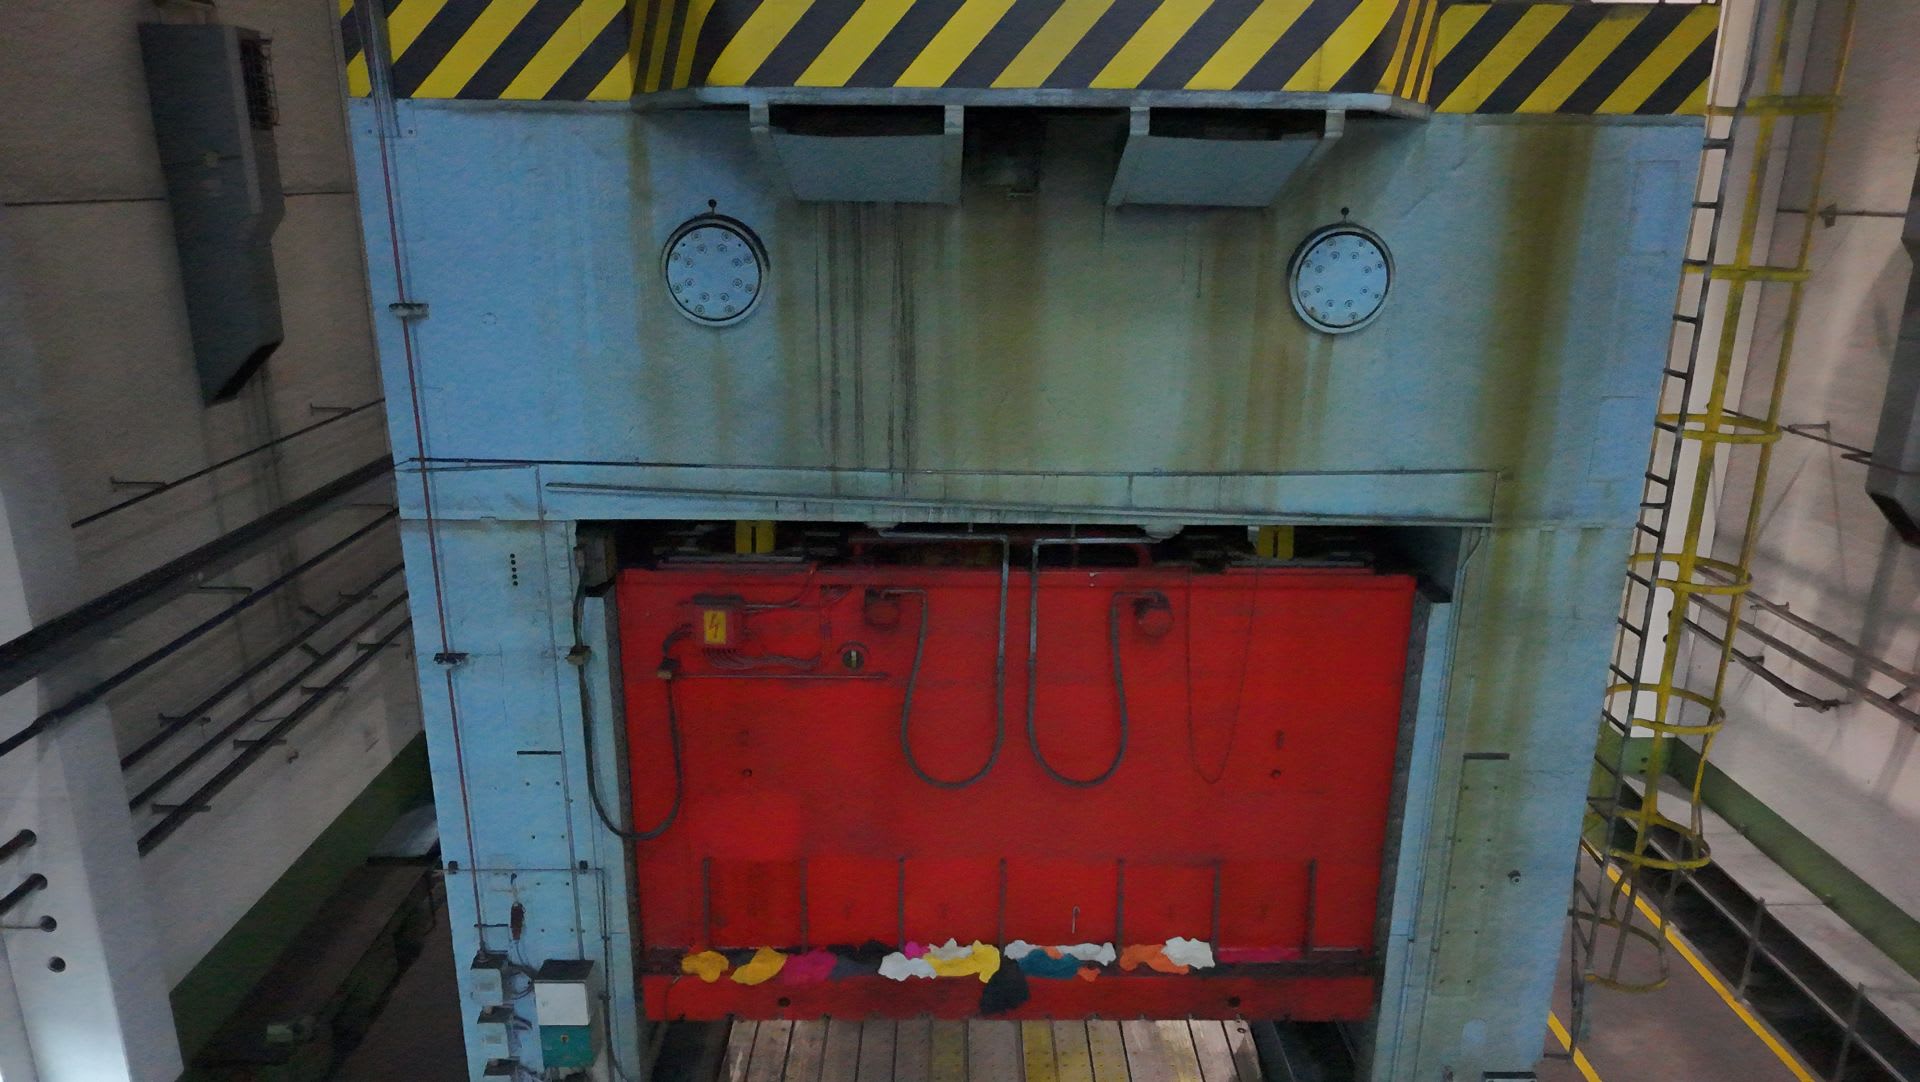
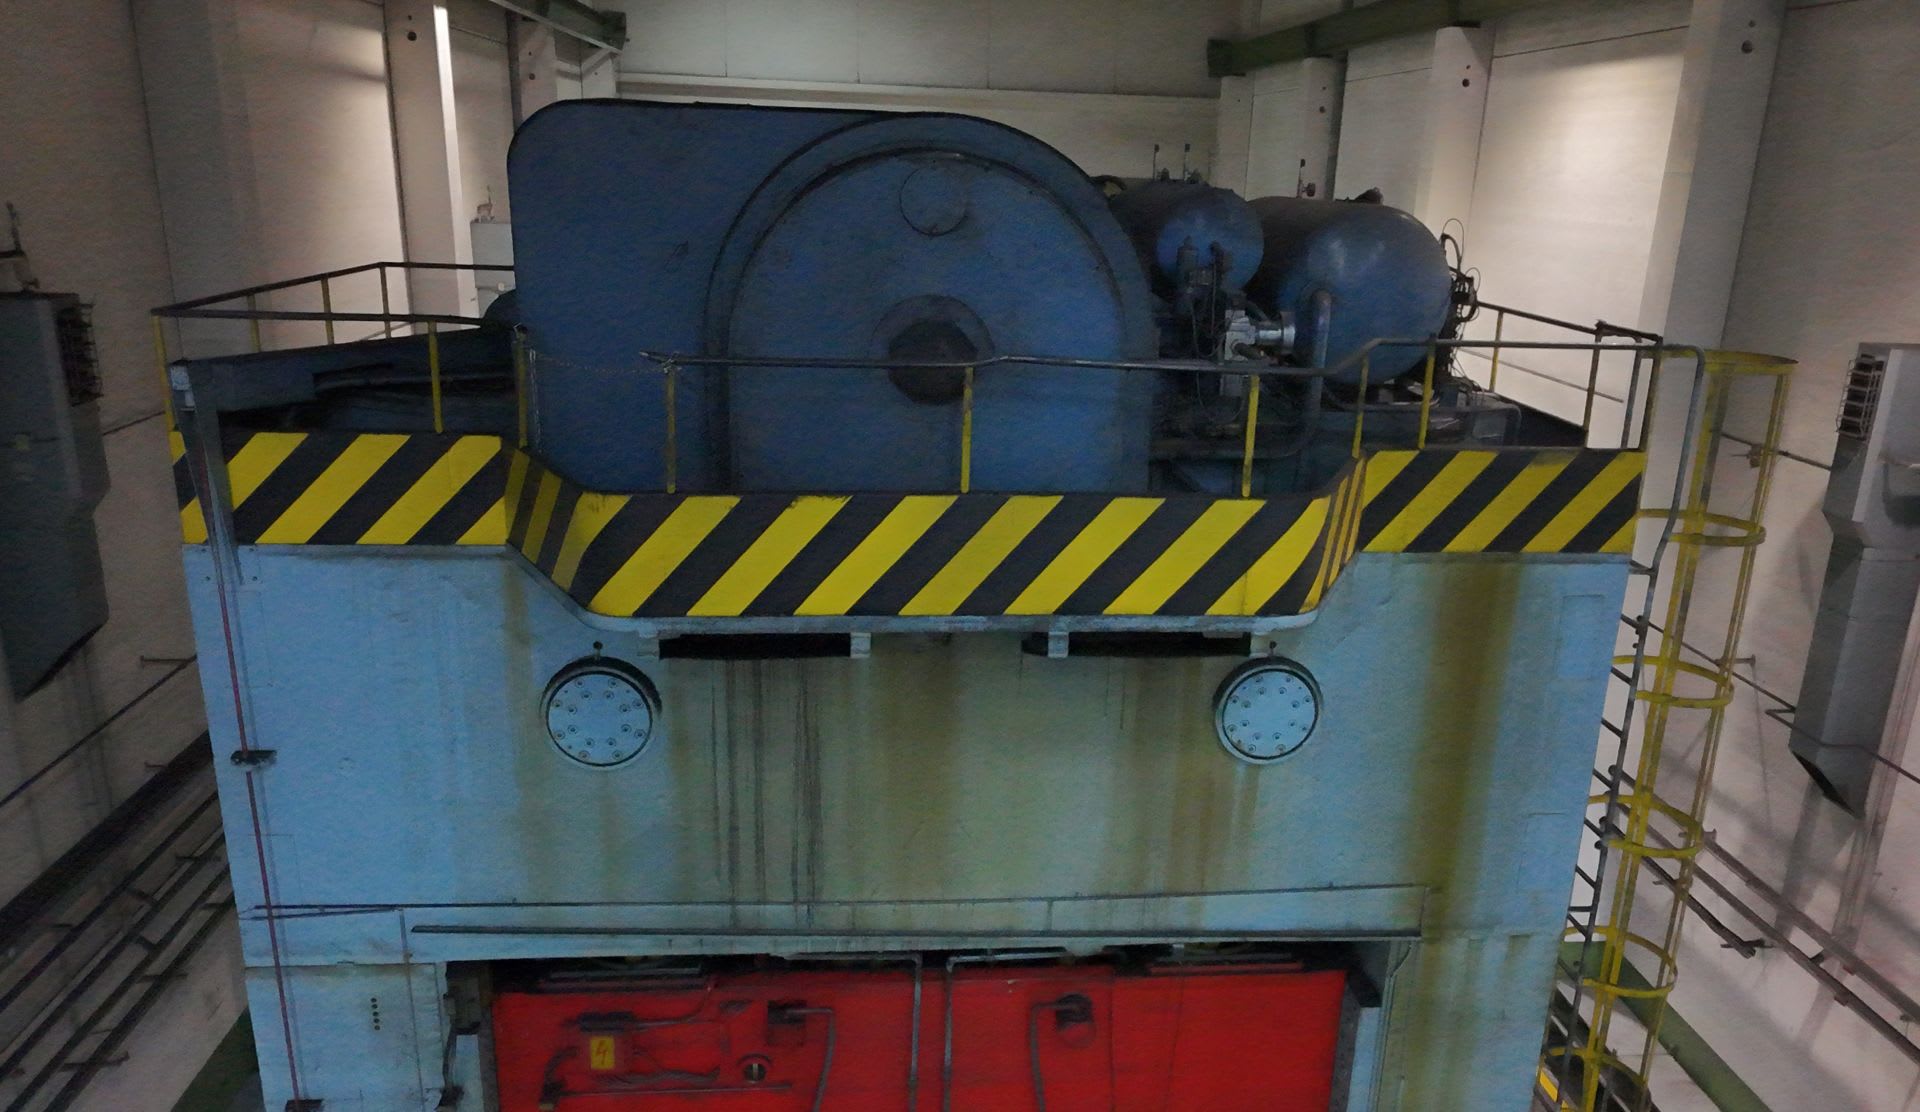
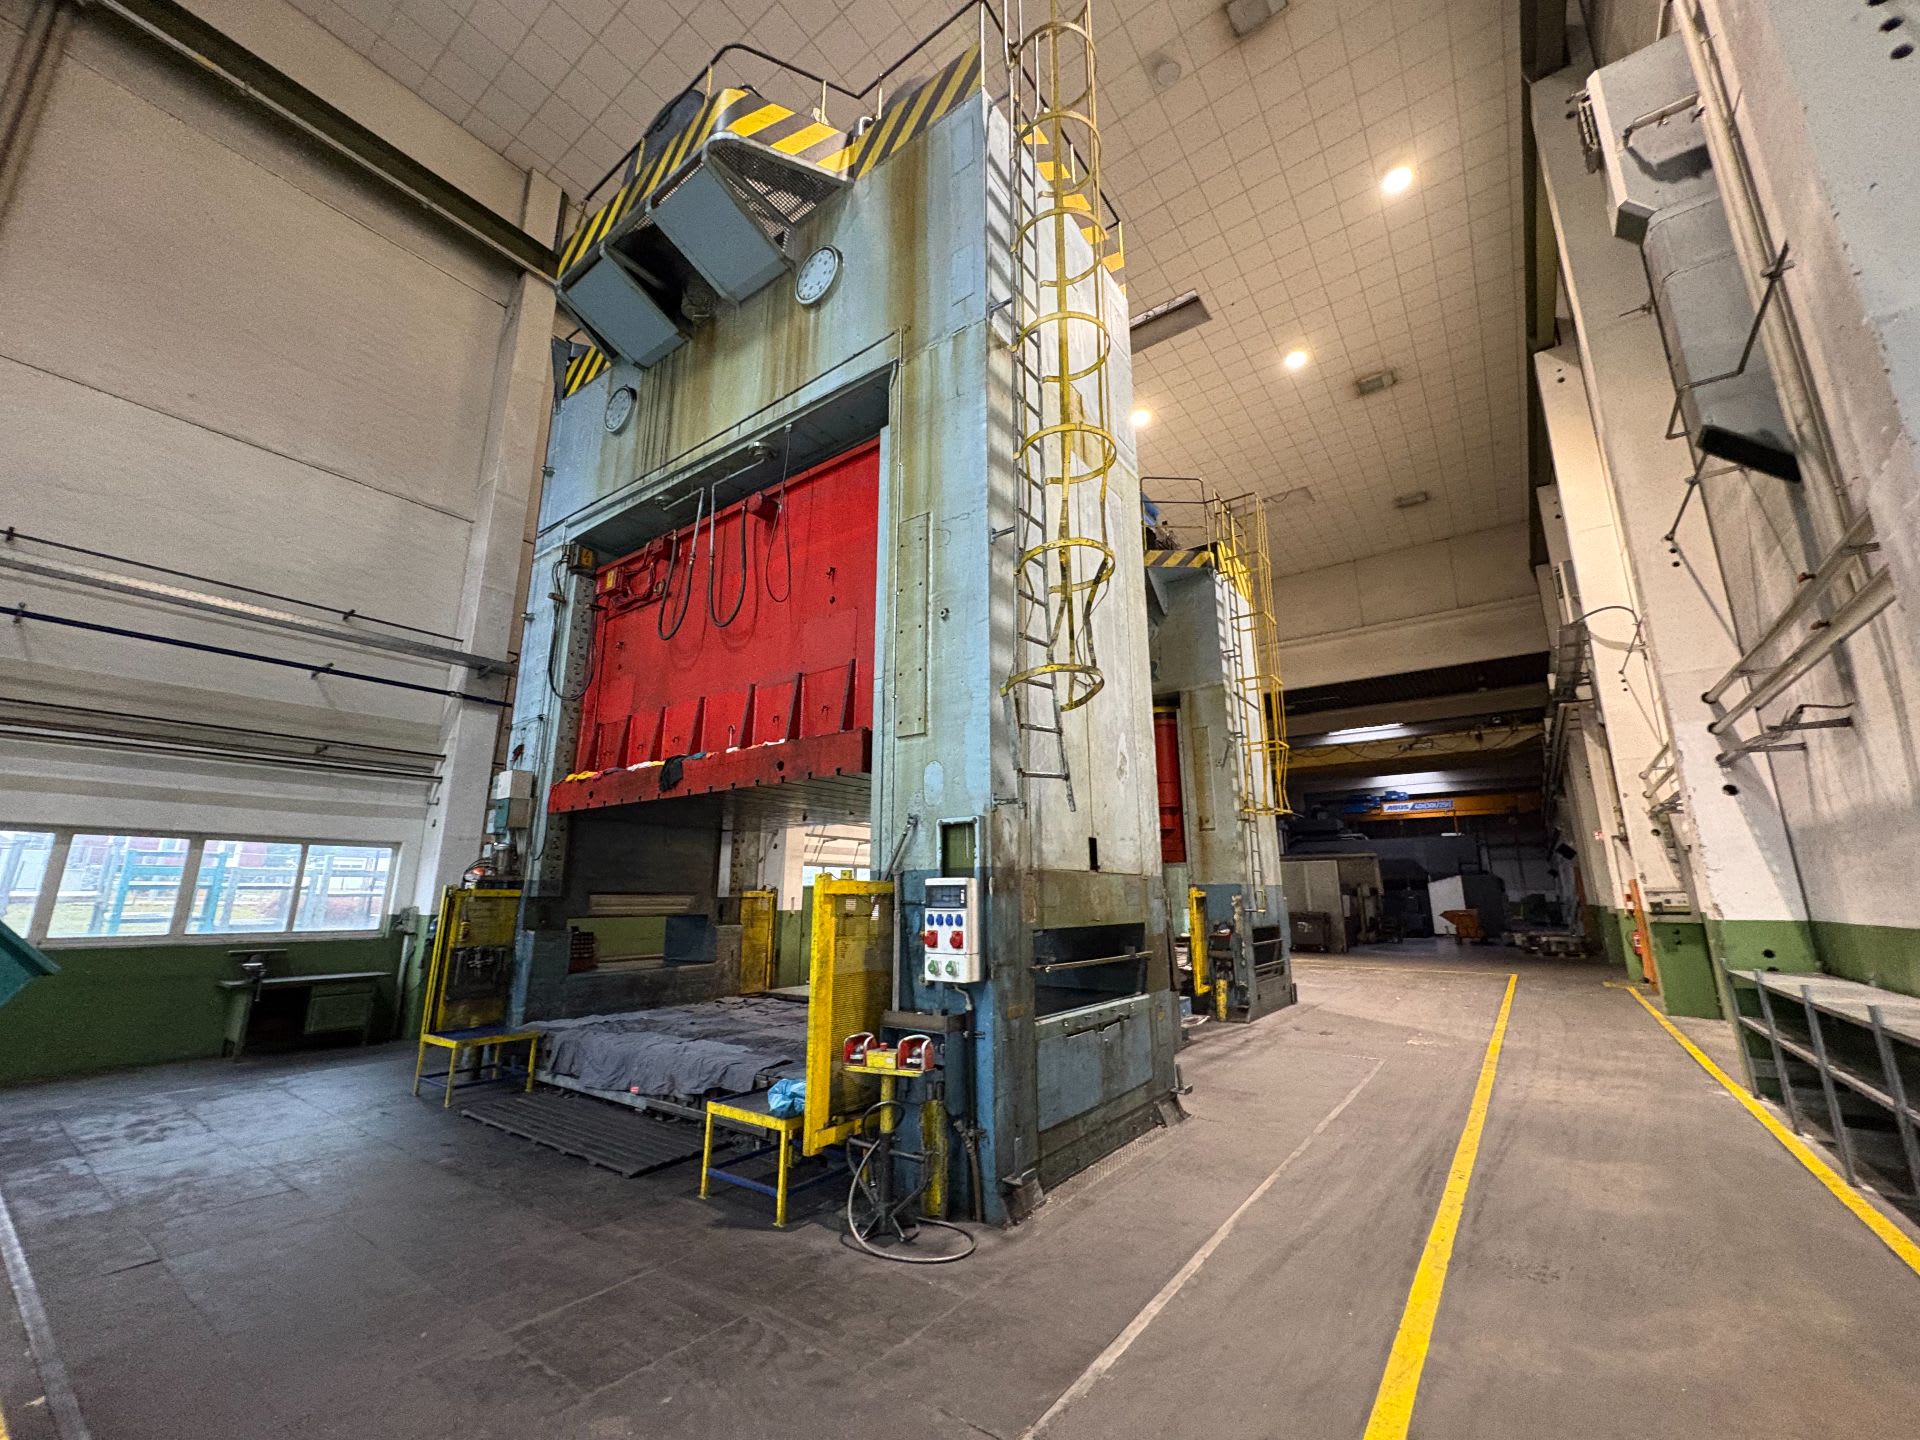
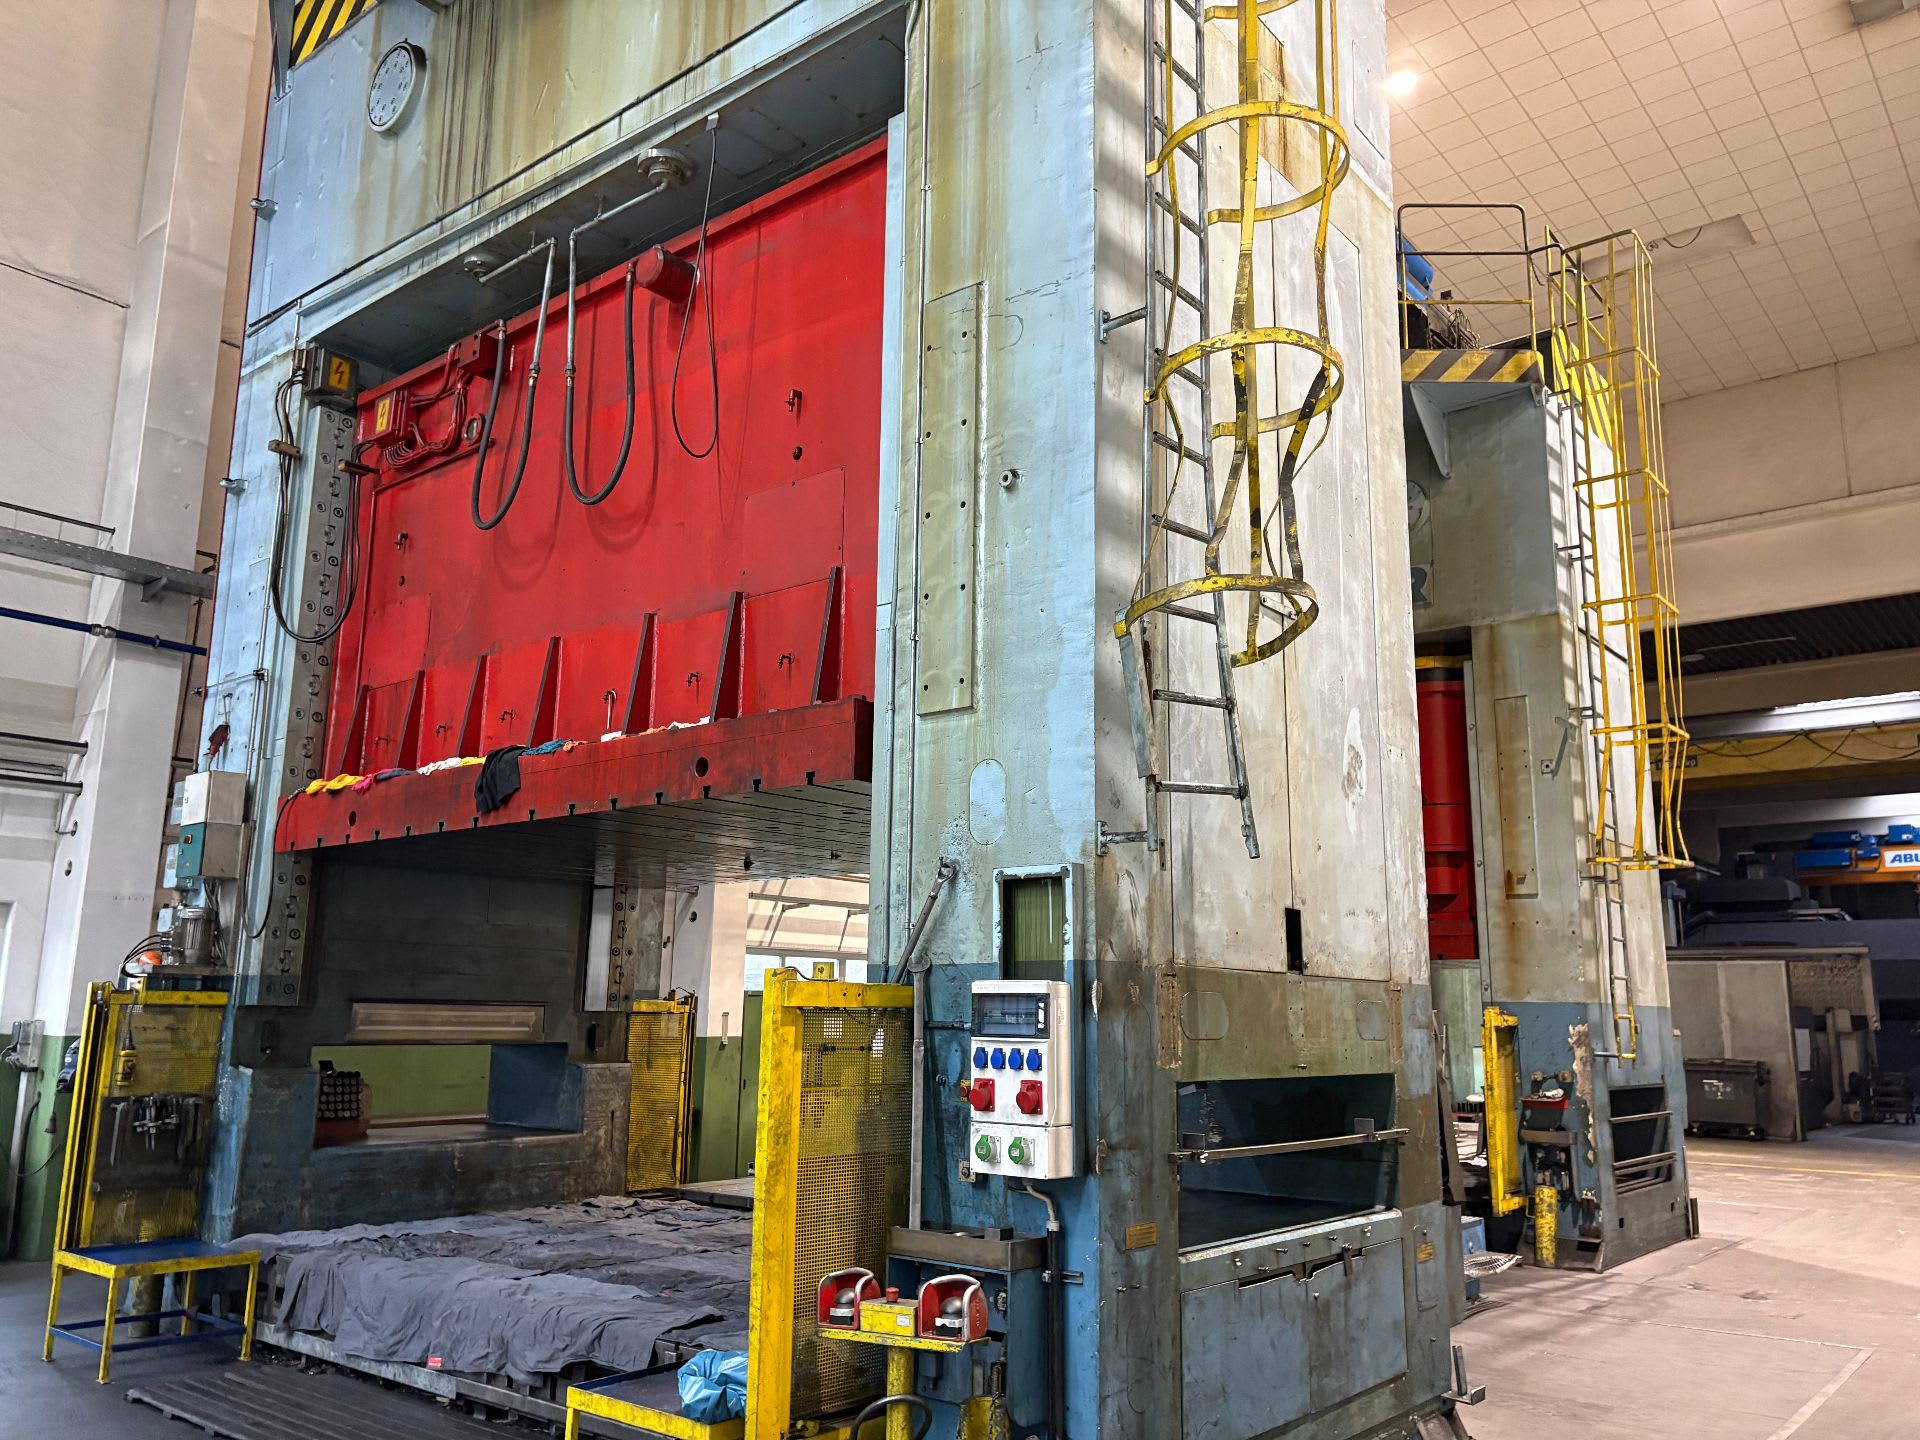
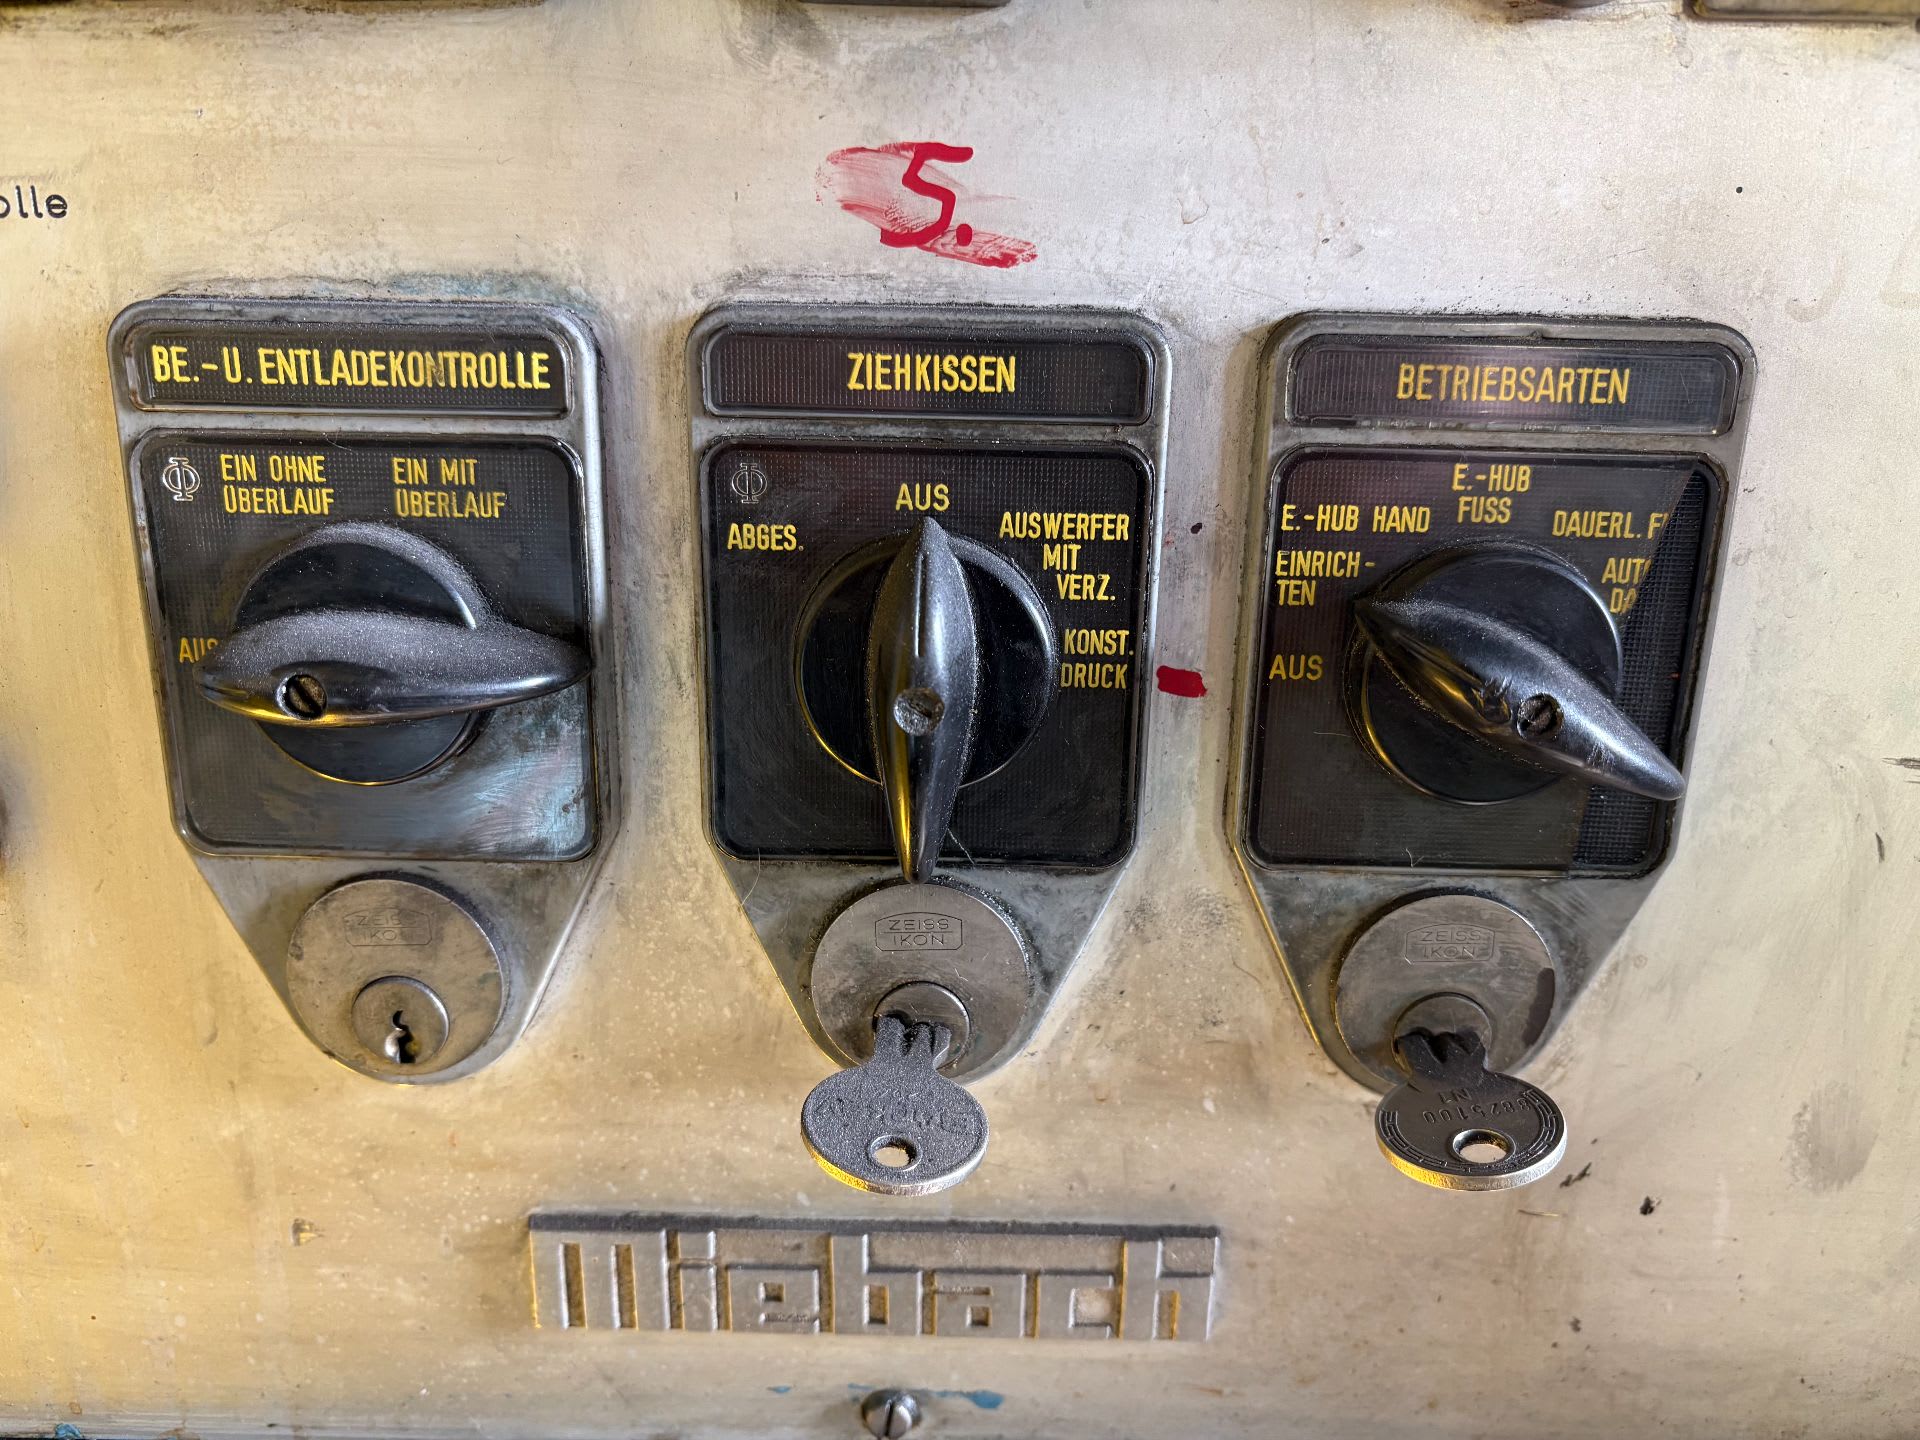
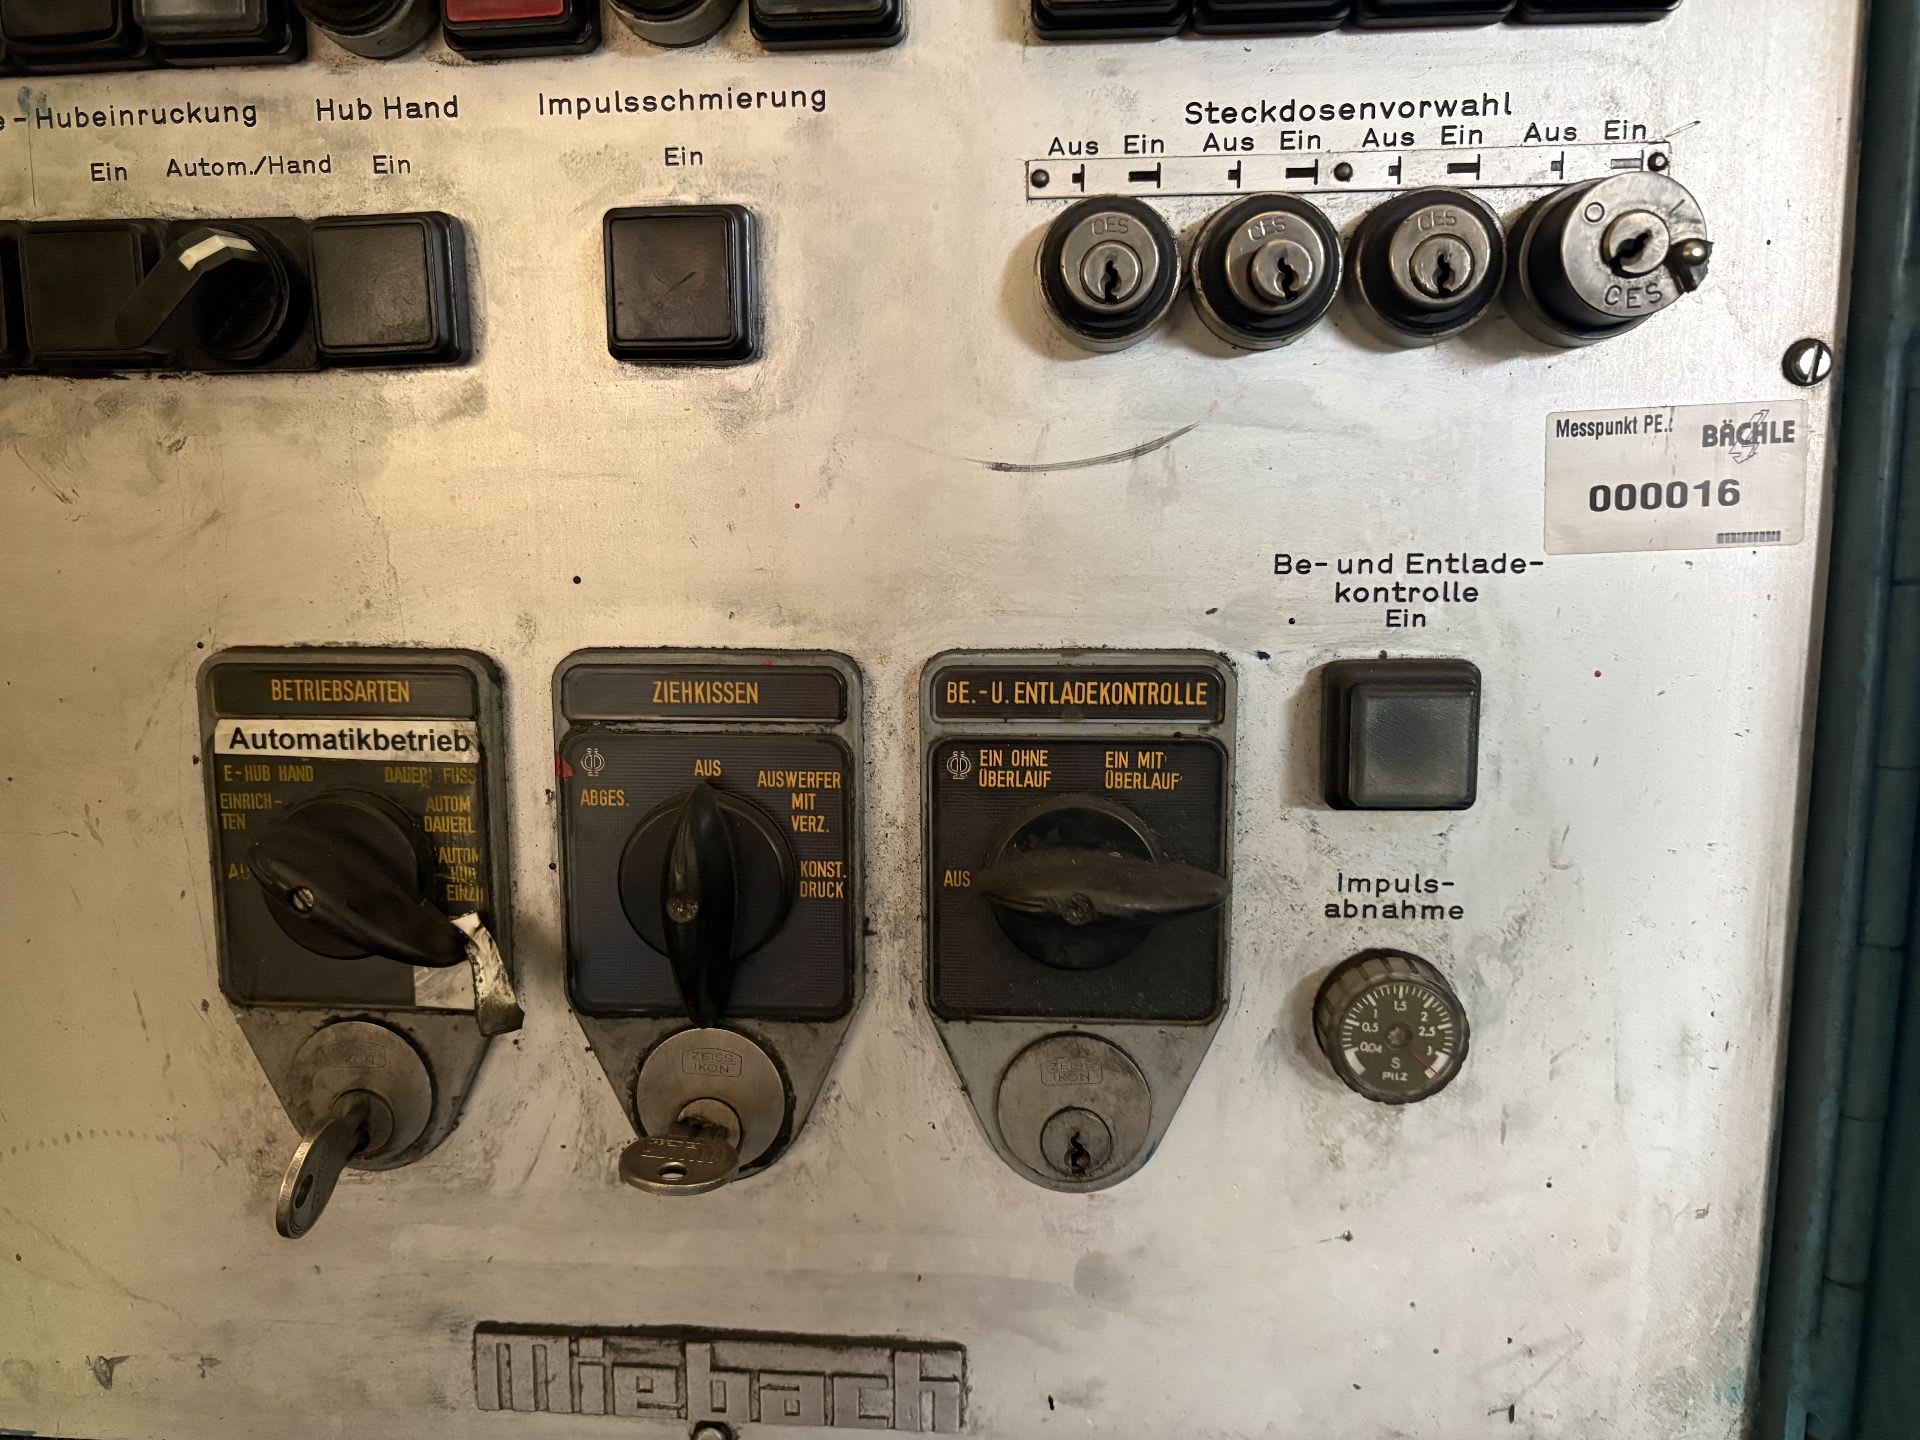
Heavy-duty mechanical eccentric drawing press in robust double-column design from Schuler, designed for continuous industrial operation in the automotive sector.
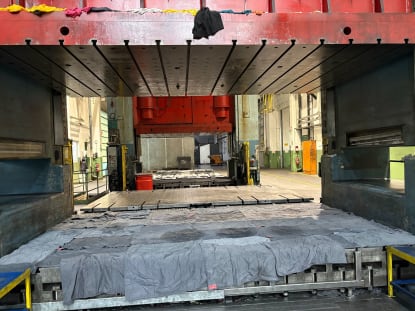
The machine features a press force of 1,200 t with a fixed ram stroke of 600 mm and an additional ram adjustment of 600 mm. The stroke rate is approx. 9 strokes per minute. The shut height is approx. 1,600 mm, allowing the processing of large-scale tools and components.
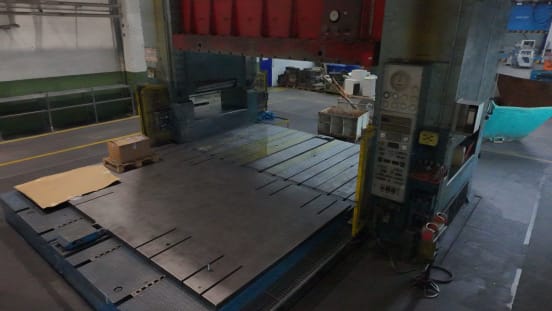
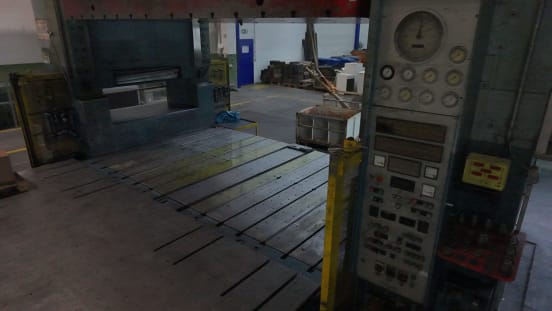
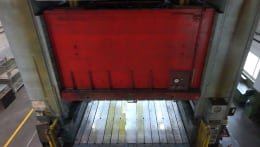
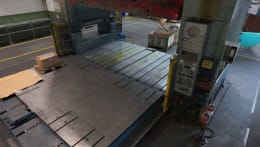
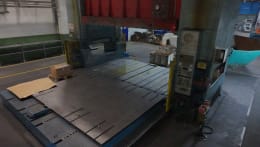
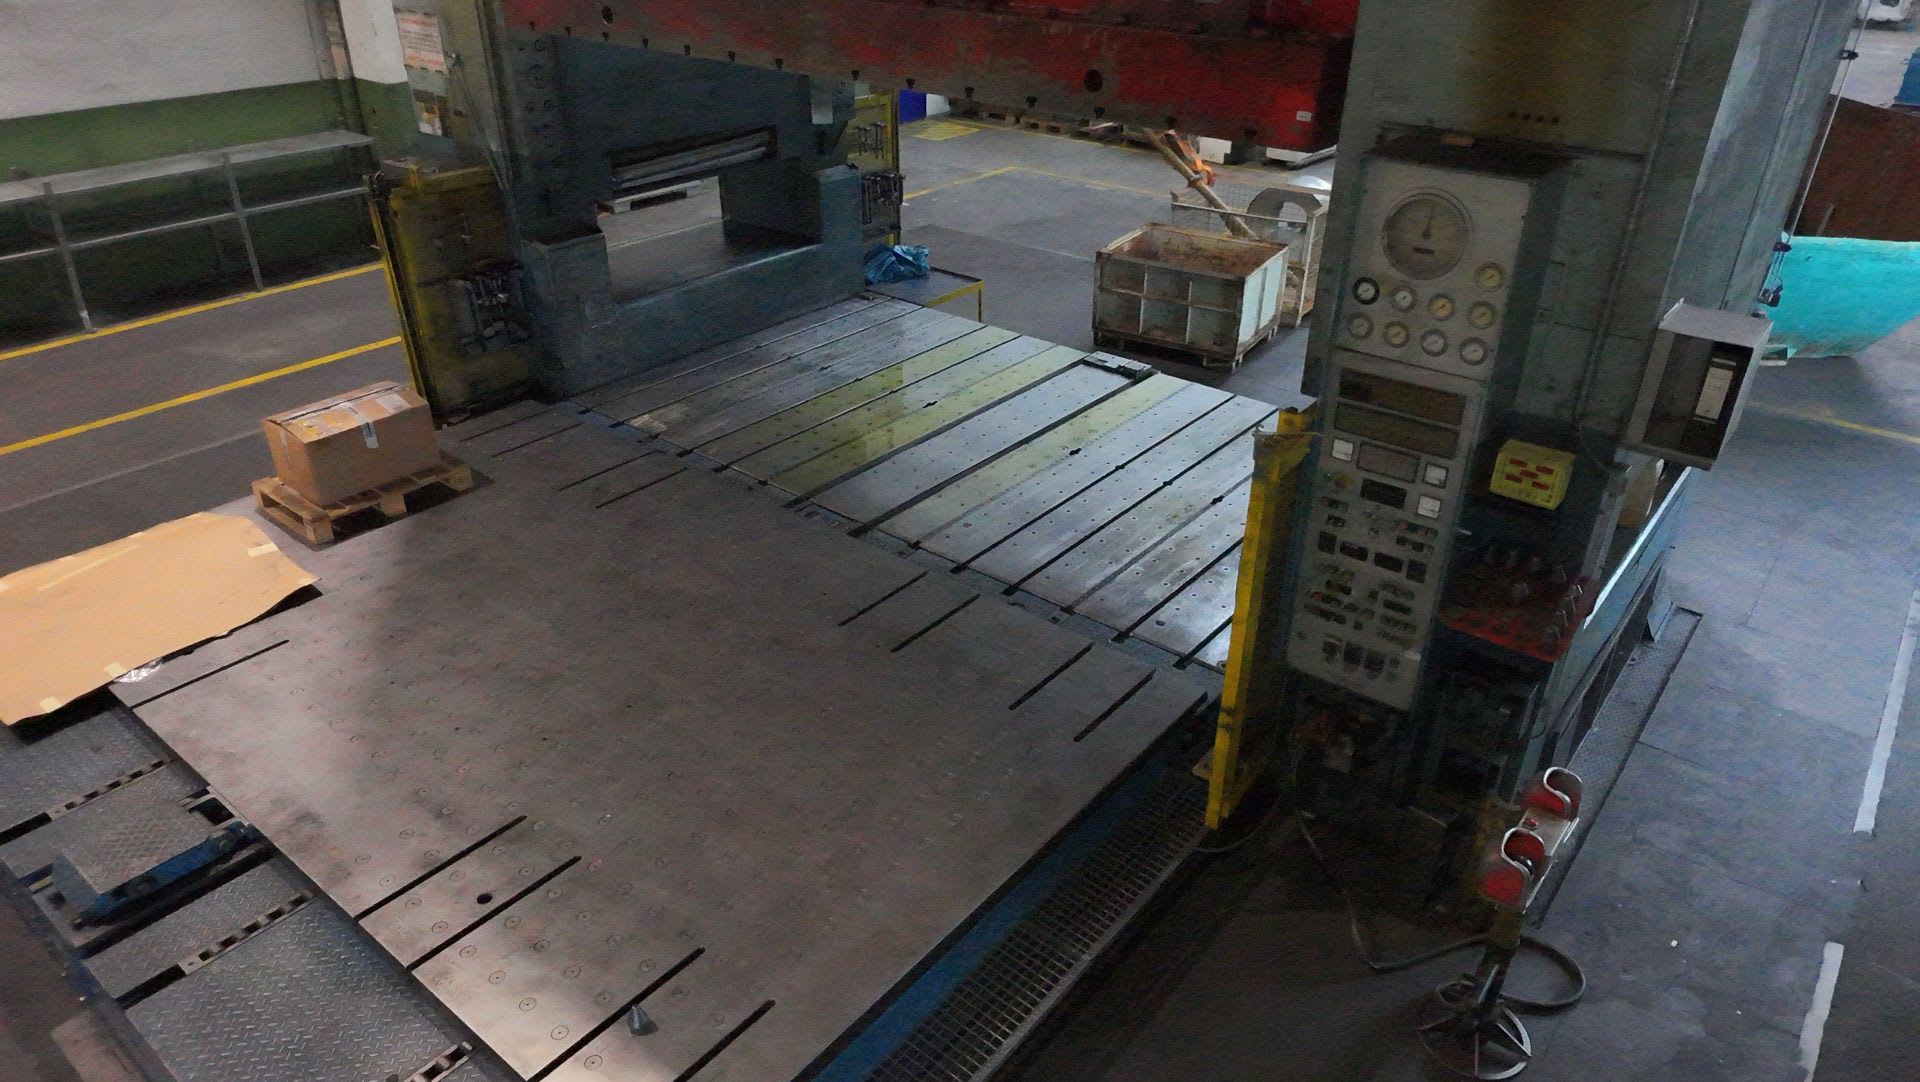
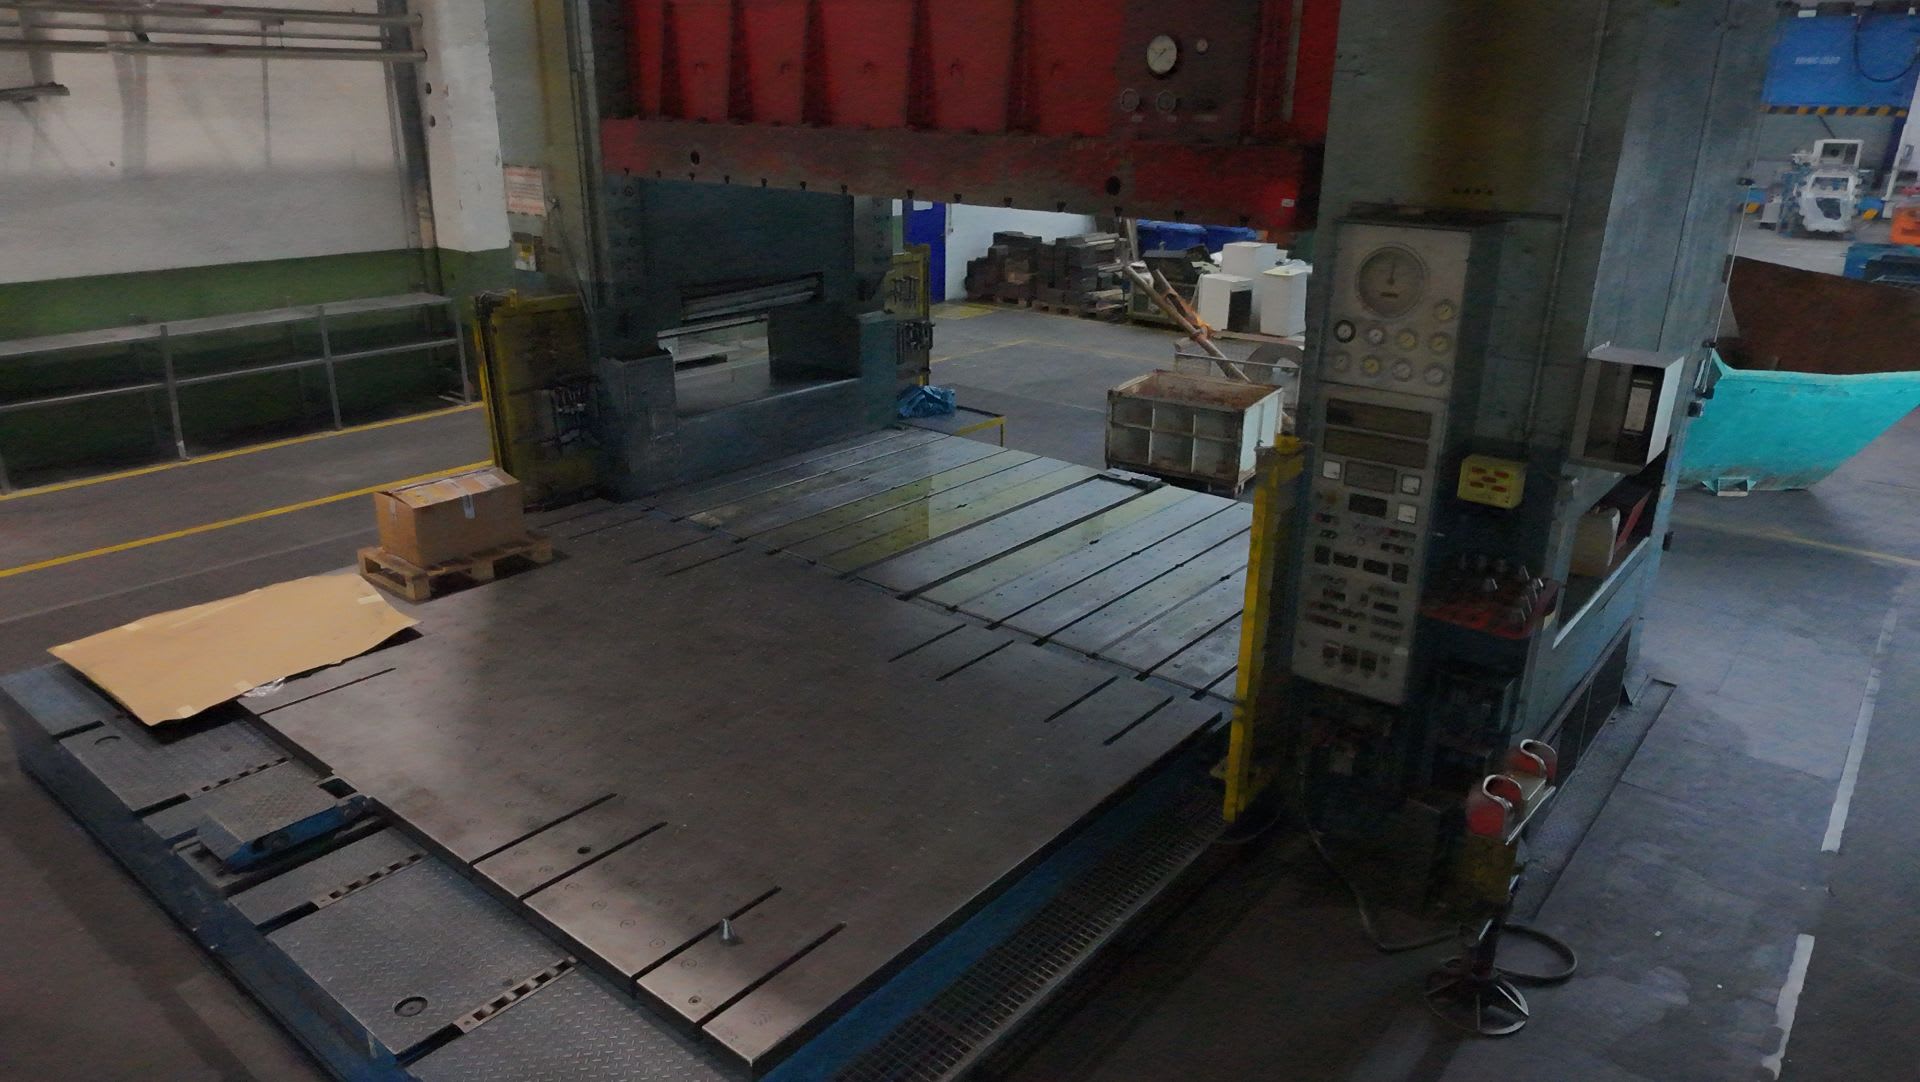
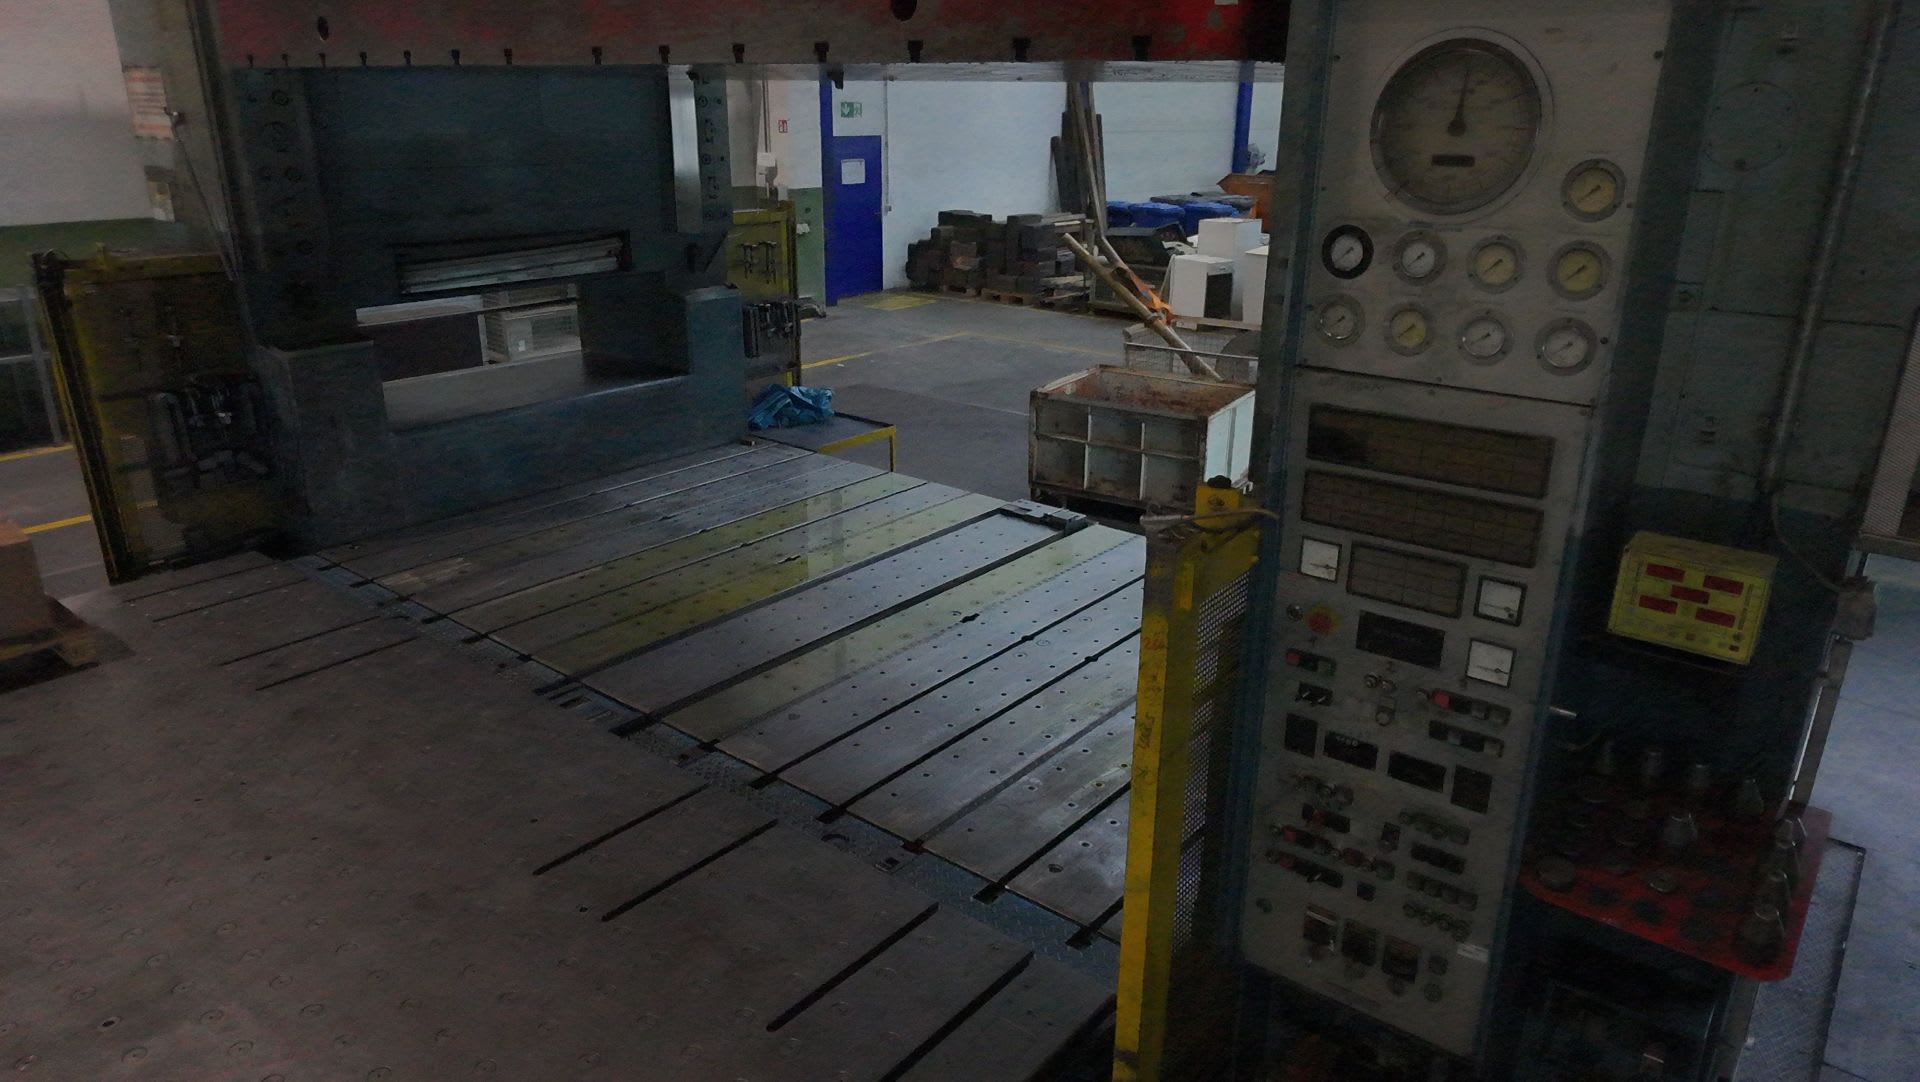
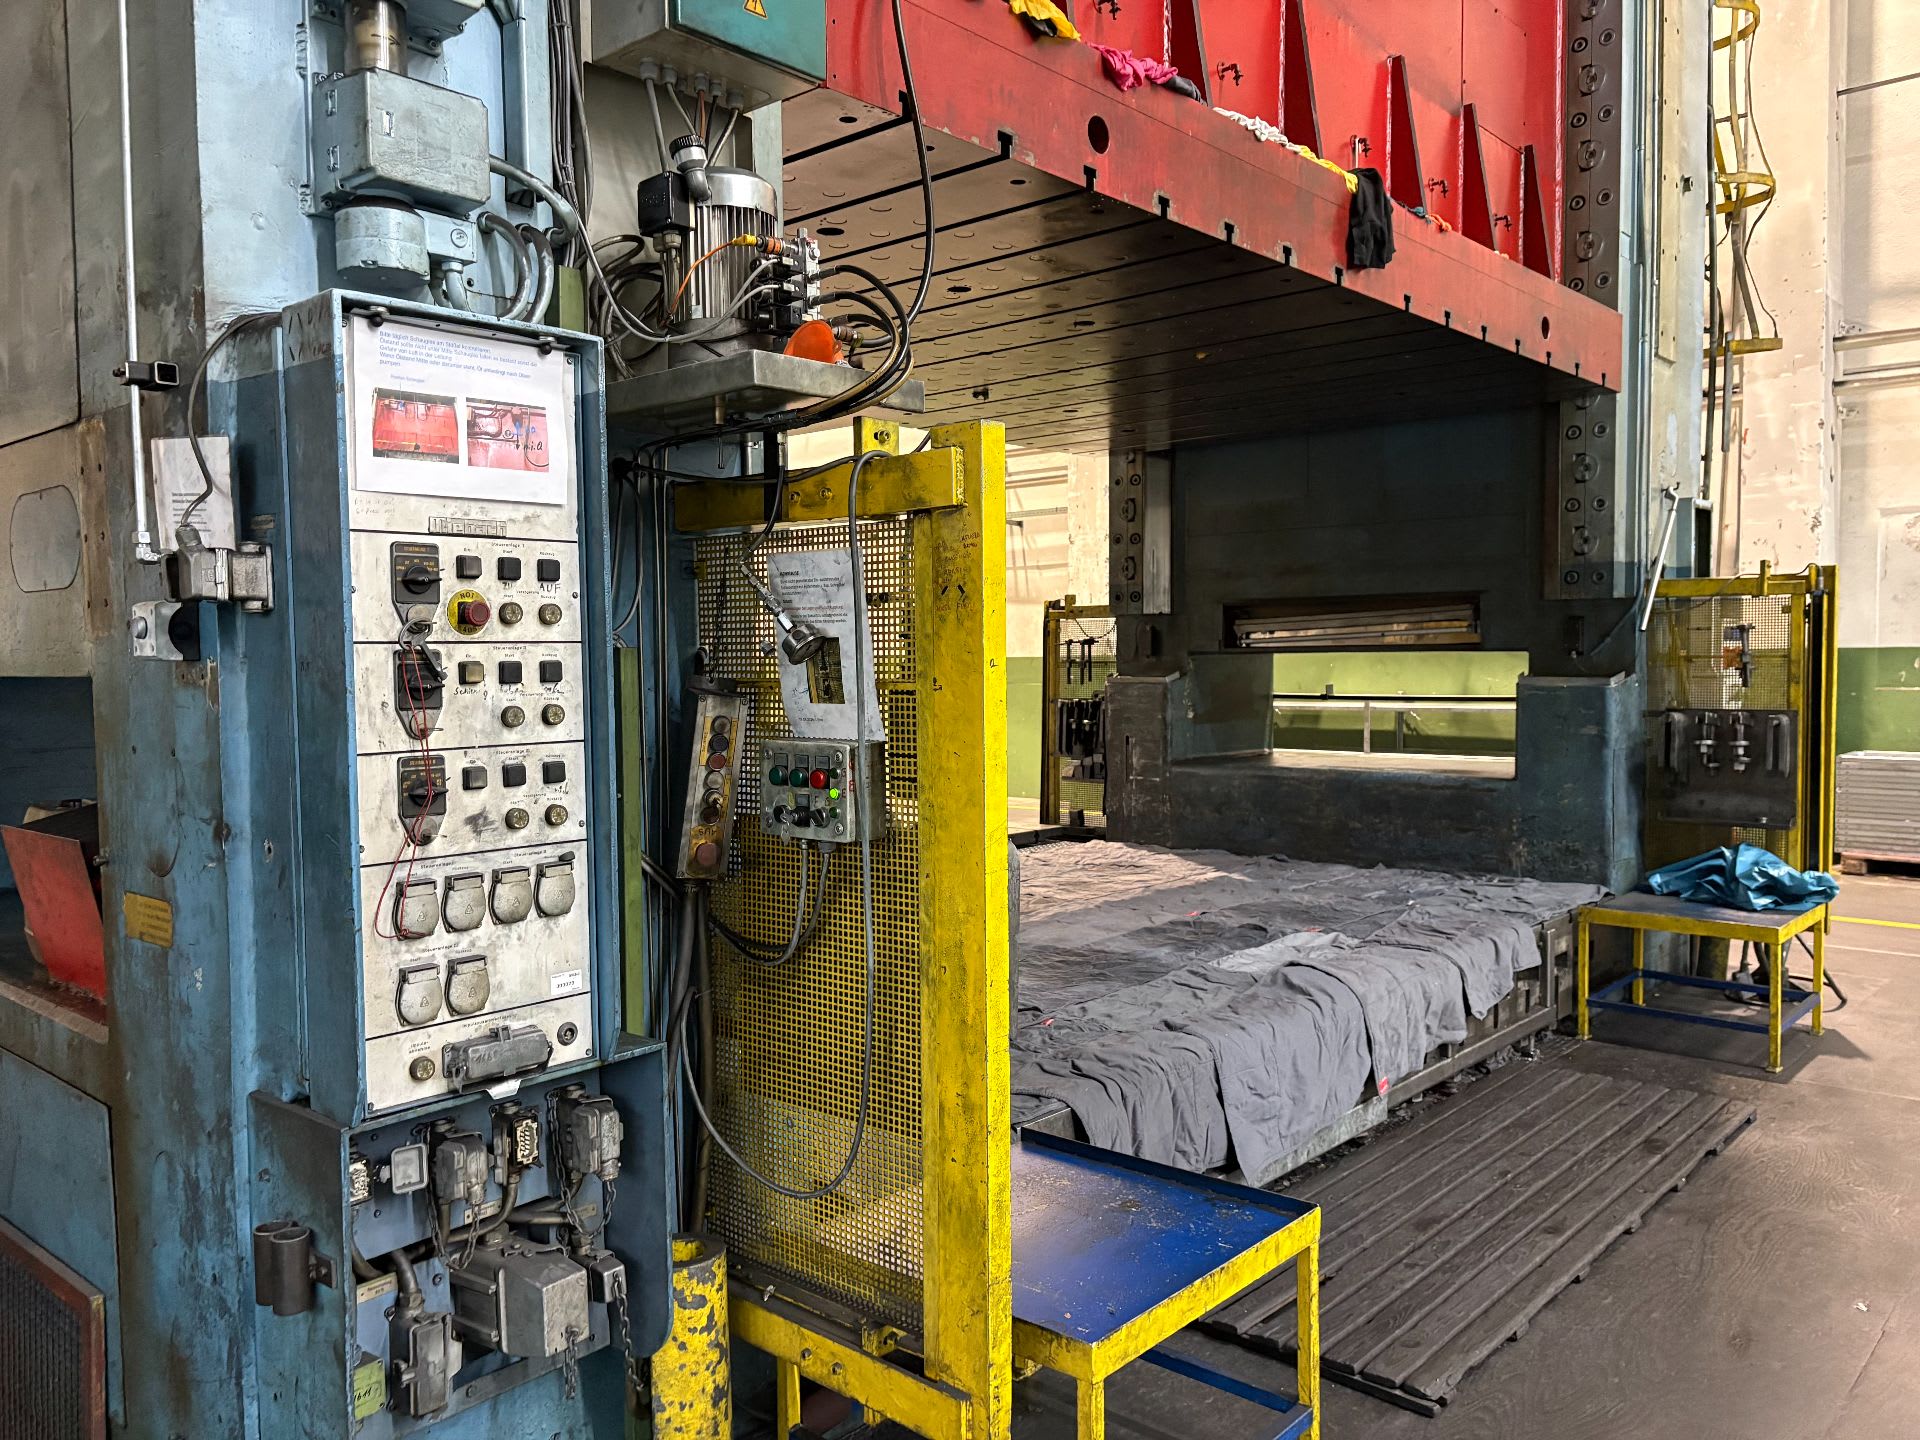
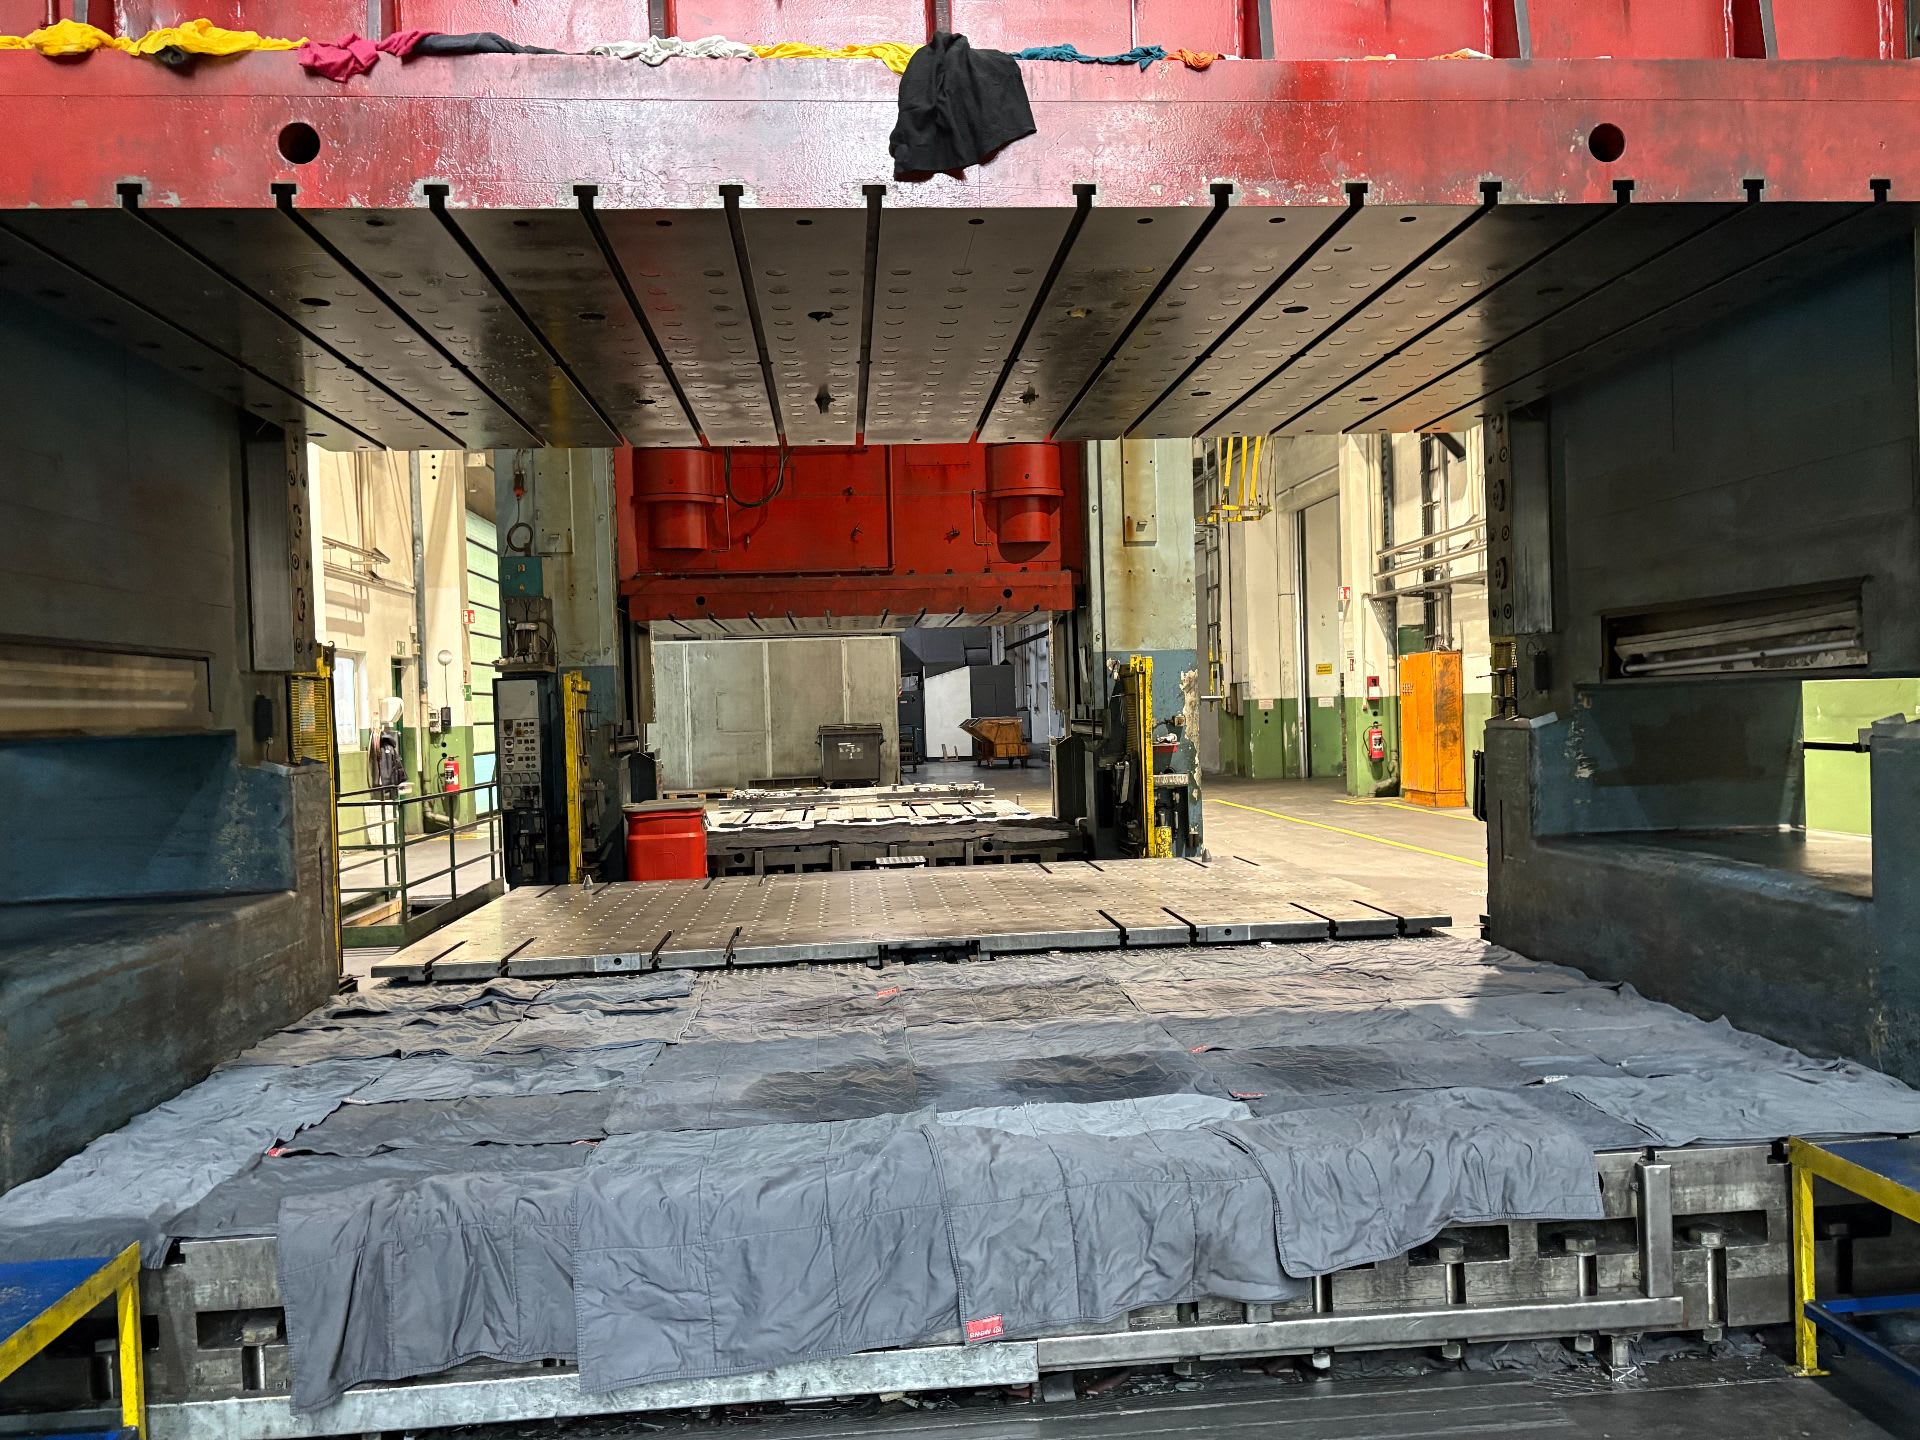
Particularly noteworthy is the large working area with a table size of approx. 4,500 mm as well as a movable / sliding press table, which significantly facilitates setup and tool change and makes the machine ideally suited for handling heavy tooling.
The integrated drawing equipment (drawing cushion) provides a force of approx. 225 t with a stroke of approx. 200 mm, enabling demanding deep drawing and forming processes, especially in automotive body production.
Additionally, the press is equipped with a pneumatic ejector in the ram (approx. 95 t / 150 mm), supporting automated part removal.
The press has not been in continuous production operation since the 1990s at its current location and has only been used for testing purposes.
- Transportation costs
- not included
- Terms of delivery
- From foundation
- Terms of payment
- 100% prepayment before pick-up
The price of a used press depends on the press type, press force, bed size, stroke, die cushion, control, year of manufacture and condition. Transportation costs are not included in the machine price; terms of delivery and payment are stated under "Additional information" in each listing. You should also budget for installation and commissioning at the new site. In most cases, the buyer is responsible for organizing the transport; upon request, ReMach can check whether transport can be arranged or supported. ReMach also helps with dismantling, loading and export paperwork.
Before restarting a used press, check all safety devices: light curtains or guards, interlocks, the emergency stop circuit and, on hydraulic presses, the safety valves. In the EU, the reference safety standard for presses is EN ISO 16092. Have an expert carry out a safety assessment before operating the press at the new site.
A press suits your die when its press force (in t or kN), bed size and die height all match the die. Also check the stroke, and a die cushion if the die is used for deep drawing. On mechanical presses, the number of strokes per minute determines output.
A workshop press has an H-frame or C-frame with manual or electric hydraulics and is used to press bearings and bushes and straighten parts in maintenance and repair. A production press has a bed and slide for mounting dies, stroke control, often a die cushion and safety systems for series production. For production use, choose by press force and die, not by force alone.
A hydraulic press uses a pump to push oil into a cylinder, and the pressing force equals oil pressure multiplied by piston area. It delivers full force over the entire stroke with adjustable stroke and speed, which makes it suitable for deep drawing, forming and die try-out. A mechanical (eccentric) press runs faster with a fixed stroke and reaches its nominal force near bottom dead centre, ideal for high-volume stamping; a try-out press is used to test and adjust dies before production.
This item is sold

Our Services
- Inspection & report
- Disassembly & installation
- Global logistics
- Customs & paperwork
- Sourcing & valuation
- Personal consultation
Related items
1. Mechanical Press: Definition, Types & Key Features
A mechanical press is a forming machine that uses mechanical means – such as levers, knuckle-joint systems, eccentrics, or spindles – to apply controlled force to a workpiece. Alternative press technologies include pneumatic presses, which use compressed air, and hydraulic presses, which rely on pressurised fluid.
Mechanical presses are well suited to embossing and light to medium forming work. Compared to hydraulic presses, they typically operate within more defined pressure ranges, making them ideal for high-speed, repetitive tasks where consistent stroke control is essential.
A standard mechanical press consists of four core components: a rigid frame, a lifting mechanism, a pressing tool, and a power source. Together, these elements determine the machine's capacity, precision, and suitability for a given application.
2. Mechanical Press Applications and Pressure Capabilities
Mechanical presses, compared to hydraulic presses, operate within more restricted pressure ranges. They are well suited to embossing and light-to-medium forming work. Manual mechanical presses, operated by hand via levers, are designed for light-duty applications such as cartridge filling. Eccentric, knuckle-joint and spindle presses are often electronically controlled and capable of handling medium pressure levels of up to 5,000 kN.
3. Mechanical Press Structure: Components & How They Work
Mechanical presses consist of four core components: a frame, a lifting mechanism, a pressing tool, and a power source. While lever presses are operated manually, many modern units are electrically driven – each design optimised for specific industrial applications.
On a spindle press, a continuously rotating flywheel drives an eccentric connecting rod via a clutch. This rod moves up and down to actuate the tool and initiate the pressing process. A knuckle-joint press, by contrast, compresses the workpiece through a toggle mechanism, while a spindle press generates pressure through the vertical movement of a rotating spindle.
The pressing tool is widely regarded as the most critical component of any press. As a highly precise, custom-manufactured part, it directly determines the quality and accuracy of the finished workpiece.
With electrical drive systems, mechanical presses can achieve exceptionally high cycle rates. This is particularly true of the knuckle-joint press, which is well suited to high-speed stamping of small components. To maximise throughput and efficiency in such applications, automated feeding and assembly systems are typically integrated into the production line.
4. Mechanical Presses: How They Work & Key Manufacturers
Although manually operated presses remain common in many workshops, mechanical presses with high cycle rates are increasingly the preferred choice in modern production environments. Their ability to support automated feeding systems makes them well suited to high-volume manufacturing lines.
While manual presses continue to serve a role in the machine inventory of many production companies, demand is steadily shifting toward automated solutions that improve throughput and consistency.
Among the most respected manufacturers of mechanical presses are FRECH, MAWI, KRUPP, WEINGARTEN, and SIEMPELKAMP – all known for producing reliable, high-performance equipment across a range of industrial applications.