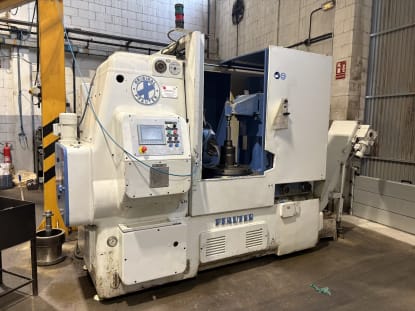
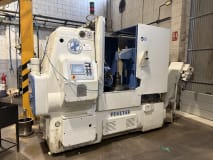
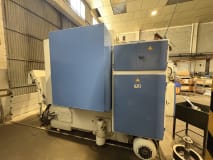
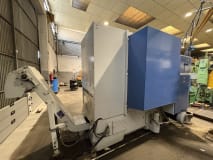
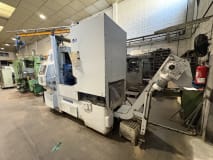
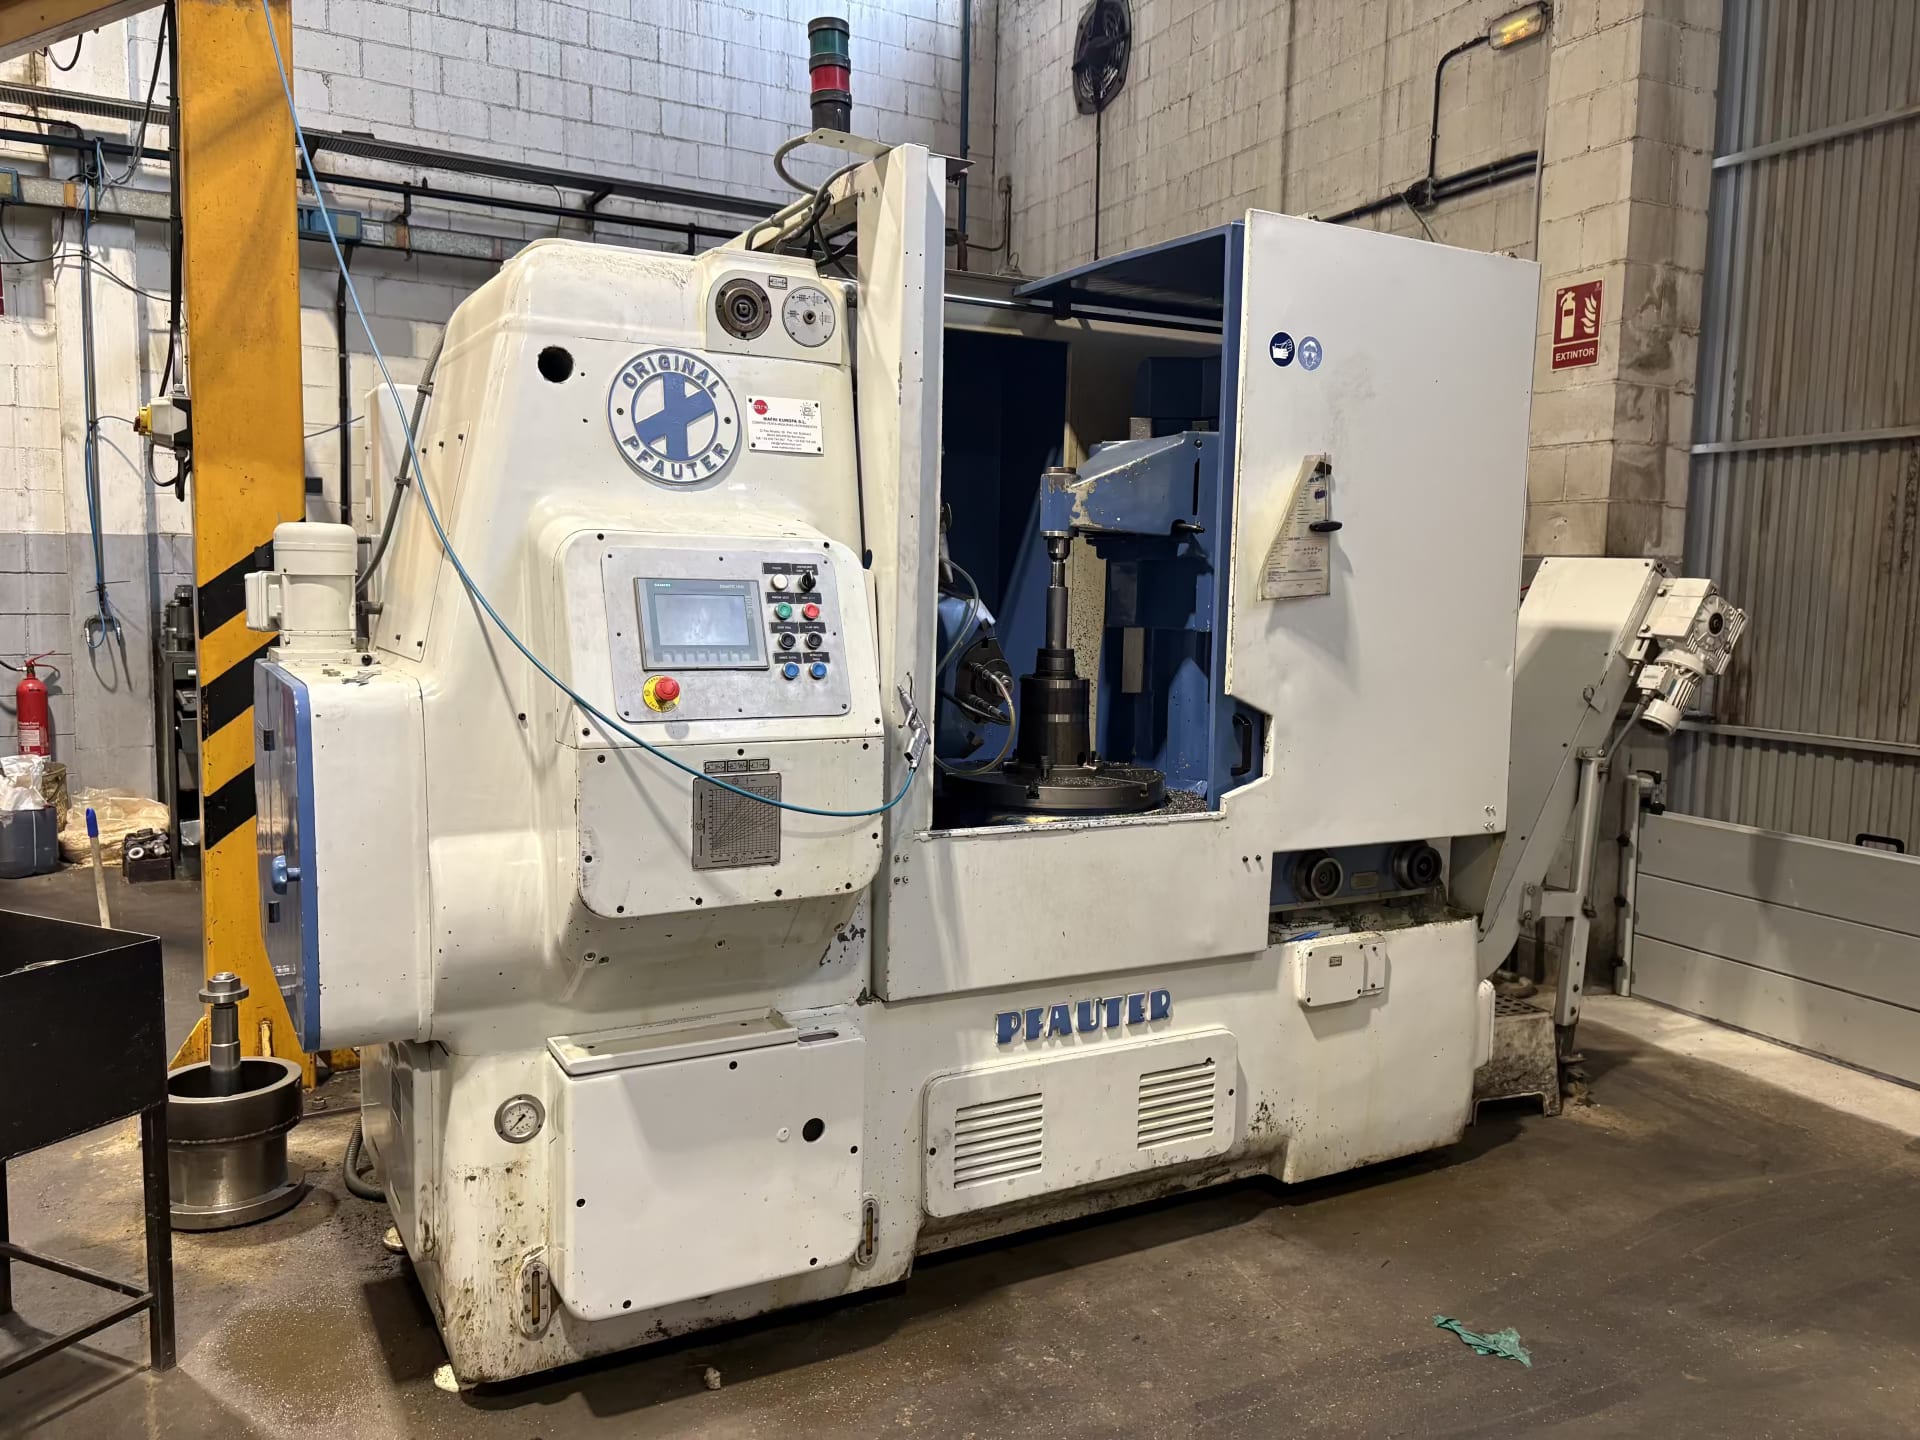
PFAUTER P630 Gear Hobbing Machine - vertical
- Storage Number
- 26022-1642
- Machine type
- Hobbing Machines
- Manufacturer
- PFAUTER
- Type
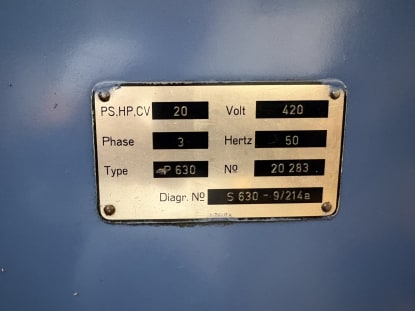
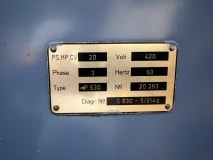
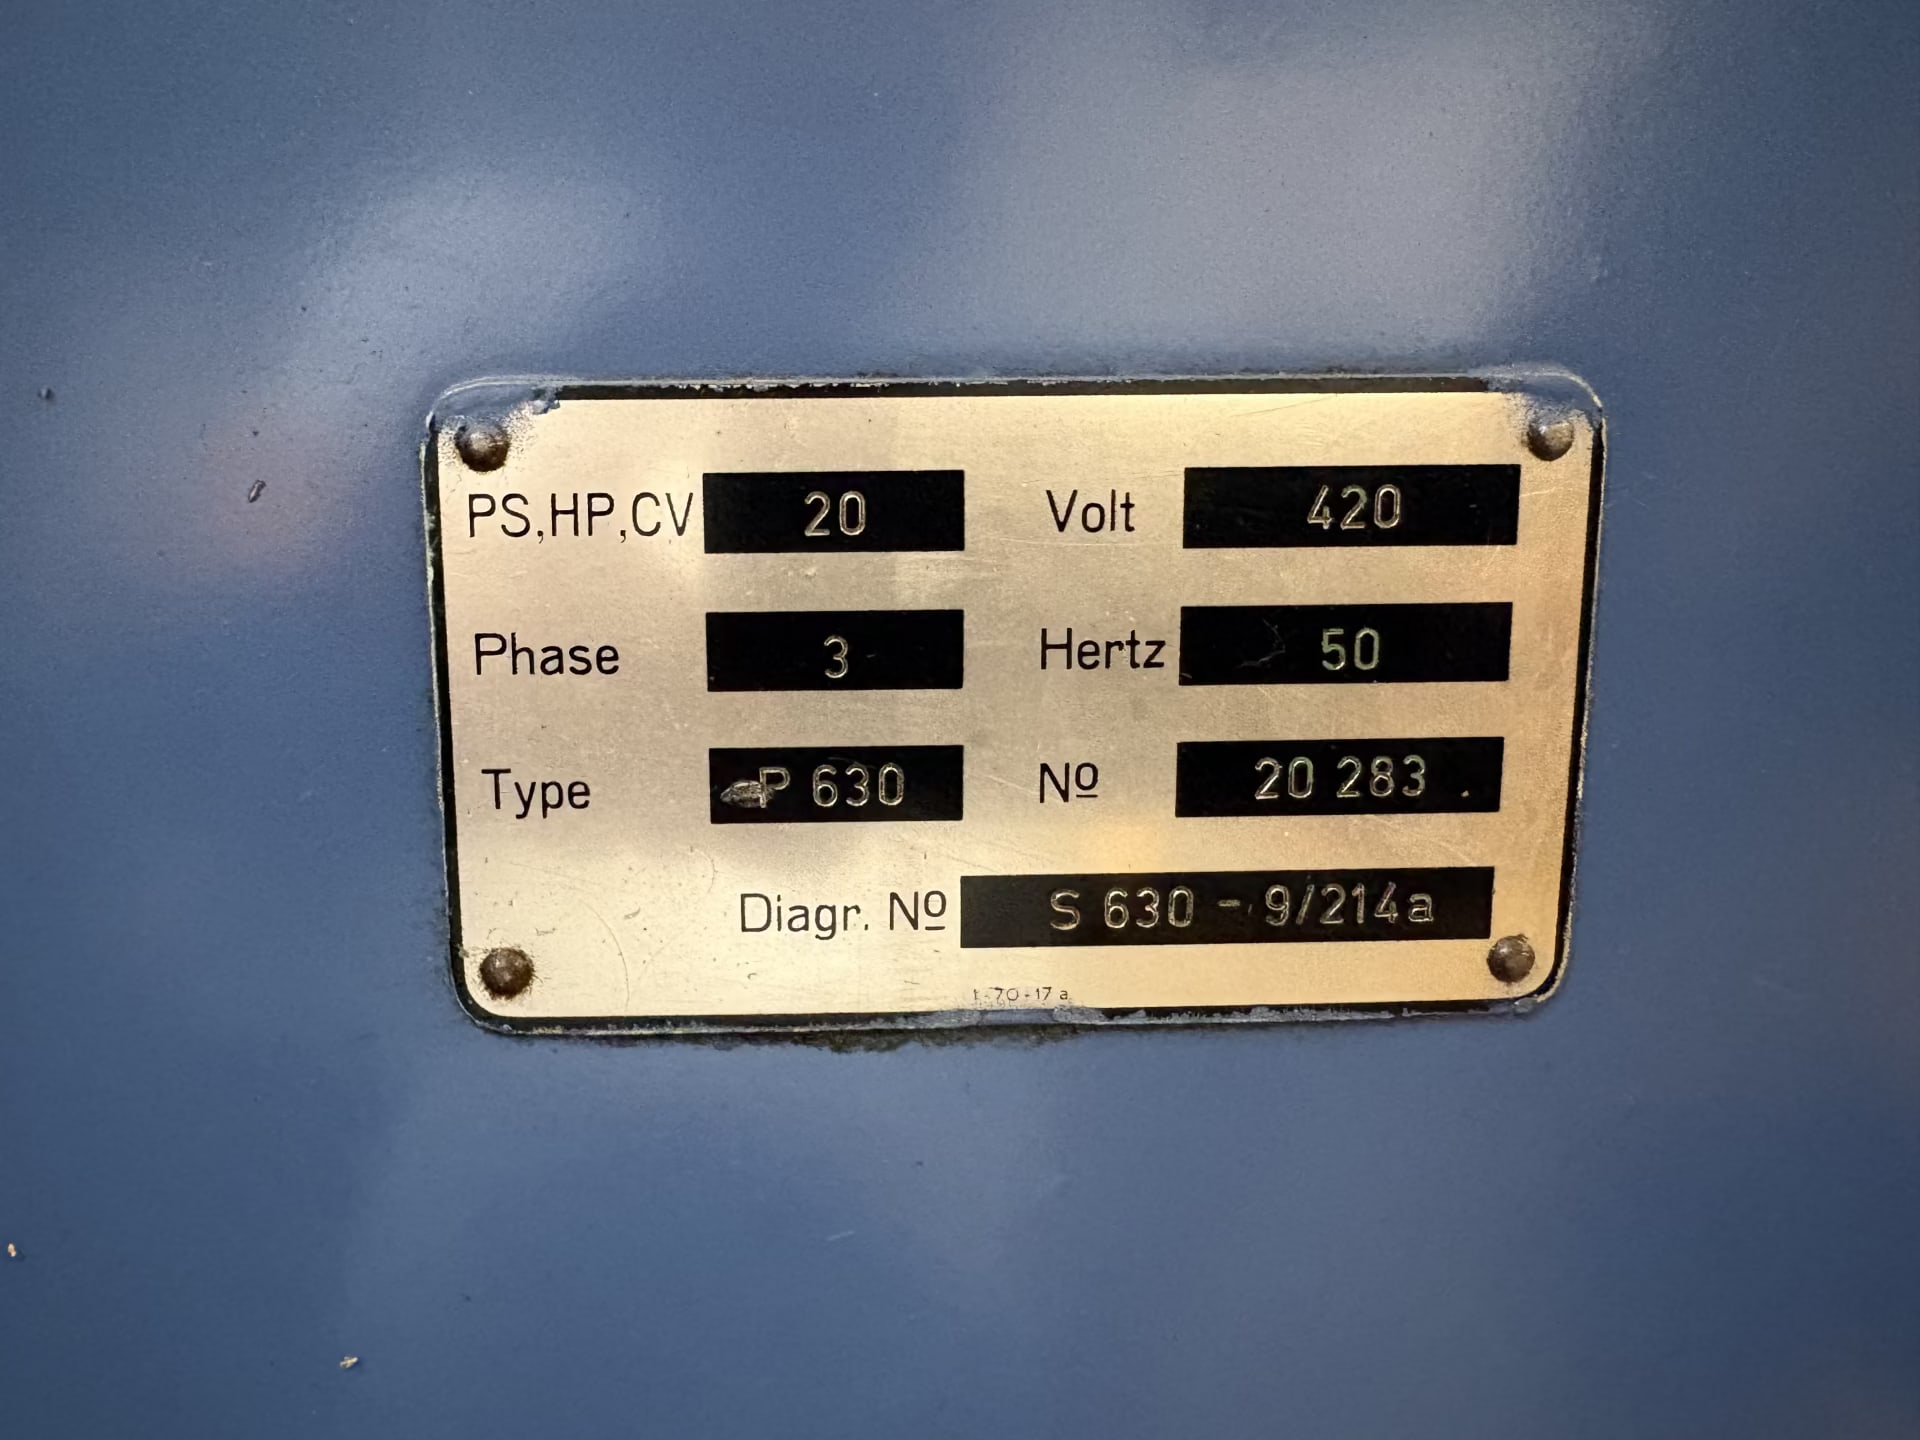
- P630
- Location
- Barcelona, Spain
- Price
- On Request
- Dimensions (LxWxH) approx.
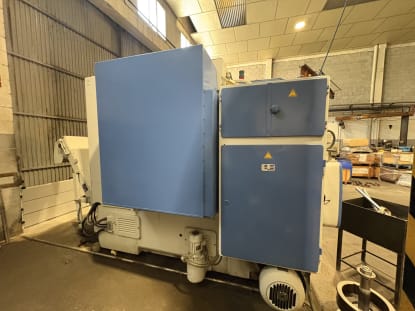
- 3000 x 2000 x 2200 mm
- Weight approx.
- 8,000 kg
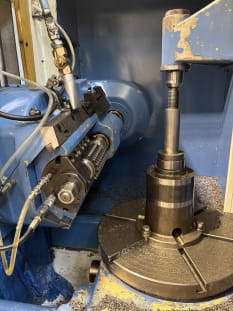
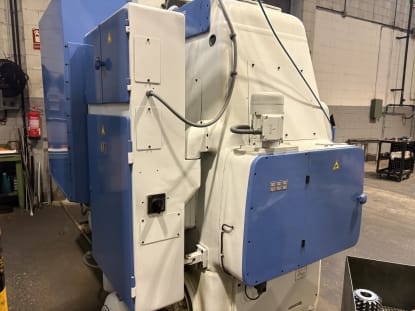
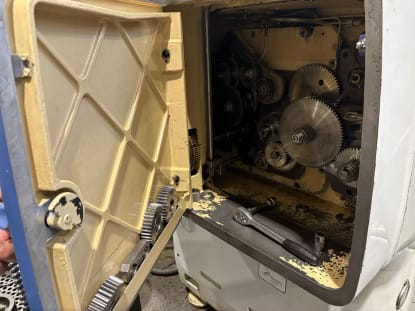
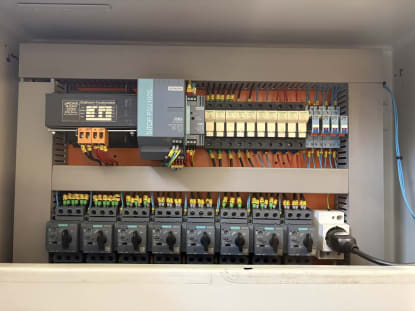
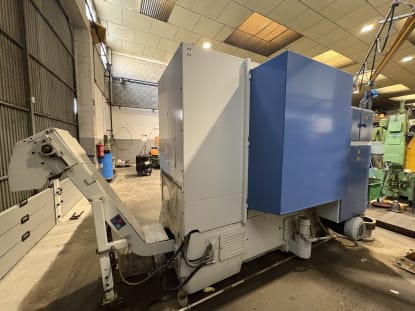
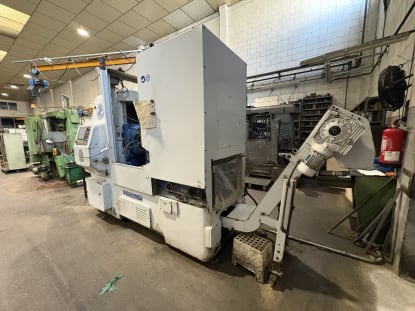
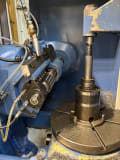
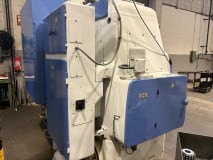
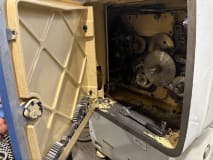
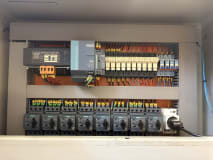
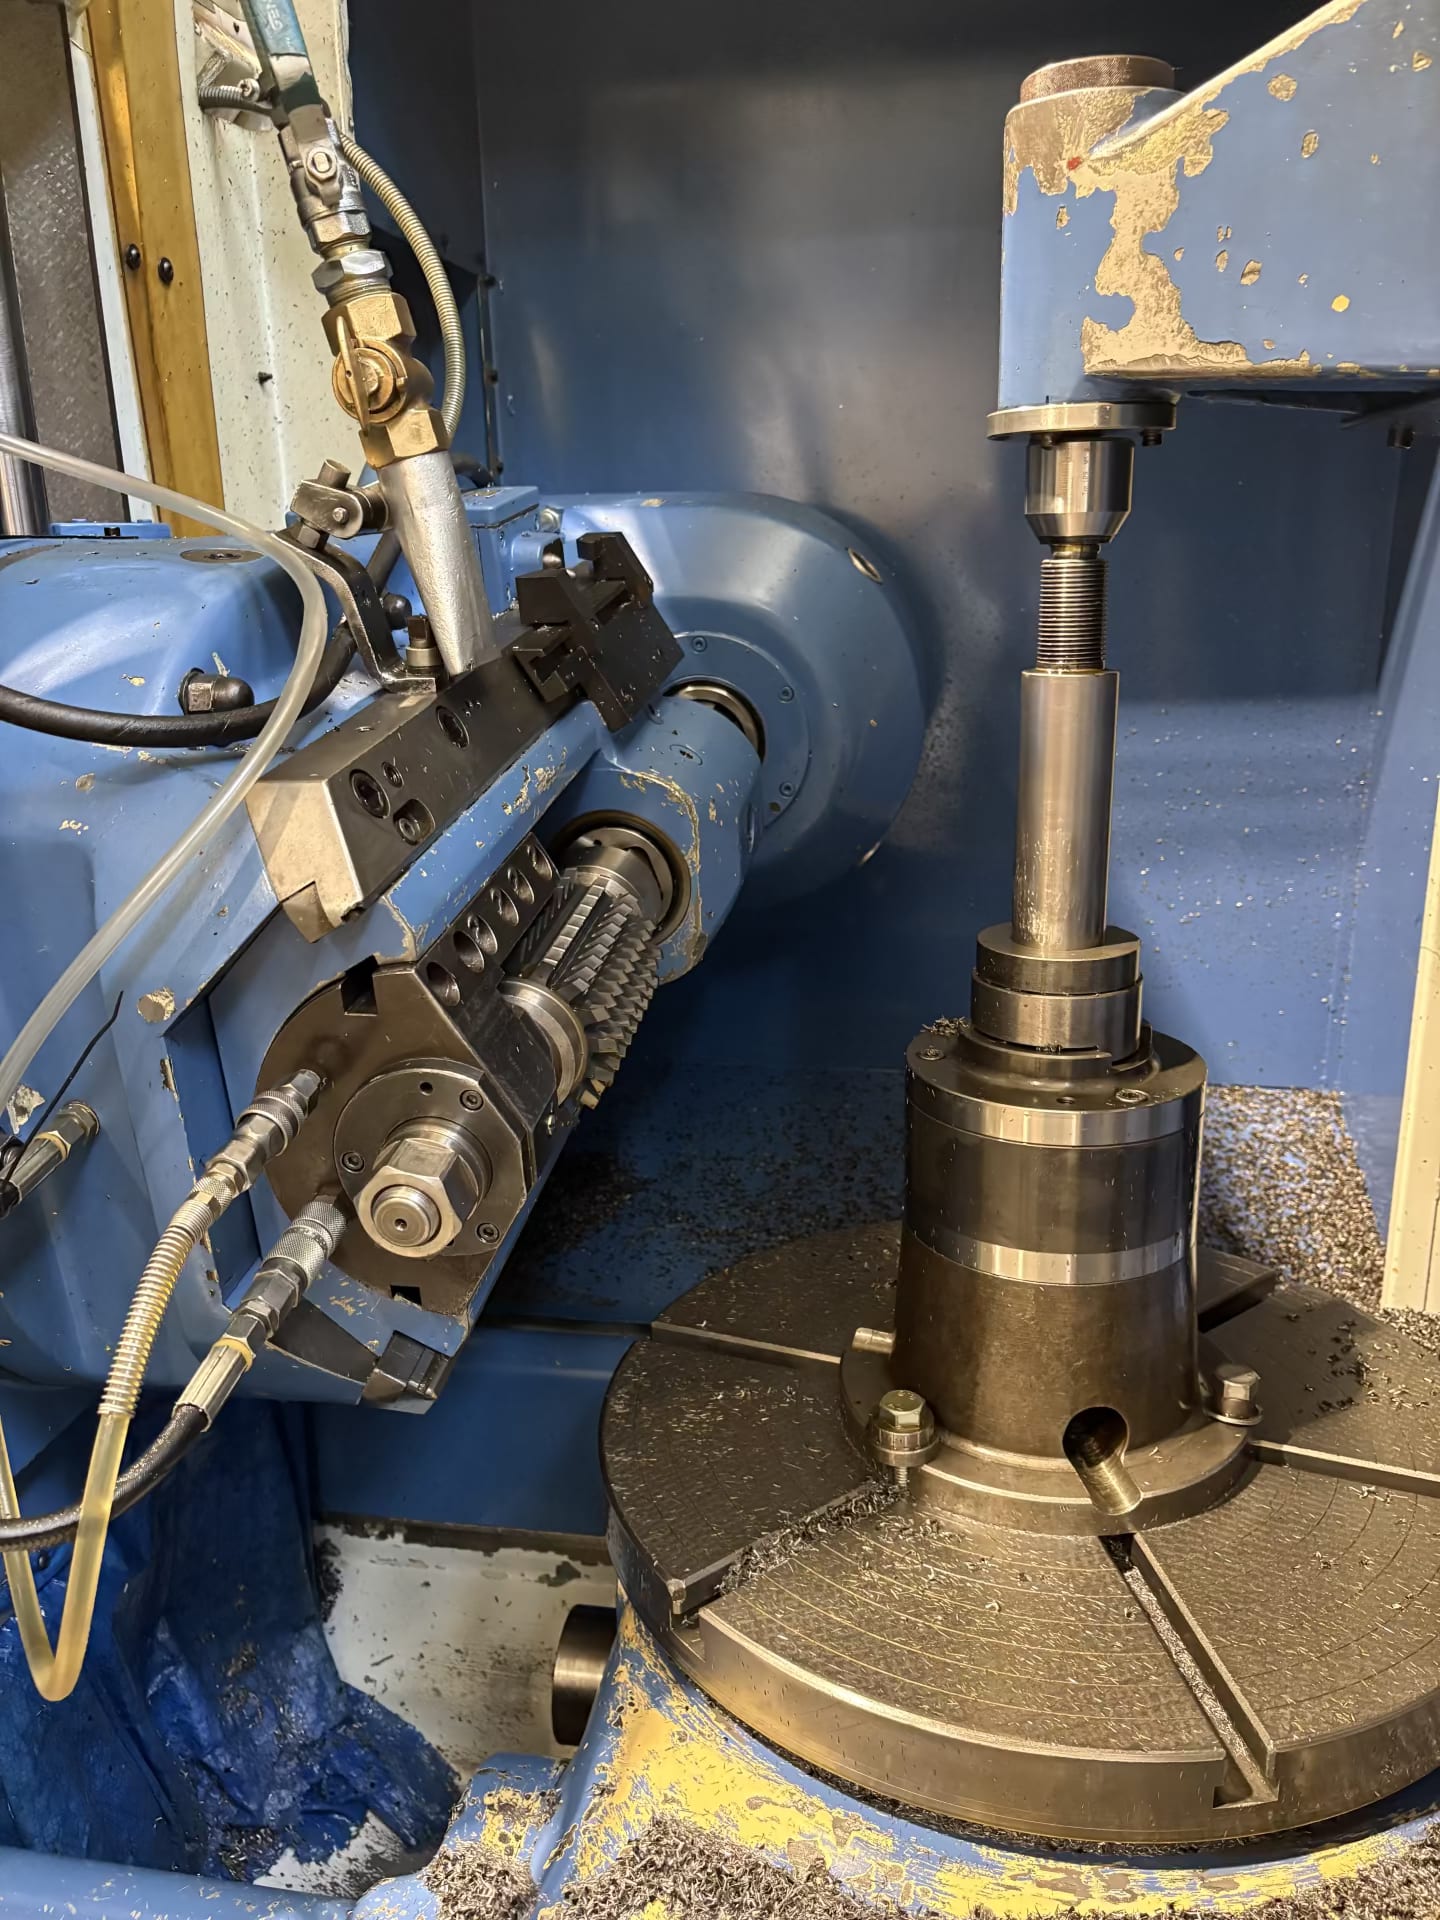
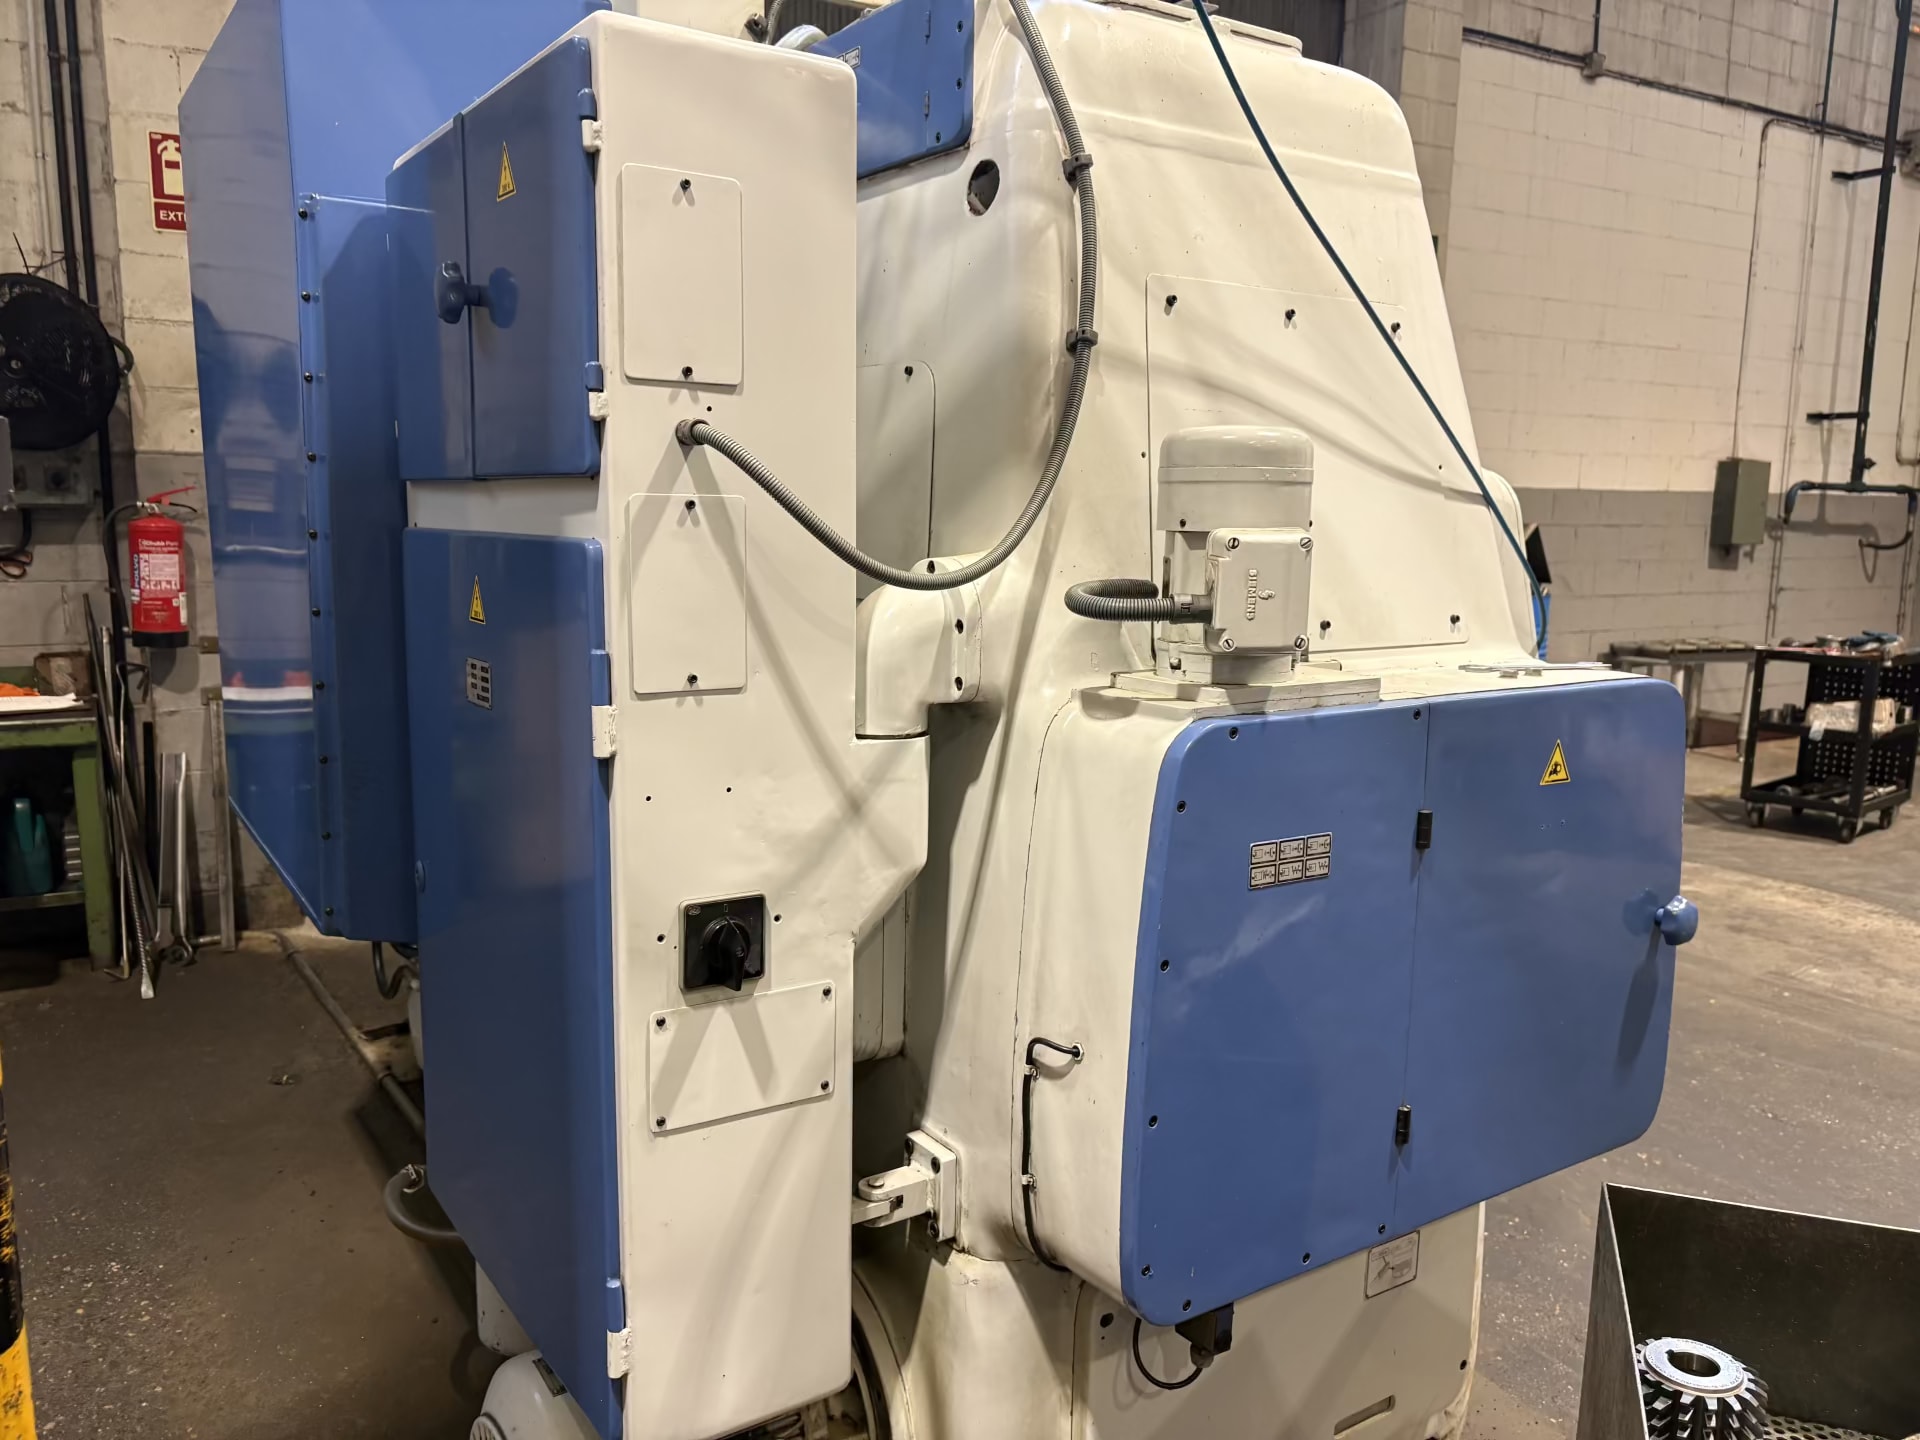
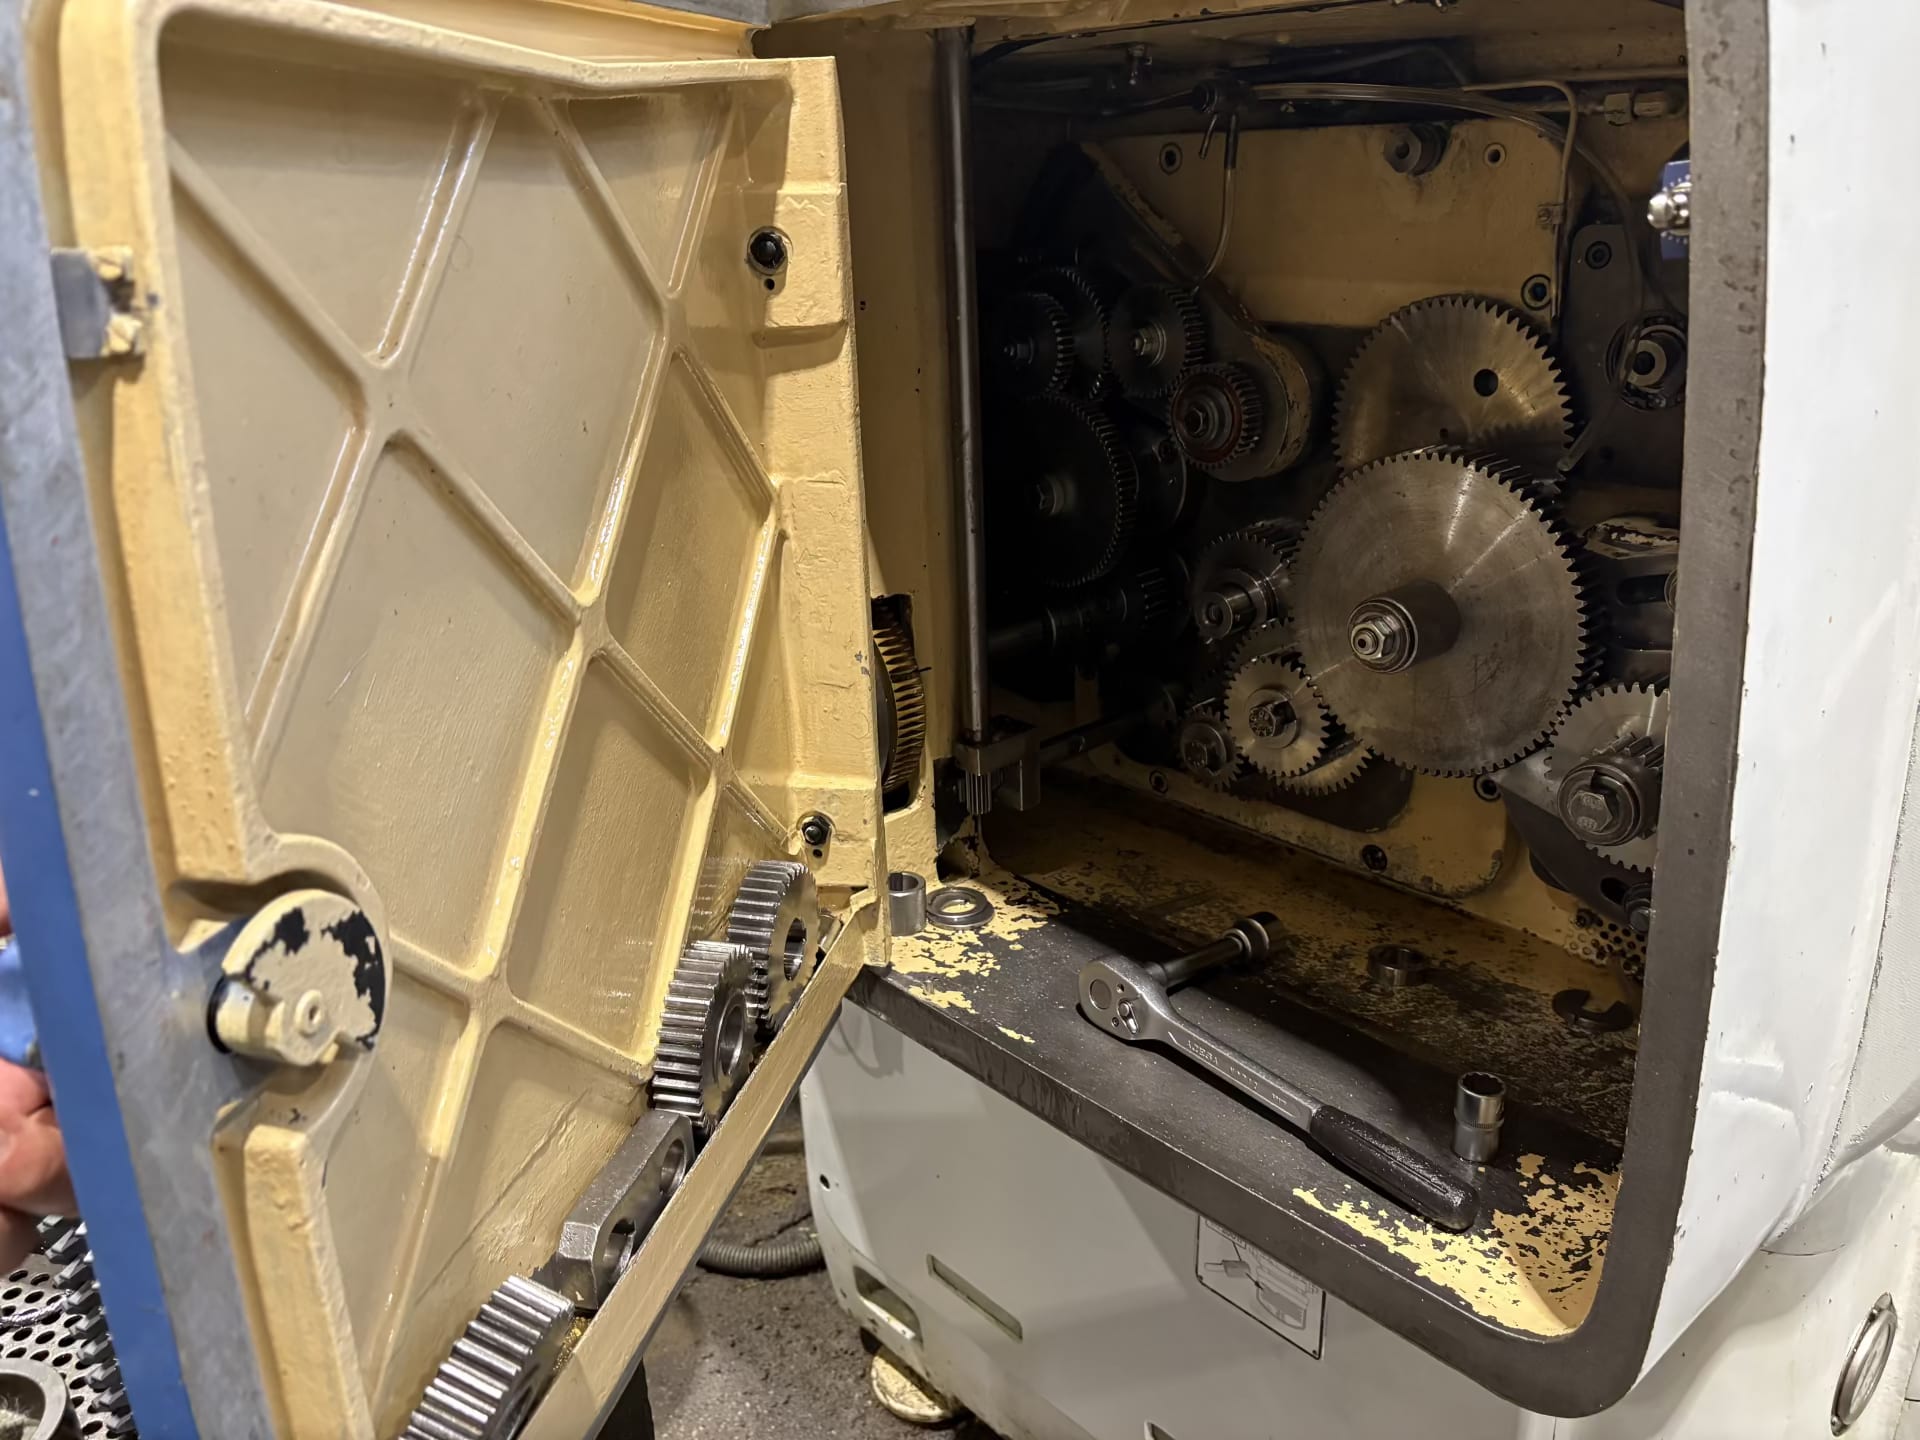
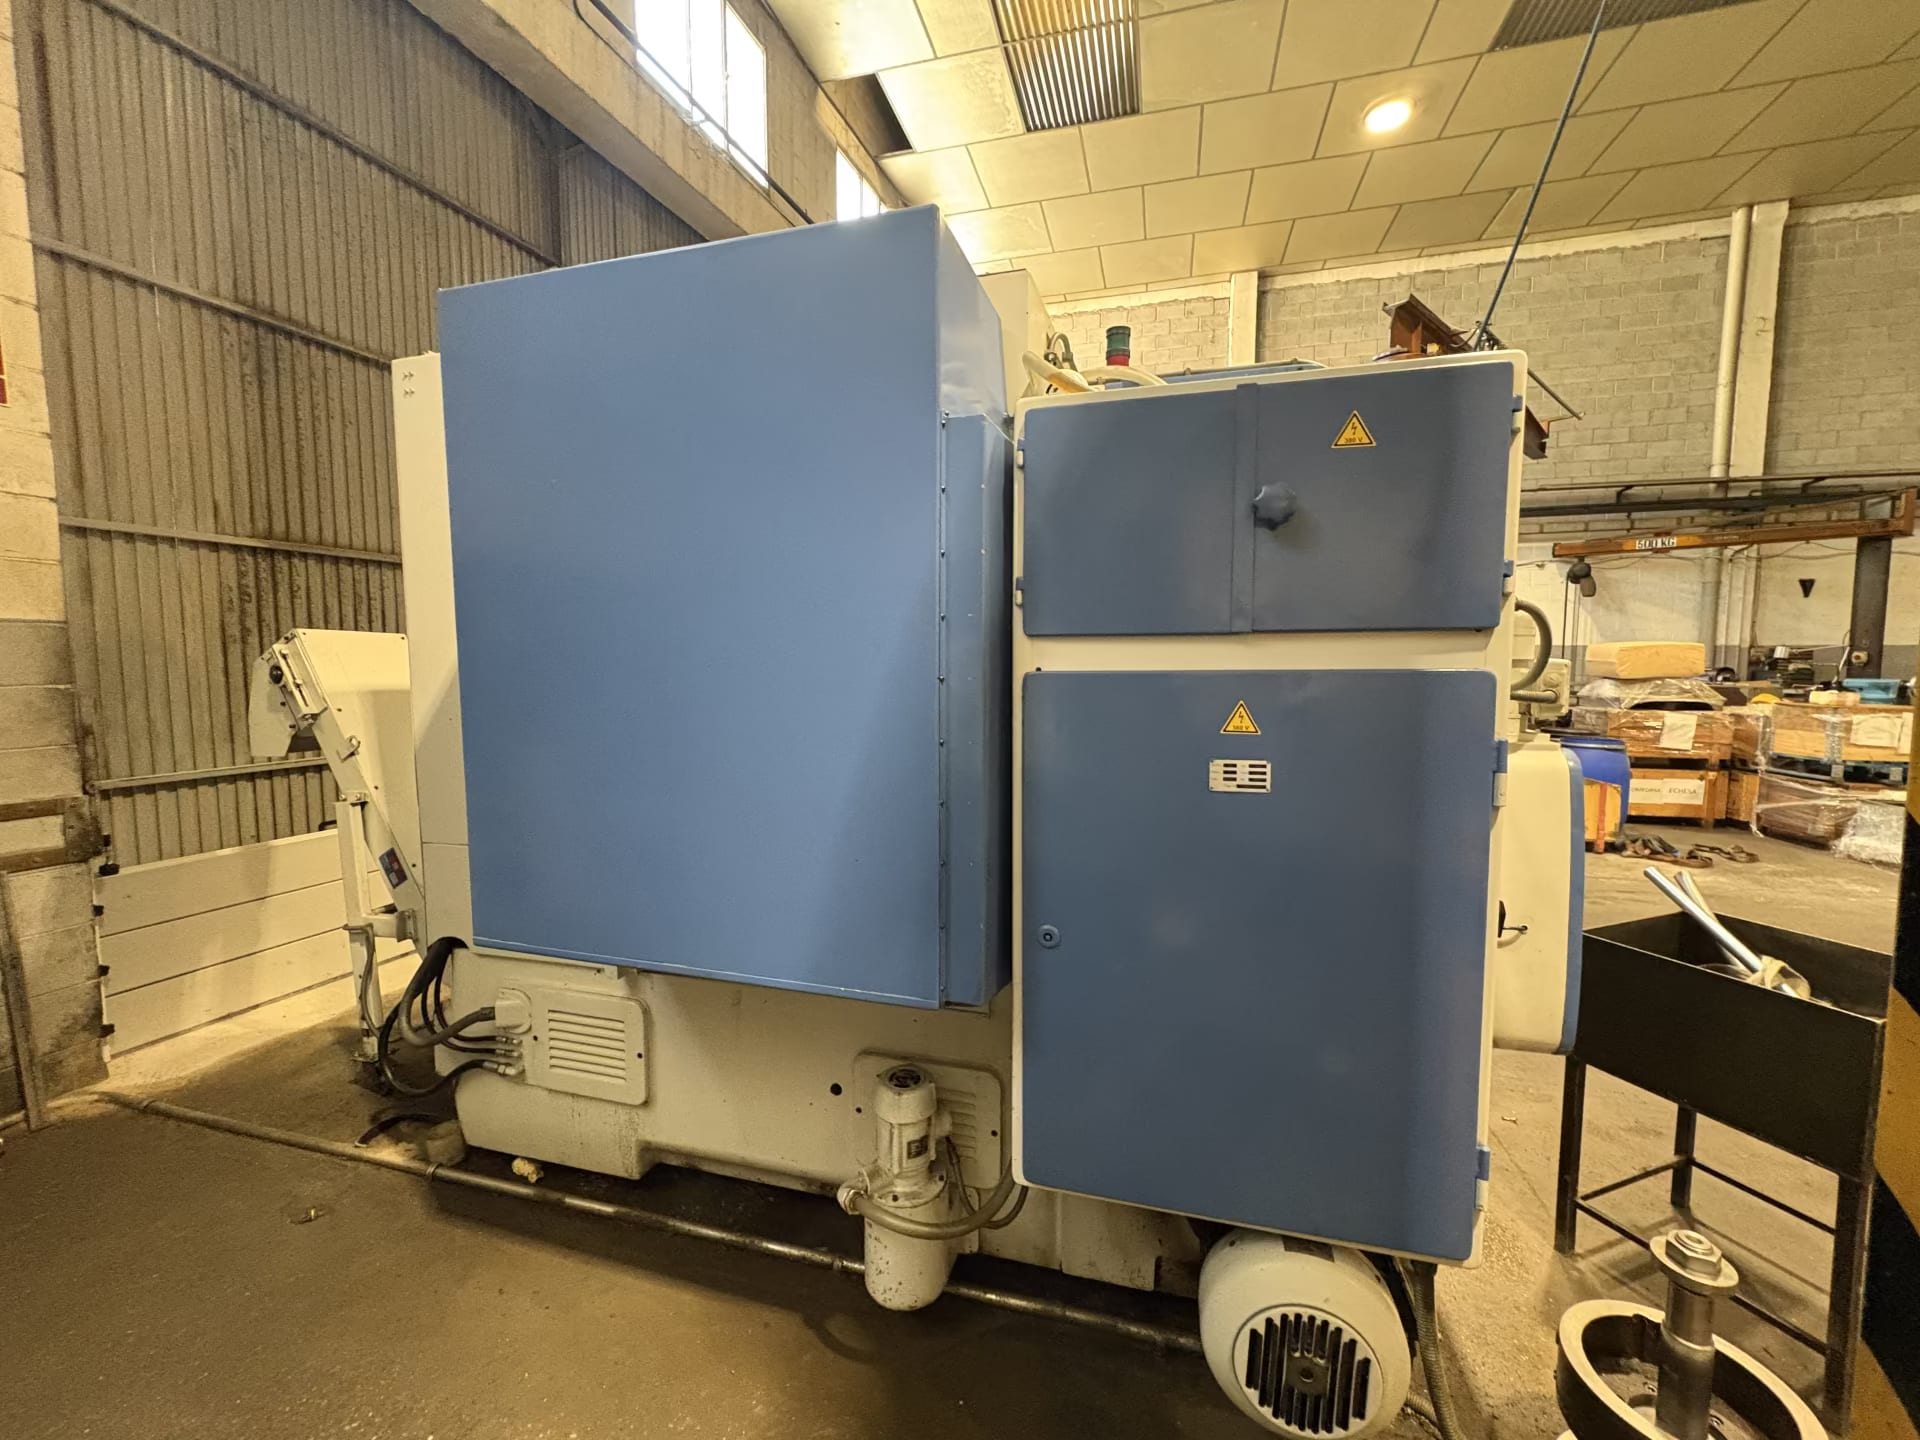
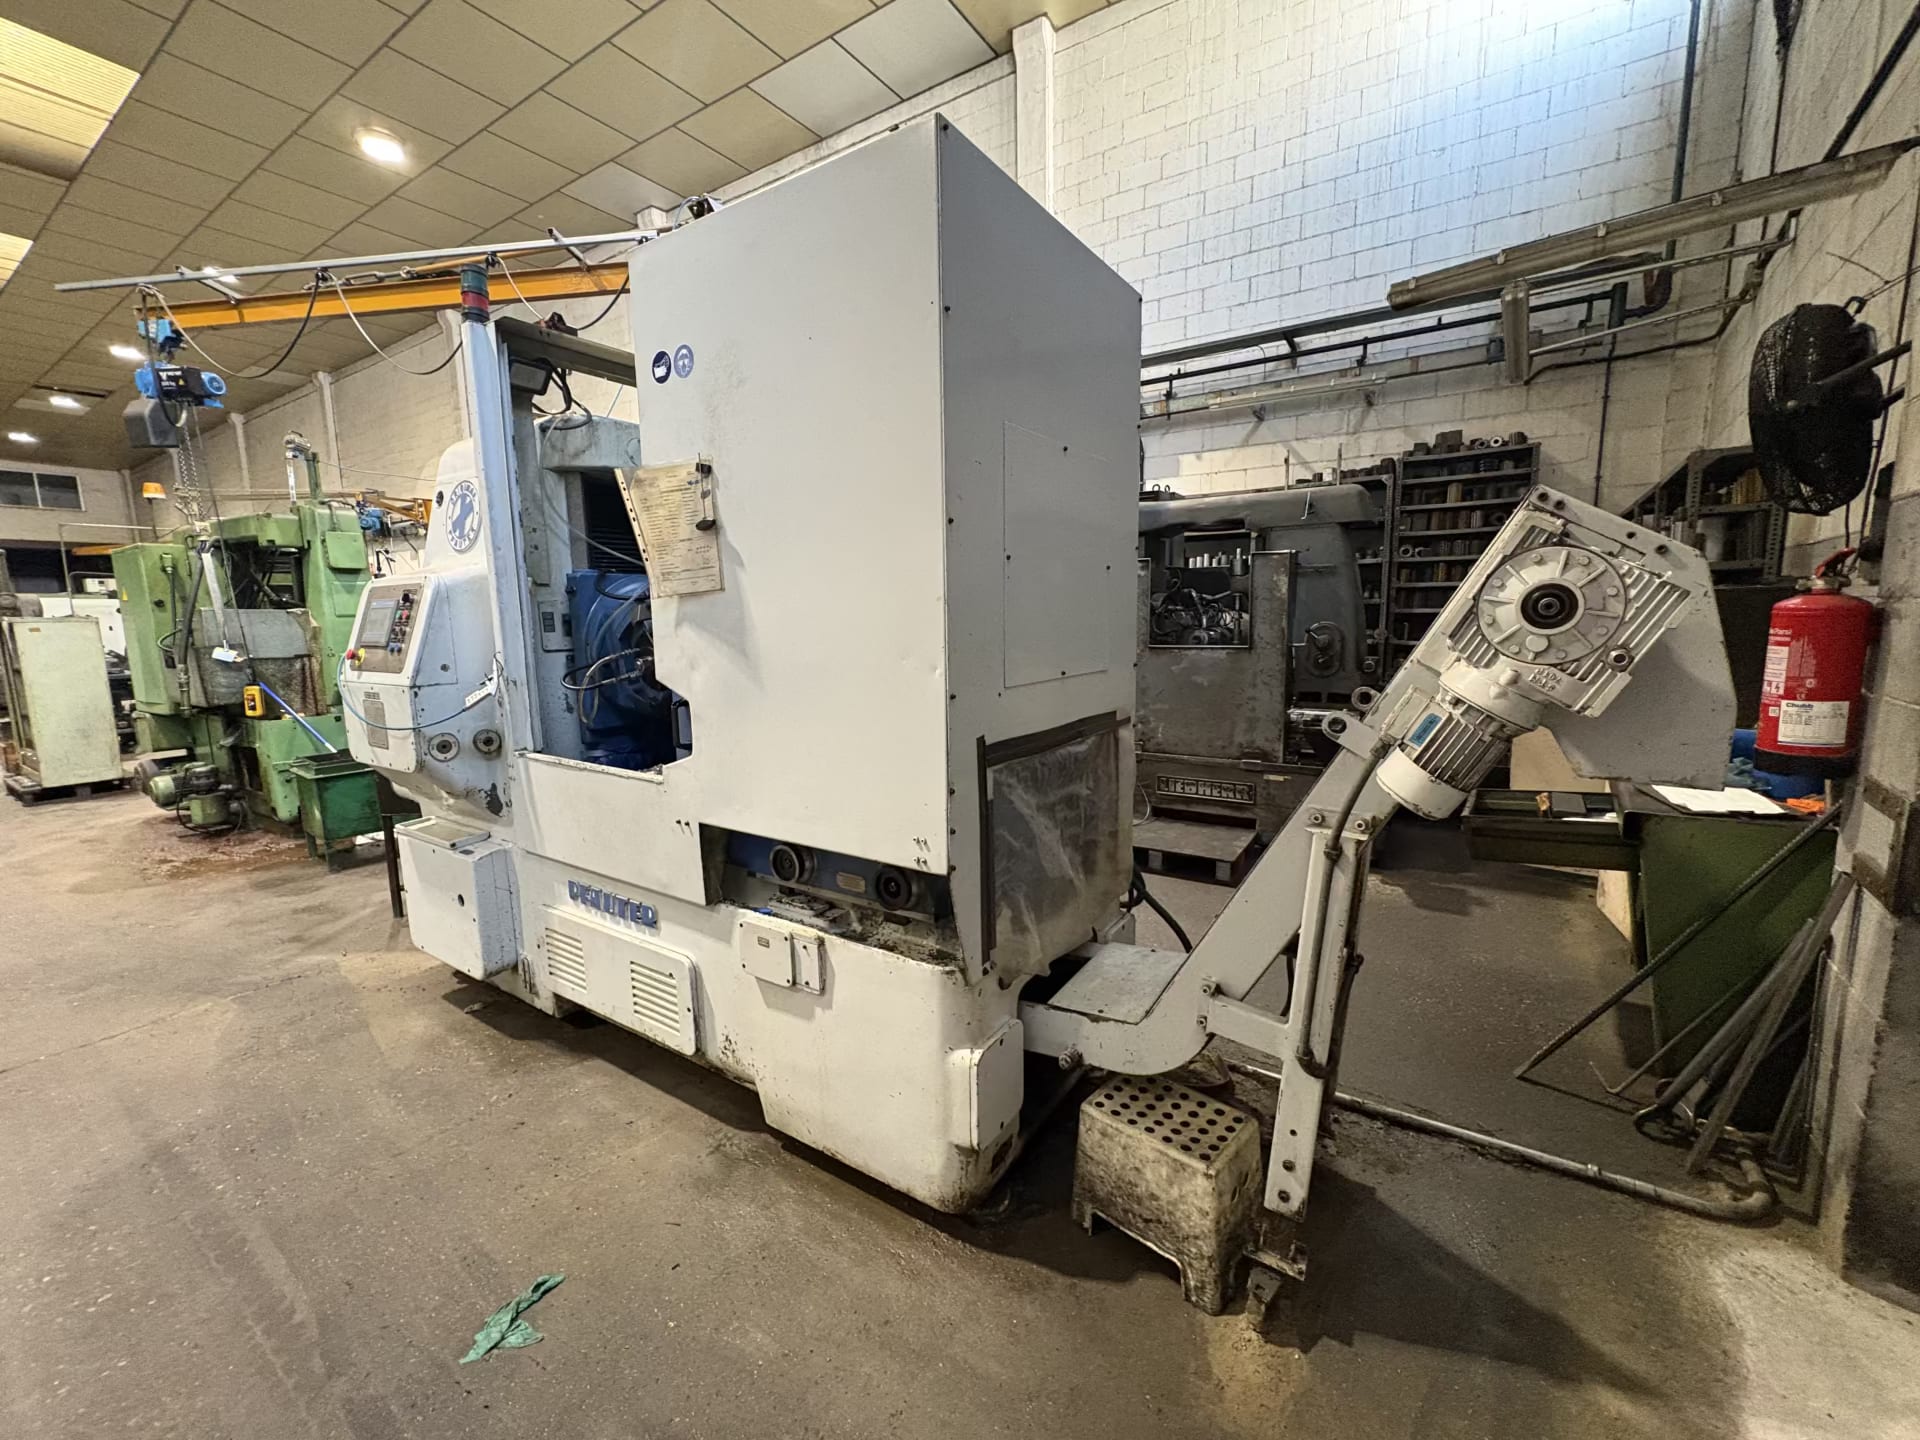
PFAUTER P630 Gear Hobbing Machine.
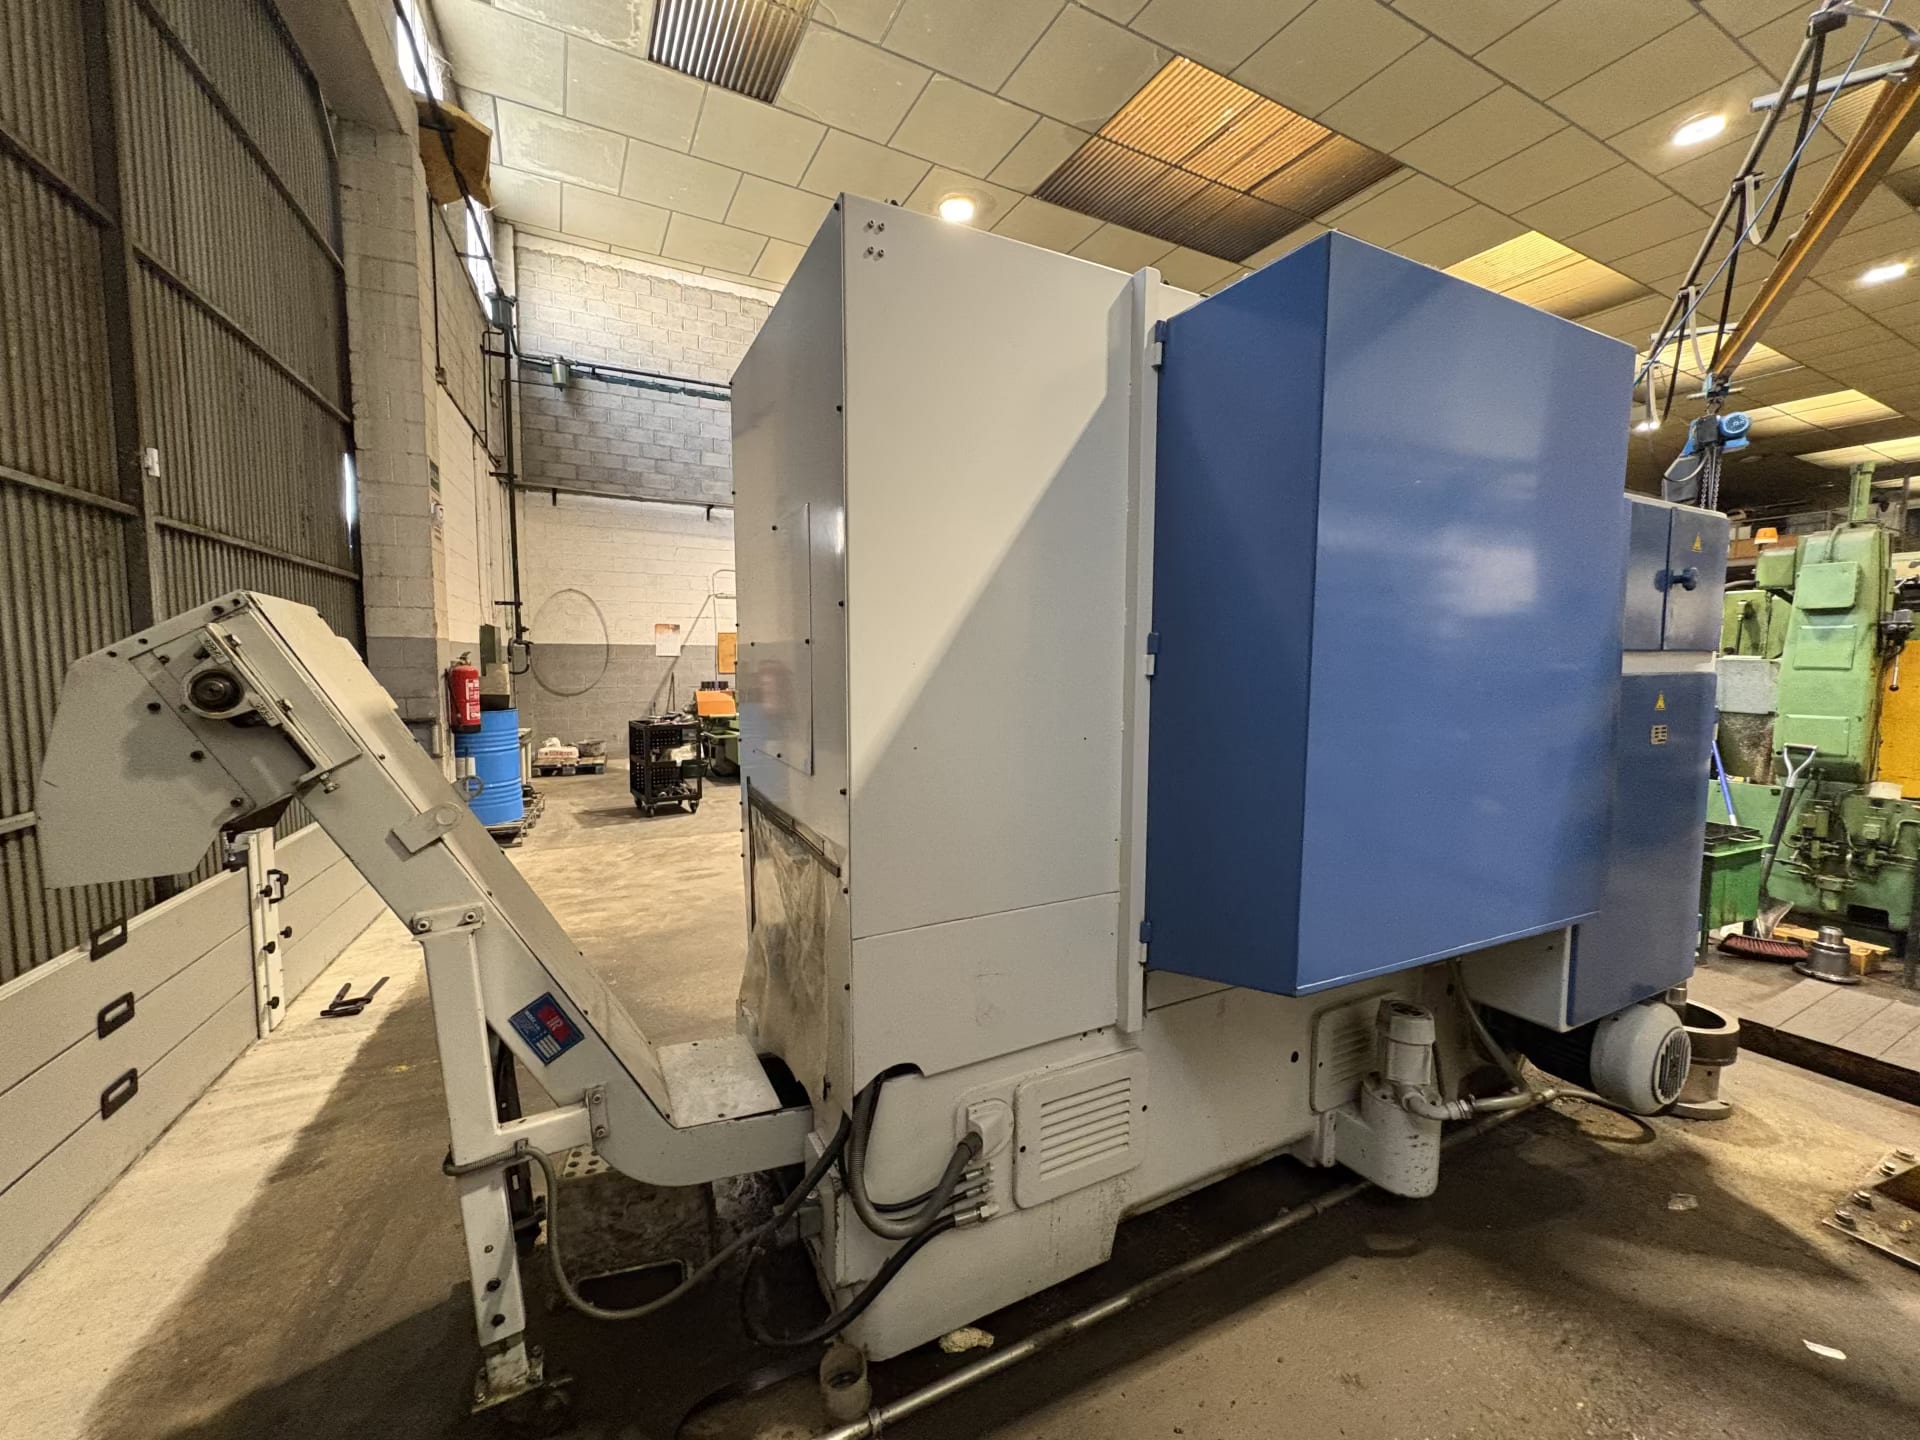
Chip Conveyor
Maximum Gear Diameter 630 mm
Gear Width 425 mm
Maximum Module 10
Table Diameter 550 mm
Table Bore 125 mm
Maximum Cutter Length 215 mm
Minimum Number of Teeth 8
Maximum Workpiece Length 825 mm
Distance Milling Spindle - Clamping Surface 50 - 425 degrees
Milling Slide Swivel 240 degrees
Spindle Speeds 62 - 390 RPM
Tangential Adjustment 200 mm
Axial Feeds 0.4 - 6.8 mm/rev
Radial Feeds 0.1 - 1.7 mm/rev
Maximum Cutter Diameter 192 mm
Total Power Requirement 20 kW
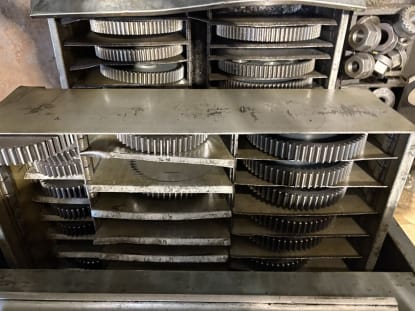
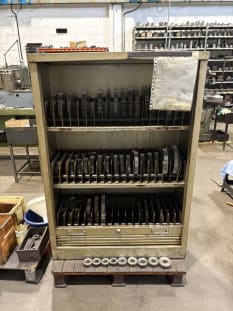
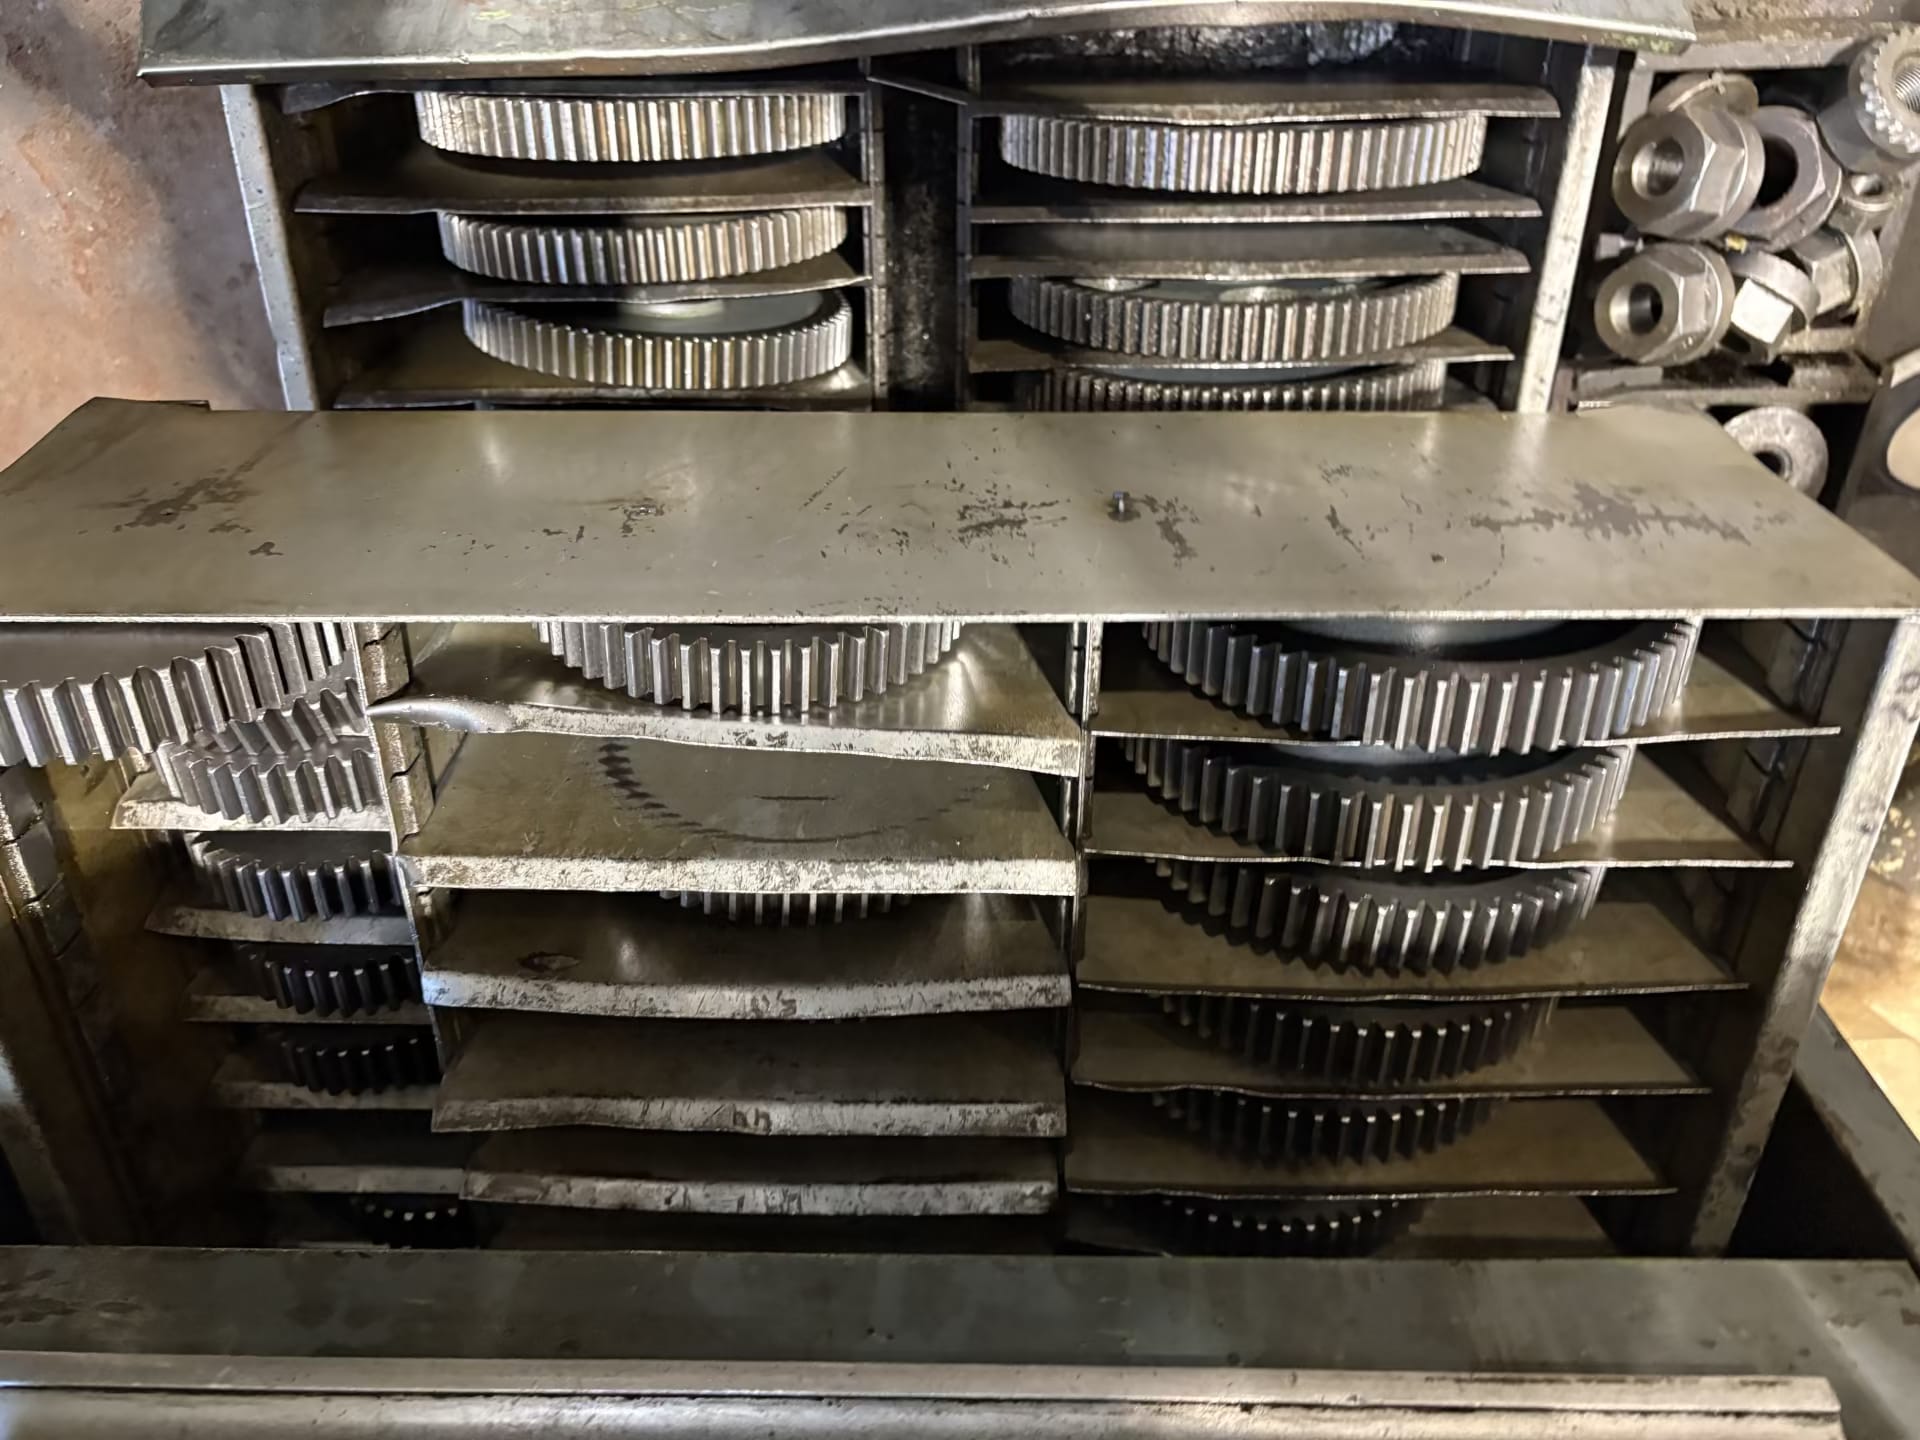
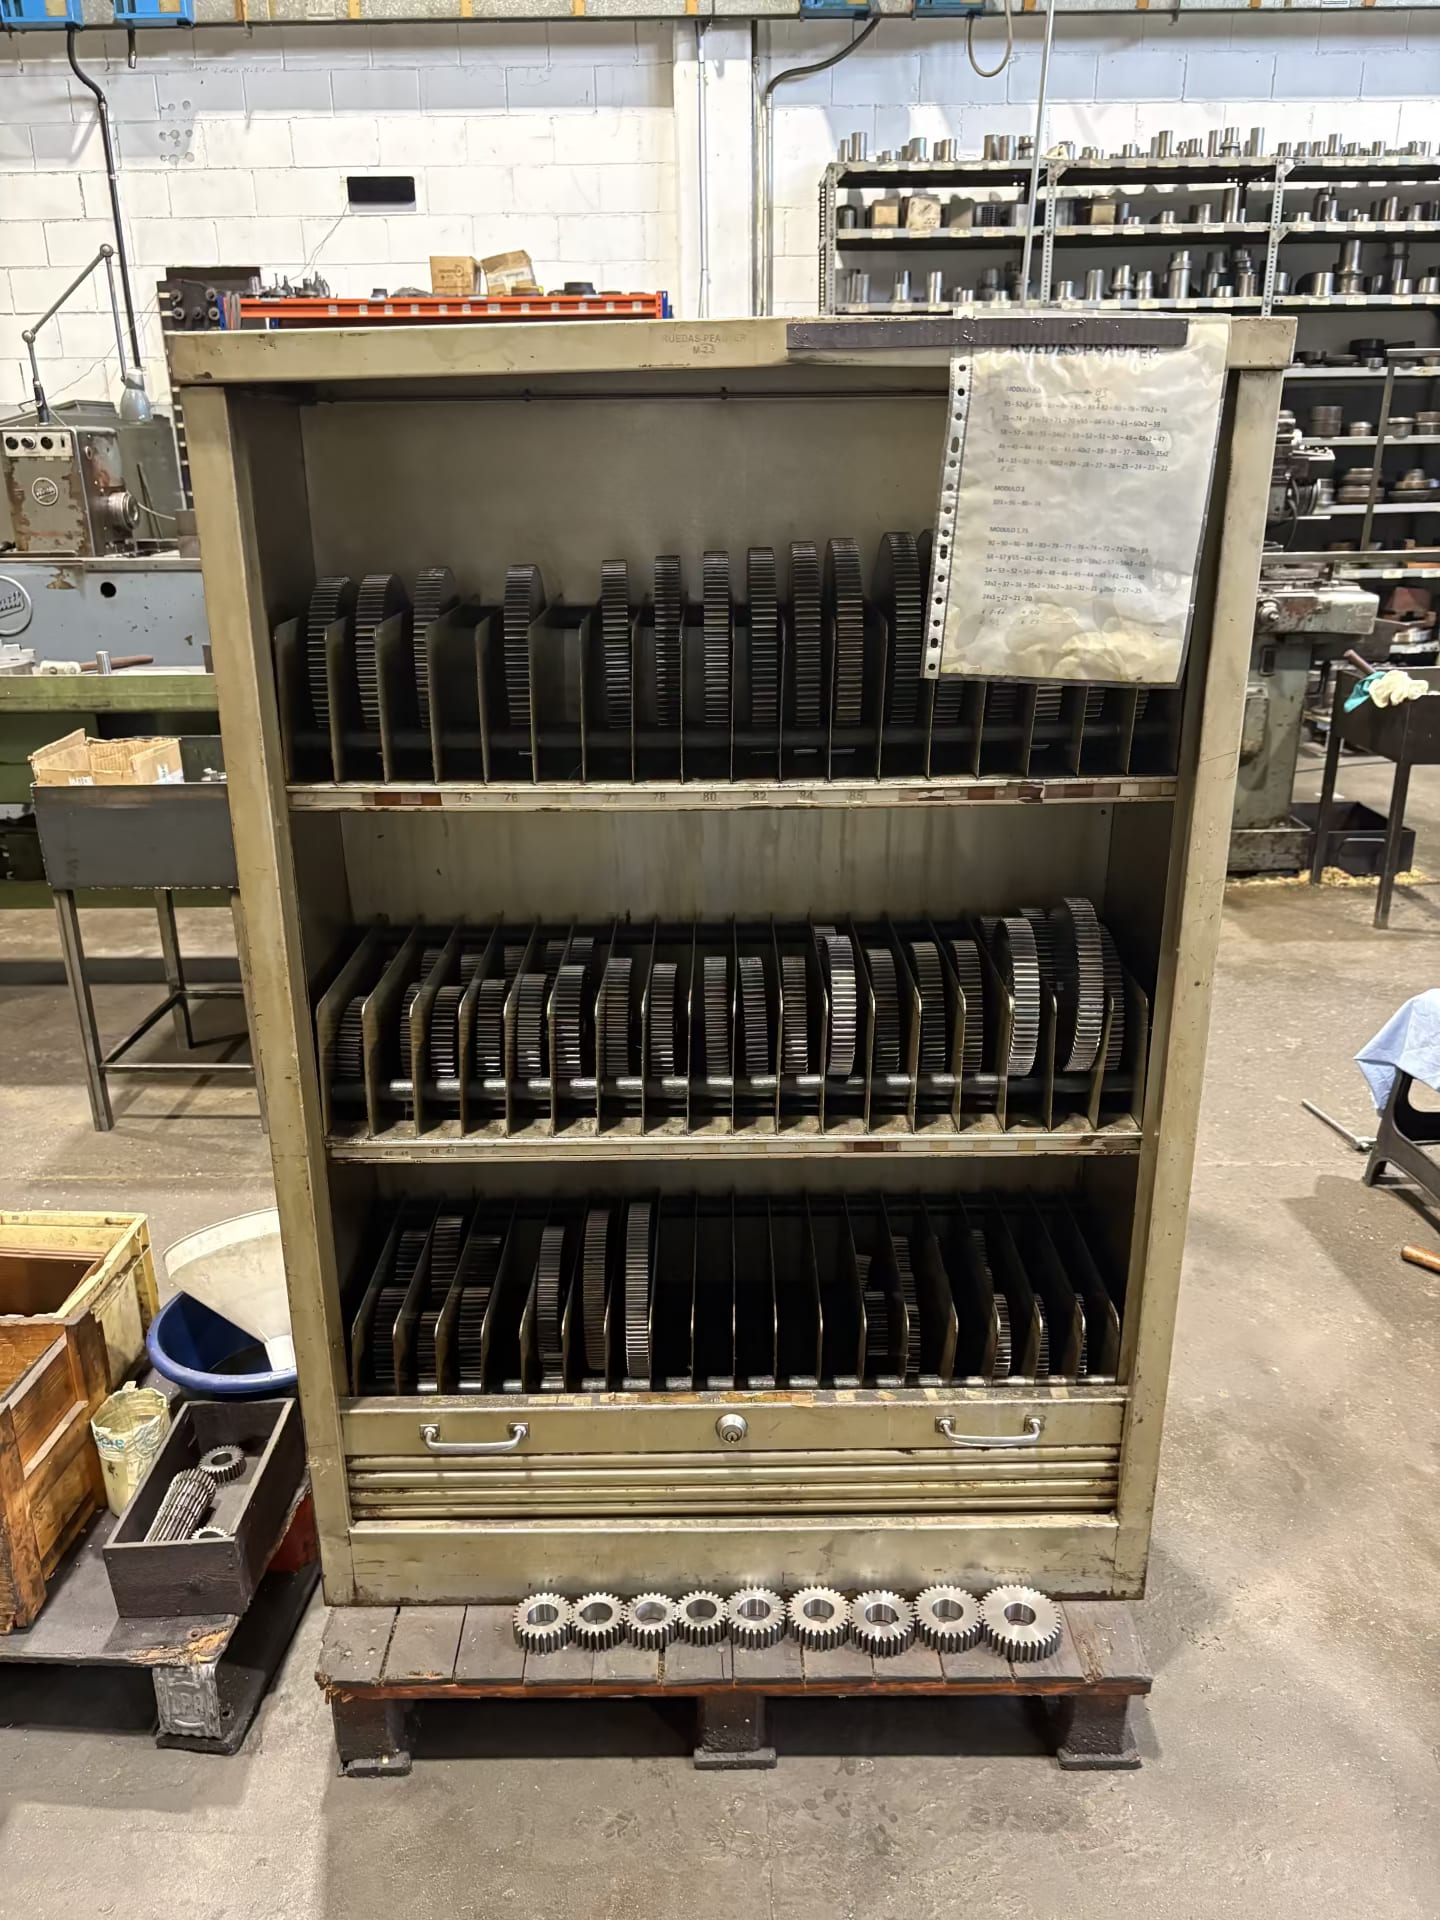
Change Gears Set / Chip Conveyor / Coolant Tank
- Transportation costs
- not included
- Terms of delivery
- EXW EX Works
- Terms of payment
- 100% prepayment before pick-up
Transportation costs are not included in the used grinding or gear cutting machine price; terms of delivery and payment are stated under "Additional information" in each listing. You should also budget for installation and commissioning at the new site. In most cases, the buyer is responsible for organizing the transport; upon request, ReMach can check whether transport can be arranged or supported. ReMach also helps with dismantling, loading and export paperwork.
Yes. Grinding produces very fine swarf, and coolant that is not filtered scratches the surface and shortens the life of the grinding wheel. Check whether the listing includes a filter system, such as a paper band filter or a magnetic separator. Grinding with oil, common in gear and tool grinding, also requires oil mist extraction and fire protection.
For gear cutting machines, check the maximum workpiece diameter, maximum module, face width and helix angle. For grinding machines, check the maximum grinding diameter and length, grinding wheel size and workpiece weight. For CNC machines, also check the control and whether in-machine measuring is included.
The three processes are used at different stages. Gear hobbing cuts the teeth with a hob, usually before heat treatment. Gear grinding finishes the teeth after heat treatment to reach high accuracy. Cold rolling forms teeth or splines by cold forming without chips and suits small modules and series production.
Grinding machines differ by the surface they produce. Surface grinders machine flat faces, usually on a magnetic table; cylindrical grinders machine rotational parts held between centres or in a chuck, externally or internally; centreless grinders support cylindrical parts on a work rest blade between grinding and regulating wheel, ideal for large series. Tool grinders sharpen and make milling cutters, drills and turning tools, while gear grinders finish tooth profiles.

Our Services
- Inspection & report
- Disassembly & installation
- Global logistics
- Customs & paperwork
- Sourcing & valuation
- Personal consultation
Related items
1. Hobbing Machines: Gear Manufacturing for All Types
Hobbing machines, also known as hobbers, are specialised machines designed for the precision production of gears. Using the machine's various settings, operators can configure the number of teeth, helix angle and profile correction to exact specifications. The hobber engages single or multiple-gear worms with the workpiece to form a worm gear unit, while the rotary cutting motion is driven by the turning milling tool. As the tool advances alongside the workpiece, it generates the tooth space – enabling the production of both spur and helical gears.
- Manufacture of gears across all types and forms
- Suitable for components used across a wide range of industries
- Exceptional dimensional accuracy and repeatability
The versatility of a hobbing machine makes it well suited to producing gears and splines to the highest levels of precision. As metal removal gradually wears the milling tool, it is continually shifted to bring fresh cutting edges into contact with the workpiece, ensuring consistent tooth quality throughout the run. Once the tool is fully worn, it is resharpened using a specialised grinding machine, extending its working life and maintaining process efficiency.
2. Hobbing Machines: From Concept to Modern Implementation
Hobbing machines were first conceived in 1856 by Christian Schiele, though automating the process remained beyond the technology of the era. In 1887, George Bernard Grant — an inventor best known for his work on mechanical calculators — filed the patent for the first true hobbing machine. The pivotal breakthrough came with a universal hobbing machine developed by Hermann Pfauter of Chemnitz, founder of the renowned PFAUTER brand.
Hobbing machine in use
3. Gear Hobbing: Industrial Applications & Key Products
Gear hobbing machines produce a wide range of gear types, including outer spur gears, helical gears, and inner gears across various sizes. The process also supports the manufacture of bevel gears, crown wheels, palloid and hypoid gearing, Gleason and Klingelnberg tooth systems, as well as screw augers and worm wheels.
These components are used across the automotive industry, agricultural technology, mechanical engineering, and plant construction. Tooth width and helix angle can be adjusted with precision through straightforward tool settings, while the continuous cutting action – with no back stroke – produces chips efficiently and consistently.
The hobbing process delivers high dimensional accuracy, making it well suited to demanding applications. Where tighter tolerances are required, workpieces are typically hardened and then finished by grinding or honing.
4. Hobbing Machine Suppliers: LORENZ, PFAUTER & More
Leading hobbing machine manufacturers include well-established names such as LORENZ, PFAUTER, and KLINGELNBERG, each recognised for their precision engineering and long-standing expertise in gear cutting technology.